Why Pulp and Paper Mill Wastewater Differs from Municipal Duty
Pulp and paper mill wastewater treatment typically combines equalization, primary DAF or clarification, anaerobic digestion, aerobic CAS or MBR, and Fenton or ozone polishing. Influent COD usually spans 1,000–25,000 mg/L with BOD₅ 400–8,000 mg/L at 35–60 °C. The train targets BOD, TSS, color, and AOX so mills meet EPA 40 CFR 430, EU BAT-AELs, or GB 3544 discharge limits.
Kraft and recycled-paper mill influent arrives with COD of 1,000–25,000 mg/L and BOD₅ of 400–8,000 mg/L. TSS runs 500–4,000 mg/L, color 5,000–20,000 Pt-Co units, and AOX 5–40 mg/L at pH 5–10 and 35–60 °C. Those ranges come from EPA 40 CFR 430 background documents and recent industry surveys (IFAS, 2025). Three numbers drive train design: BOD:COD typically 0.3–0.5, heat that favors anaerobic energy recovery, and AOX that biology alone cannot strip.
The temperature and COD profile make anaerobic pretreatment commercially attractive. A mesophilic UASB or IC reactor operating at 35–40 °C converts up to 85% of influent COD to biogas. Methane yield is approximately 0.35 Nm³ CH₄ per kg COD removed (per 2024 IWA anaerobic reactor design data). Few other industrial waste streams allow an ETP to export energy while still meeting COD discharge limits.
Four sub-streams sit inside a typical mill, and the train must match each. Kraft pulping produces black liquor that is normally recovered in the recovery boiler and only sent to the ETP as spills or condensates. Bleaching generates the chlorinated organics, color, and AOX load. The paper machine discharges white water rich in starch, fillers, and fiber fines.
The combined integrated-mill effluent is what most ETPs actually treat. Equalization and segregation, not biology, are usually the first things to fix on a mill ETP.
Pulp and Paper Mill Wastewater Treatment: The 2026 Process Train
The 2026 reference train for combined pulp and paper effluent starts with bar screening and grit removal. Flow and quality equalization follows at 6–12 h HRT with 4–8 W/m³ mixing. Primary clarification or dissolved air flotation (DAF) then feeds an anaerobic UASB or IC reactor at 6–24 h HRT. The aerobic stage is conventional activated sludge (CAS) or a membrane bioreactor (MBR system for pulp and paper biological treatment).
Tertiary polishing uses Fenton, ozone, sand filter, activated carbon, and optionally RO. Sludge thickening and dewatering close the train with a plate and frame filter press for paper mill sludge. The block flow is similar from the EU to North America to China. Segregation upstream and reuse downstream create the real differences.
For fiber-rich streams, a DAF system for pulp and paper primary treatment outperforms sedimentation. Micro-bubble flotation at 5–20 m/h hydraulic loading typically removes 80–95% of TSS and 60–80% of suspended BOD. It also strips most free oil and resin that would overwhelm the anaerobic stage.
Sedimentation tanks cap out near 3 m/h overflow rate and lose fine fiber. DAF captures those fines and is the default primary step in most 2026 retrofits.
Positioning MBR after the anaerobic stage collapses the secondary clarifier and sand filter into one step. Effluent TSS is routinely below 1 mg/L with particle cut-off <1 μm. Aerobic CAS still removes most soluble COD. MBR is preferred when the mill wants reuse water or a tight TSS consent.
Fenton polishing doses H₂O₂ at 0.5–2× the COD mass and Fe²⁺ at 50–200 mg/L. Operators hold pH 3–4 for 30–60 minutes, then neutralize. That chemistry cuts color and AOX biology cannot remove. Sludge yield is 8–15 kg dry solids per 1,000 L treated, dewatered to 25–35% DS for disposal or co-incineration.
Unit Operation Parameters and Equipment Choices
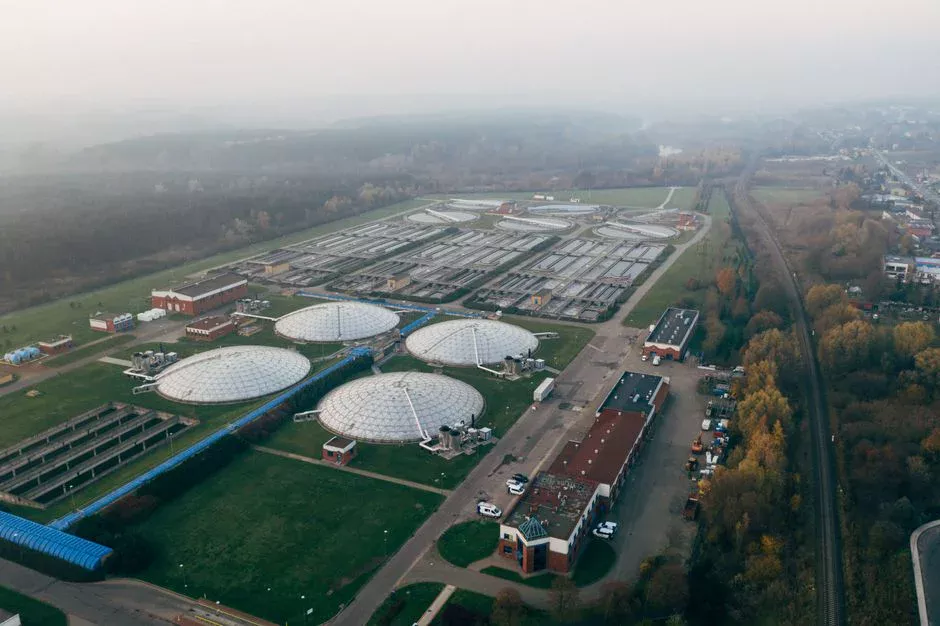
Unit operation parameters for pulp and paper ETPs in 2026 sit in the design basis table below. Engineers can lift the ranges into a design basis document. Procurement can use the same numbers to specify equipment. Values are typical operating ranges from 2024–2026 mill installations (HydropureWater field data, 2026; cross-checked against EPA 40 CFR 430 background documents and EU BREF 2014).
| Unit Operation | Key Parameters | Typical Equipment |
|---|---|---|
| Equalization | HRT 6–12 h; mixing 4–8 W/m³; air or mechanical | Equalization basin with submersible mixers |
| Primary (DAF) | Surface loading 5–20 m/h; recycle ratio 10–30%; air:solids 0.005–0.06 kg/kg | DAF system for pulp and paper primary treatment |
| Anaerobic UASB/IC | HRT 6–24 h; upflow 1–3 m/h; OLR 5–15 kg COD/m³/d; COD removal 60–85% | UASB or IC reactor with GSS separator |
| Aerobic CAS | MLSS 3,000–5,000 mg/L; SRT 15–30 d; F/M 0.1–0.3 kg BOD/kg MLSS/d | Aeration basin + secondary clarifier |
| Aerobic MBR | MLSS 8,000–12,000 mg/L; SRT 30–60 d; flux 10–20 LMH; effluent TSS <1 mg/L | MBR system for pulp and paper biological treatment with DF-series PVDF flat-sheet MBR module |
| Fenton Polishing | pH 3–4; H₂O₂:Fe²⁺ molar 5–10:1; reaction 30–60 min; COD drop 40–70% | Reaction tank + neutralization + DAF or sand filter |
| Sludge Dewatering | Cycle 60–180 min; cake 25–35% DS; polymer dose 3–8 kg/t DS | Plate and frame filter press for paper mill sludge |
CAS versus MBR is the recurring design decision on pulp and paper biological trains. CAS needs 3–4× the footprint of an equivalent MBR. It also settles worse (SVI 150–250 vs 80–120) and discharges 10–30 mg/L TSS — fine for sewer, not for reuse.
MBR runs at 2–3× the MLSS, doubles the SRT, and emits <1 mg/L TSS with low turbidity for RO pretreatment. The trade-off is energy: MBR aeration and membrane scouring add 0.1–0.2 kWh/m³. Upstream anaerobic biogas typically offsets 30–60% of that load on kraft mills we size.
For the primary step, the comparison is simpler on fiber-rich mill effluent. Sedimentation caps at roughly 3 m/h overflow rate and loses 40–60% of TSS from fiber-rich streams. DAF handles 5–20 m/h, removes 80–95% of TSS, and recovers fiber as a saleable stream.
A high-efficiency sedimentation tank still has a place as a pre-DAF grit step. DAF is now the default primary clarifier on pulp and paper retrofits built or upgraded in 2024–2026.
Recycled Paper vs Kraft Mill: How the Train Changes
Recycled (de-inking) mill effluent carries lower AOX (typically <5 mg/L). It also carries higher starch, coating color, ink residues, and DAF skimmings. The full train is still justified, but the anaerobic step becomes optional.
DAF plus MBR plus Fenton is the standard 2026 configuration for recycled mills, and capital can be saved by skipping the UASB/IC. AOX is rarely the limiting parameter; color and COD usually are.
Kraft mills are the opposite case on load and AOX. Cooking and bleaching generate high BOD, dark color (often 10,000+ Pt-Co), and AOX of 10–40 mg/L. The full train is mandatory: DAF for fiber, UASB or IC for BOD and biogas, MBR for residual COD, and Fenton or ozone for color and AOX.
Bleaching-stage equalization is non-negotiable on kraft ETPs. Without it, bleach-plant spikes wipe out methanogens in the anaerobic reactor.
Integrated mills (pulp plus paper) sit in the middle of the load range. They need combined equalization sized for the worst-case sub-stream, not the average day. Black-liquor segregation is the other non-negotiable.
The recovery boiler should handle >99% of black liquor solids, with only spills and condensates routed to the ETP. Designing biology to absorb raw black liquor is a fast path to upset and a consent failure.
How do kraft effluent system balances work?
Kraft effluent system balances start with mass flows for black liquor solids, bleach filtrates, and paper-machine white water. Size biology only after those flows are fixed. Most plants we size keep >99% of black liquor solids in the recovery boiler loop. Only spills and condensates go to the ETP.
Bleach filtrate equalization at 6–12 h HRT damps AOX and pH spikes that crash methanogens. White-water fiber and filler loads set primary DAF surface loading. Anaerobic OLR then follows residual soluble COD after fiber capture.
A practical kraft balance sheet tracks COD, TSS, AOX, and temperature for each sub-stream against the combined ETP feed. If bleach COD peaks exceed the anaerobic OLR envelope of 5–15 kg COD/m³/d, add diversion or extra equalization before the UASB or IC.
Temperature balances matter on kraft effluent as well. Influent at 35–60 °C supports mesophilic reactors without steam. Cooling may still be needed when white water dilutes hot kraft streams below about 30 °C.
How does tissue mill wastewater treatment differ?
Tissue mill wastewater treatment in 2026 usually follows a recycled-fiber path rather than a full kraft bleach train. Tissue lines shed high starch, wet-strength residuals, and fine fiber. AOX is typically <5 mg/L when virgin kraft bleach filtrate is absent.
Most tissue ETPs we commission skip anaerobic stages when BOD:COD stays high and COD is moderate. DAF plus aerobic MBR or CAS, then Fenton only if color consent is tight, is the common layout.
Smaller tissue sites and satellite converting plants often segregate sanitary wastewater from the process ETP. An Underground Package Sewage Treatment Plant (WSZ Series) can treat that domestic stream on-site. The process train then stays sized for fiber, starch, and coating loads. Where tissue white water is reused heavily, primary DAF fiber recovery and MBR filtrate quality become the binding constraints, not AOX polishing.
2026 Compliance Targets and Reuse Opportunities
2026 compliance targets for kraft and paper mills rest on three regulatory anchors. In the US, EPA 40 CFR 430 sets BOD₅ and TSS limits in kg per metric ton of product. Subparts cover kraft (B), paperboard (E), groundwood, sulfite, deink, and non-integrated paper — confirm the subcategory before sizing.
In the EU, IED 2010/75/EU and the 2014 BREF define BAT-AELs of COD 70–200 mg/L. AOX BAT-AELs run 0.1–1.0 mg/L and TOC 15–50 mg/L by process type.
In China, GB 3544-2008 plus the 2024 amendment path set pH 6–9. COD limits are ≤100 mg/L for existing plants and ≤80 mg/L for newer plants, with color ≤50 dilution units and AOX ≤12 mg/L. The train in this guide can meet all three when MBR and Fenton match the strictest local envelope.
Reuse is where the 2026 economics land for pulp and paper mills. An MBR plus RO system for paper mill water reuse can deliver 70–85% recovery. Permeate typically blends into wash water or cooling-tower make-up.
Integrated mills in water-stressed regions already run 50–70% reuse ratios. With biogas export from the anaerobic stage, full-train retrofit payback commonly lands inside 4–6 years at 2026 energy and discharge-fee tariffs.
CAPEX and OPEX Ranges for a 2026 Pulp and Paper ETP
CAPEX and OPEX ranges for a 2026 pulp and paper ETP are screening budgets only. Influent load, discharge envelope, seismic zone, and automation scope routinely shift these bands ±30%.
| Plant Size (Flow) | CAPEX (USD) | OPEX — Biological Only (USD/m³) | OPEX — Biological + Fenton (USD/m³) | OPEX — Full Train with RO/Reuse (USD/m³) |
|---|---|---|---|---|
| Small 100–500 m³/d | $400K–$1.5M | $0.15–$0.30 | $0.30–$0.55 | $0.45–$0.80 |
| Mid 500–2,000 m³/d | $1.5M–$5M | $0.15–$0.35 | $0.30–$0.65 | $0.50–$1.00 |
| Large 2,000–10,000 m³/d | $5M–$20M | $0.20–$0.45 | $0.35–$0.80 | $0.60–$1.20 |
Energy on a pulp and paper ETP is dominated by aeration: 0.4–0.8 kWh/m³ for the aerobic stage, plus 0.1–0.2 kWh/m³ for MBR scouring. Anaerobic biogas offsets 30–60% of aeration when methane feeds a CHP unit. Chemical cost is the swing OPEX variable.
Budget nutrients for biology, H₂O₂ and Fe²⁺ for Fenton, antiscalant for RO, and polymer at 3–8 kg per tonne of dry solids. An automatic chemical dosing for Fenton and nutrient addition cuts chemical spend 8–15% by tracking actual load. That is usually the cheapest OPEX win on an existing plant.
Selection Checklist Before You Freeze the Design Basis
A pulp and paper ETP selection checklist should be locked before CAPEX quotes harden. Skip any one item and the train usually needs a redesign mid-project.
- Confirm EPA 40 CFR 430 subcategory (or EU BAT-AEL / GB 3544 class) and the strictest COD, TSS, color, and AOX limits.
- Map kraft, bleach, paper-machine, and sanitary sub-streams; size equalization for the worst spike, not the average day.
- Choose primary DAF versus sedimentation from measured fiber fines and target TSS after primary.
- Decide anaerobic yes/no from BOD:COD, temperature (35–40 °C preferred), and biogas offtake value.
- Pick CAS versus MBR from reuse goals, footprint, and effluent TSS consent (<1 mg/L favors MBR).
- Budget Fenton or ozone only if color/AOX biology cannot meet; set H₂O₂ and Fe²⁺ from COD mass and pH 3–4 residence time.
- Close sludge path: 8–15 kg DS per 1,000 L treated, cake 25–35% DS, polymer 3–8 kg/t DS.
Plant engineers sizing kraft or tissue ETPs get the most from this guide. So do EPC contractors writing design bases and buyers comparing DAF, MBR, and Fenton packages. Mills that only need sanitary treatment for offices or remote converting sheds should use an Underground Package Sewage Treatment Plant (WSZ Series), not a full process ETP. To match equipment to your flow, COD envelope, and discharge consent, request a pulp and paper ETP design review with influent data and permit limits.
Frequently Asked Questions
What influent COD range is typical for a kraft pulp mill ETP?
Kraft mill combined effluent typically arrives at the ETP with COD of 1,000–25,000 mg/L, BOD₅ of 400–8,000 mg/L, and temperature of 35–60 °C (per EPA 40 CFR 430 background data, 2024–2025). This high-temperature, high-BOD profile is why anaerobic pretreatment with UASB or IC is standard on modern kraft mills. Designers should still confirm subcategory-specific production-normalized limits before freezing reactor volume.
How effective is MBR for pulp and paper mill wastewater?
An MBR at MLSS 8,000–12,000 mg/L, SRT 30–60 d, and flux 10–20 LMH typically delivers >95% COD removal and effluent TSS <1 mg/L (HydropureWater field data, 2026). The low-turbidity filtrate feeds RO for water reuse. Compared with CAS, MBR needs roughly one-third of the footprint and produces reusable water rather than sewer-grade discharge. Most mills targeting reuse specify MBR after anaerobic pretreatment.
Why is DAF preferred over sedimentation for paper mill effluent?
DAF operates at 5–20 m/h hydraulic loading versus the ~3 m/h limit of sedimentation, and removes 80–95% of TSS from fiber-rich streams that defeat clarifiers. Fiber recovery as a salable or recyclable stream is a second benefit that sedimentation rarely matches at the same footprint. Primary DAF is therefore the default on most 2024–2026 pulp and paper retrofits we see.
What is the standard Fenton dose for color and AOX removal?
Fenton oxidation for pulp and paper polishing runs at pH 3–4, with H₂O₂ dosed at 0.5–2× the COD mass and Fe²⁺ at 50–200 mg/L (H₂O₂:Fe²⁺ molar 5–10:1), a 30–60 minute reaction, and post-neutralization. Chemistry details are covered in the Fenton Oxidation System guide for industrial use, 2026. Biology cannot replicate this step for AOX and high-molecular-weight color bodies.
What causes effluent TSS exceedance and how is it fixed?
TSS exceedance on a paper mill ETP usually traces to three causes. Bulking sludge in the secondary clarifier (SVI >200) is common. Flow spikes past equalization can wash out solids. A damaged MBR membrane can also leak biomass.
Diagnostic steps are mapped in the 2026 engineering guide to effluent TSS exceedance. Practical fixes are usually a polymer dose change, an SRT increase, or a membrane integrity test on the affected line.