
Why Textile Effluent Is a 2026 Priority for UK Mills
UK mills cannot defer effluent upgrades in 2026 because three pressures have converged on dyehouse discharge: tightening Environment Agency consent limits, brand-led chemistry restrictions, and rising water-and-sewerage bills. Textile wet processing is one of the most water-intensive industrial activities on record, consuming up to 300 L of process water per kg of finished fabric (Soares et al., 2014, via ScienceDirect topic page). With 10–15% of applied dye pigments lost to the effluent stream (Yuranova et al., 2004, via ScienceDirect topic page) and more than 100,000 commercial dyes in circulation, a generic biological plant is not engineered to handle the chromophore load, salinity, or auxiliaries in a modern reactive dyehouse.
The regulatory layer now stacks three regimes on top of each other. First, EPR 2010 permits issued by the Environment Agency govern any direct discharge to surface water or ground, with consent limits increasingly specified on colour, salinity, and persistent substances. Second, trade-effluent consents issued by the local sewerage undertaker (Thames, United Utilities, Yorkshire Water, Severn Trent) govern the 90%+ of UK wet processors that discharge to sewer. Third, the ZDHC Wastewater Guidelines 2.1 and ZDHC MRSL 3.1 set commercial discharge targets stricter than minimum consent and are now embedded in the supplier requirements of most UK high-street brands (ZDHC Foundation, 2024 guidance). A 2019 Chemicals Investigation Programme run by the Environment Agency also keeps PFAS-based finishes and PFCs under active scrutiny. The mill that does not revisit its consent, chemistry, and reuse position in 2026 will pay the difference in sewerage charges, brand audit findings, and missed water-reuse savings.
What Is in Textile Wastewater: A Contaminant Profile
Textile wastewater is not one stream — it is a sequence of process-specific discharges that mix in the drains: scouring (high pH, BOD, greases), bleaching (residual H₂O₂, starch sizes), dyeing (unfixed reactive, azo, disperse, sulfur, vat, or acid dyes, plus 50–100 g/L of Glauber salt from reactive baths), and printing/finishing (metals from pigments, softeners, formaldehyde, PFCs). ScienceDirect's textile wastewater topic page catalogues the chemical families a treatment plant must address: dyes, starches, hydrogen peroxide, surfactants, acids, alkalis, metal soaps, and dispersants.
Quantify that profile and the engineering problem becomes clearer. Reactive dyeing alone adds 50–100 g/L TDS through sodium chloride and sodium sulphate, often meaning the inorganic salt load exceeds the organic COD load. The dye families behave very differently in biological systems: reactive azo and disperse dyes are notoriously recalcitrant because their chromophores are designed to resist washing, light, and microbial attack; sulfur and vat dyes carry high COD and strong colour; acid and direct dyes are more amenable to biosorption. Variability is the second engineering constraint: a dyehouse running three shifts can swing pH from 4 to 12 across a single day as batches drop. DAF and equalisation tanks exist precisely to flatten that swing before it reaches the biological stage.
UK Discharge Routes and 2026 Consent Limits
Identifying the legal regime is the first step before any equipment is specified. UK textile sites fall into one of two consent routes, and the choice dictates both the target quality and the enforcement body.
- Discharge to sewer — a trade-effluent consent issued by the local water and sewerage company under the Water Industry Act 1991. Limits are site-specific but typically cover BOD (often ≤300 mg/L), COD (often ≤1,000 mg/L), TSS, ammonia, oil and grease, pH (commonly 6–10), temperature (≤43 °C at the sewer point), sulphide, and metals (Cr, Cu, Ni, Zn). Many undertakers now add colour as a Hazen or m⁻¹ absorbance limit and a conductivity or chloride cap, particularly for dyehouses.
- Direct discharge to surface water or ground — an Environmental Permitting (England and Wales) Regulations 2010 (EPR 2010) permit from the Environment Agency. EPR permits are bespoke, increasingly tight on colour (true and apparent), salinity, and persistent substances, and any new application requires a H1 risk assessment and detailed chemical monitoring.
On top of the legal regime, two non-statutory drivers shape 2026 investment: the 2019 Chemicals Investigation Programme (Environment Agency, 2019) which extended PFAS scrutiny to textile finishes, and the ZDHC Wastewater Guidelines 2.1 which brand buyers now audit against. A mill discharging to Thames or United Utilities typically needs to meet both sets of targets in practice.
| Regime | Issued by | Typical parameters limited | 2026 tightening trend |
|---|---|---|---|
| Trade-effluent consent (sewer) | Local water company (Thames, United Utilities, Yorkshire, Severn Trent, etc.) | BOD, COD, TSS, ammonia, oil/grease, pH, temperature, metals, sulphide | Adding colour (Hazen/absorbance), chloride/conductivity caps, Zn and Cr tightening |
| EPR 2010 permit (direct discharge) | Environment Agency | COD, BOD, TSS, ammonia, total N, total P, true and apparent colour, salinity, metals, whole-effluent toxicity | Stricter colour units, micro-pollutant watchlist, PFAS in finishes |
| ZDHC Wastewater Guidelines 2.1 (commercial) | ZDHC Foundation (brand-adopted) | COD, BOD, TSS, TDS, colour, pH, metals, AOX, surfactants, per- and polyfluorinated substances | Already stricter than most UK minimum consents; brand audits ongoing |
Process Train: From Bar Screen to Polished Effluent
A modern UK textile effluent plant is a fixed process train: coarse screening, flow and load equalisation, DAF flotation, biological oxidation, tertiary polishing, sludge handling, and (for reuse sites) a membrane train. Each stage has a job; miss one and the next stage underperforms.
- Coarse screening — a rotary bar screen removes lint, fabric scraps, and packaging that would rag around pumps and shred MBR membrane fibres. Typical aperture 2–5 mm, automatic cleaning.
- Flow and load equalisation — 24–48 h buffer smooths pH, temperature, and salinity peaks from batch dyeing. Without it, biology suffers and salt shocks shorten the activated-sludge settle.
- DAF flotation — coagulated colour, suspended solids, oils, and fibre fines are floated with micro-bubbles. The DAF flotation unit typically handles 4–300 m³/h and removes 60–90% of suspended solids and a large fraction of disperse and reactive colour when paired with appropriate coagulants.
- Biological treatment — MBR (submerged 0.1 µm PVDF) or SBR. MBR gives a smaller footprint, near-zero TSS in the effluent, and a permeate that is reuse-ready.
- Tertiary polishing — FBR-Fenton or ozone to break the residual chromophores that biology cannot touch.
- Sludge dewatering — combined DAF and waste-activated sludge passes to a filter press for sludge dewatering before off-site disposal.
For the screening stage, a rotary bar screen sized to peak flow protects every downstream unit from ragging and pump damage — a cheap insurance policy compared to a blocked MBR module.
| Stage | Typical textile influent | Target after stage | Typical removal |
|---|---|---|---|
| Bar screen (2–5 mm) | Lint, rags, packaging | Solids-free liquor | >95% gross solids |
| Equalisation (24–48 h) | pH 4–12 swings, 1,000–3,000 mg/L COD | pH 7–9, 500–1,500 mg/L COD | Buffers peaks; modest BOD drop |
| DAF | 500–2,000 mg/L TSS, 200–1,000 Pt-Co colour | 50–200 mg/L TSS, <200 Pt-Co | 70–90% TSS, 50–80% colour with coagulant |
| MBR (0.1 µm PVDF) | 500–1,500 mg/L COD, TDS 2,000–10,000 mg/L | <100 mg/L COD, <1 NTU turbidity | 85–95% COD, >99% TSS |
| FBR-Fenton (1–5 mg/L Fe, 160 mg/L H₂O₂) | Residual 50–200 Pt-Co colour, COD 100–300 mg/L | <15 Pt-Co apparent colour | Up to 93% decolorisation; 80–93% COD (Su et al., 2011b) |
MBR vs SBR: Choosing the Right Biological Stage
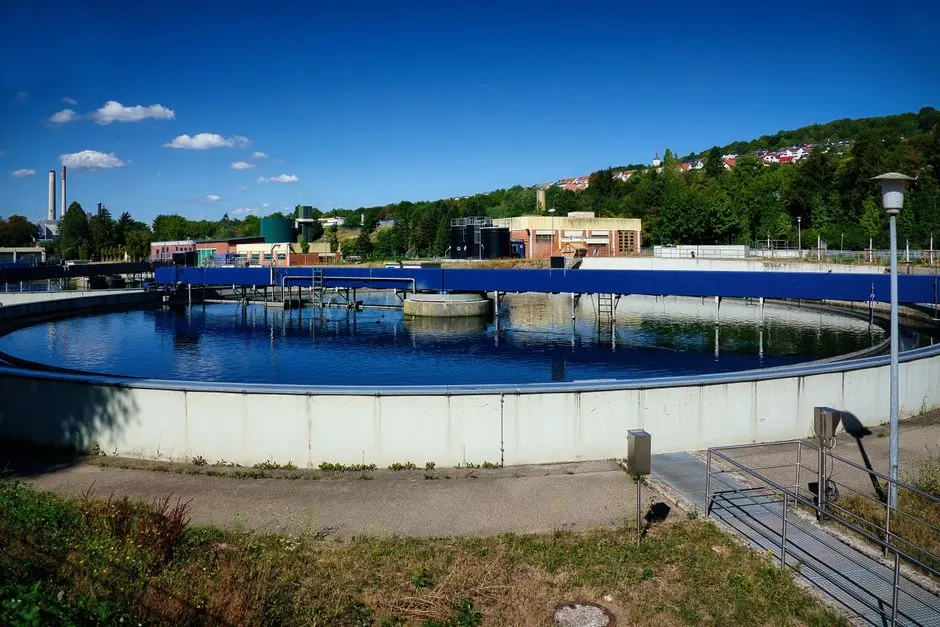
The two most common biological choices in UK textile plants are MBR and SBR. The decision is driven by reuse intent, footprint, and consent stability.
MBR uses a submerged PVDF membrane module, typically 0.1 µm nominal pore size, immersed in the aeration tank. An MBR membrane bioreactor system delivers a permeate with TSS effectively below detection and turbidity under 1 NTU, suitable for direct feed to RO. MBR tolerates higher mixed liquor suspended solids (8,000–12,000 mg/L) than CAS, which roughly halves the tankage needed. Field data on dyehouse MBRs shows stable 85–95% COD removal and significant azo-dye reduction when an anaerobic zone is included upstream. Drawbacks: membrane cleaning chemicals, aeration energy, and operator skill.
SBR runs a single tank in fill–react–settle–decant cycles. It has lower capital cost, simpler controls, and is forgiving of batch dyehouse loads. Effluent TSS is higher (typically 20–80 mg/L), so it is generally piped to sewer rather than reused. SBR suits 50–500 m³/d sites with intermittent flows and stable consents. Where SBR is paired with anaerobic/aerobic staging, biological colour work is meaningful: a microbial fuel cell study on real dye wastewater (Kumar Sonu et al., 2020, via ScienceDirect topic page) recorded 82.14% COD removal, 68% TDS removal, and 74.8% decolorisation simultaneously, showing the colour ceiling is biological when staging is right.
Decision rule of thumb: if reuse is planned, choose MBR with the DF membrane module; if discharge-only with a low-risk consent, SBR may be enough.
| Parameter | MBR (0.1 µm PVDF) | SBR |
|---|---|---|
| Typical flow range (UK textile) | 10–2,000 m³/d | 50–500 m³/d |
| Footprint vs CAS | ~40% of CAS | ~70% of CAS |
| Effluent TSS | <1 mg/L (effectively zero) | 20–80 mg/L |
| Reuse-ready permeate | Yes (RO feed) | No (additional filtration needed) |
| Operator skill | Higher (membrane CIP) | Lower (timer-based) |
| Capex vs SBR | ~1.3–1.6× | Baseline |
Tertiary Polishing: Ozone, Fenton and Activated Carbon
Tertiary polishing is where UK mills close the gap between an MBR permeate that is biologically clean but still coloured, and a discharge that the undertaker will accept. The three practical options are ozonation, Fenton (preferably FBR-Fenton), and activated carbon polishing.
Ozonation attacks chromophores fast. Ozonation alone reached only 28.5% COD removal in 30 minutes in Azbar et al. (2004) (via ScienceDirect topic page), but combined with a fluidised-bed reactor and granular activated carbon it reached 60% COD removal (Lin and Lai, 1999, via ScienceDirect topic page). A packaged ozone generator is the simplest add-on for the colour ceiling, and works well as a polishing step on MBR permeate.
FBR-Fenton is the heavy-lifter. Conventional Fenton needs around 400 mg/L Fe²⁺ and 550 mg/L H₂O₂ for full decolourisation (Badawy and Ali, 2006, via ScienceDirect topic page). FBR-Fenton achieves up to 93% decolorisation with just 1–5 mg/L Fe²⁺ and 160 mg/L H₂O₂ (Su et al., 2011b, via ScienceDirect topic page), because the carrier surface keeps iron in the reactive zone and reduces sludge. The same study found COD reductions of 80–93% on real dye wastewater. The chemistry and integration steps are covered in detail in this Fenton oxidation system guide.
Activated carbon (PAC or GAC) is the safety net for residual COD, trace organics, and any recalcitrant AOX, and is commonly placed as a final polish before RO or sensitive consents.
Reuse and ZLD: Closing the Loop on a UK Dyehouse
Once colour and COD are within consent, the next engineering question is reuse. A dyehouse that currently draws mains water at £1.50–2.50/m³ and pays sewerage on top has a payback lever that few other industrial sectors do. The ScienceDirect topic page notes that advanced treatment can effectively recover water from textile effluents and reuse it in production — the same finding ZDHC-aligned mills now cite in their sustainability reports.
Reuse trains pair UF with RO. UF handles turbidity, suspended solids, and most bacteria; an ultrafiltration system sized at 0.01–0.05 µm protects the RO from fouling. An industrial RO system then desalinates the UF permeate, achieving up to 95% recovery in single-pass or two-pass configuration. Hardness in textile feeds (especially from process additions) needs an industrial water softener upstream of the RO to prevent scale on membranes. Typical reuse ratios for a UK dyehouse are 30–50% of polished effluent, which can halve mains demand and reduce sewerage discharge volume in proportion. Full ZLD with evaporation and crystallisation is justified only at very small flows (<500 m³/d) or where a discharge consent is unobtainable — most UK sites stop at RO reuse.
Cost Shape and Decision Framework for 2026
CAPEX for a UK textile effluent plant is dominated by the biological stage (MBR roughly 1.3–1.6× SBR on a like-for-like flow) and any reuse membrane train. DAF and Fenton skid packages typically sit at 10–20% of the total CAPEX each; civil works, equalisation tanks, and the MBR tankage are the heavy civil items. OPEX is dominated by sludge disposal, Fenton reagents (H₂O₂ and Fe salt), ozonation power, RO membrane replacement, and brine disposal where ZLD applies. Directional CAPEX for a packaged 100 m³/d textile MBR plant (screen + DAF + equalisation + MBR + Fenton + sludge) sits in the low-single-digit £m range; larger 500 m³/d builds scale roughly linearly on flow with diminishing civil cost per m³. These figures are flow- and consent-dependent and should be confirmed against a site-specific enquiry.
A five-step decision framework covers the common cases:
- Confirm consent route — sewer trade-effluent or EPR 2010 direct discharge. This sets the target quality.
- Define reuse target — 0% (discharge only), 30–50% (RO reuse), or 100% (ZLD).
- Pick biological stage — MBR for reuse, SBR for low-risk discharge-only consents.
- Choose tertiary by colour limit — FBR-Fenton for high colour, ozone for moderate, GAC polishing for sensitive consents.
- Add reuse train if mains water >£2/m³ or consent is tightening — UF + RO plus softener, with brine management sized to consent.
For small UK sites (10–200 m³/d), containerised modular wastewater systems with MBR and DAF pre-integrated cut civil works, shorten permit timelines, and can be commissioned in weeks rather than months — a practical answer for mills that need a 2026 solution without a six-month build.
| Configuration | Indicative CAPEX share | Main OPEX drivers | Best fit |
|---|---|---|---|
| Discharge only (SBR + DAF + sludge) | DAF 15%, SBR 50%, civil 25%, sludge 10% | Sludge disposal, power | 50–500 m³/d, stable consent |
| Discharge (MBR + DAF + FBR-Fenton + sludge) | DAF 12%, MBR 45%, Fenton 15%, sludge 10%, civil 18% | Fenton reagents, sludge, power | 10–2,000 m³/d, tight consent |
| Reuse (above + UF + RO + softener) | Add UF+RO+softener ~25–30% | RO membrane replacement, energy, brine | Mains water >£2/m³, brand water targets |
Frequently Asked Questions
What is the typical consent limit for colour in a UK textile discharge?
There is no single UK number; trade-effluent consents from water companies commonly specify a true-colour limit in the 50–200 mg/L Pt-Co range (or an equivalent absorbance at 436 nm), with tighter values for direct-discharge EPR 2010 permits. ZDHC Wastewater Guidelines 2.1 sets stricter commercial targets that brand audits now enforce. (Source: ZDHC Foundation guidance, 2024; UK water company trade-effluent consent templates.)
Is MBR or SBR better for a small UK dyehouse?
SBR is usually the lower-CAPEX choice for flows of 50–500 m³/d where effluent goes to sewer with a low-risk consent. MBR is the better fit if the site plans water reuse, has a tight consent on TSS, or is constrained on footprint — the submerged 0.1 µm PVDF membrane gives near-zero TSS effluent and a permeate ready for RO. (Source: HydropureWater field data, 2026.)
Can textile effluent be reused for process water?
Yes. An MBR permeate polished by UF and RO can be reused for wash-water, rinsing, and lower-grade process applications, with recoveries up to 95%. An industrial softener upstream of the RO prevents hardness scaling, and 30–50% reuse can halve mains demand and sewerage charges for a typical dyehouse. (Source: ScienceDirect textile wastewater topic page; HydropureWater field data, 2026.)
How much does a UK textile effluent plant cost in 2026?
CAPEX is flow- and consent-dependent. As a directional guide, a packaged 100 m³/d MBR + DAF + FBR-Fenton plant sits in the low single-digit £m range, scaling roughly linearly on flow with diminishing civil cost per m³. Containerised MBR/DAF systems for 10–200 m³/d sites typically cut civil works and permit time significantly. (Source: HydropureWater field data, 2026 — directional only.)