Establish the Compliance Basis Before Choosing Equipment
Mining and metals plants near Belle meet sewer pretreatment limits by treating the discharge as a permitted industrial discharge, not by relying on a generic treatment package. The plant must establish the correct federal and state authorization, obtain the receiving POTW’s current local limits in writing, characterize each wastewater stream separately, and size treatment from peak flow and representative water quality data. This mining wastewater sewer-limit compliance workflow prevents equipment from being selected against an assumed or outdated discharge condition.
Start with the facility’s mineral-processing category, the applicable 40 CFR Part 436 subpart, NPDES coverage, state authorization, and any industrial user permit. A reserved subpart is not evidence that no requirement applies (HydropureWater, 2026). The Clean Water Act requires point-source discharges from mining operations, including discharges from associated impoundments, to be authorized under an NPDES permit (US EPA, 2026).
Then request the receiving POTW’s current local limits, prohibited discharges, monitoring rules, sampling requirements, and acceptance conditions in writing. Local limits are site-specific and may be numeric or narrative; they protect the POTW’s treatment process, sludge system, and receiving waters. POTWs impose local limits at the industrial user’s point-of-connection discharge to the POTW collection system (US EPA, S2).
Reconcile those requirements with NPDES conditions, state rules, the industrial-user permit, discharge authorization, monitoring obligations, and signed reuse or discharge conditions. The resulting compliance basis should identify the controlling documents in this order:
- The applicable federal and state discharge authorizations.
- The POTW’s sewer use ordinance, local limits, and industrial-user permit.
- Signed site conditions covering reuse, monitoring, reporting, and discharge.
- The facility records and representative wastewater data used for design and acceptance.
The supplied research does not establish Belle’s receiving POTW, industrial-user authorization, local limits, or numerical discharge standards. Those items must come from current official records. A generic article cannot fill that gap, and an equipment supplier should not be asked to assume local limits that have not been issued in writing.
Separate Every Wastewater Stream
Mine drainage, mineral-processing effluent, tailings-pond discharge, and dewatering water must be characterized separately because they can impose different limits on treatment capacity, chemical consumption, sludge handling, and discharge control. Combining them in equalization without characterization can dilute a high-concentration stream and obscure the mass load that governs treatment performance (AMPAC USA, 2025-09, as cited in HydropureWater research).
Acid mine drainage may carry dissolved metals including iron, manganese, copper, zinc, arsenic, and cadmium. Mineral-processing water can contain process chemicals and dissolved ore constituents, while tailings-pond effluent can contribute fine solids, processing chemicals, and leached metals (AMPAC USA, 2025-09, as cited in HydropureWater research). Dewatering discharge can change with local geology. The treatment objective therefore depends on the stream, not simply on the facility’s mining category.
Build a sampling program around four measured inputs: flow, pH, metals, and TSS. Add oil and grease, process-reagent residuals, and conductivity or TDS where they affect the selected treatment or reuse objective. Sampling must cover normal production, peak discharge, startup, shutdown, rainfall, and other material operating conditions before equipment sizing.
| Stream | Principal characterization | Decision before treatment selection |
|---|---|---|
| Mine drainage wastewater | Flow, pH, acidity, dissolved metals, and storm-event variability | Determine chemical dose and solids-separation capacity at the controlling condition. |
| Mineral processing effluent | Ore constituents, process-reagent residuals, conductivity or TDS, and relevant metals | Determine whether precipitation and polishing are sufficient or process-specific treatment is required. |
| Tailings-pond effluent | TSS, fine solids, metals, and residual process chemicals | Define solids capture, hydraulic capacity, and sludge disposition. |
| Dewatering discharge | Flow, pH, metals, TSS, and geology-dependent composition | Decide whether separate treatment or combined equalization provides a defensible control strategy. |
Calculate the controlling contaminant mass load from representative concentration and discharge flow. Low-concentration runoff must not be allowed to dilute a more difficult stream merely because both can enter the same tank. Segregation also simplifies chemical control, sludge handling, and reuse decisions.
Build a Treatment Train with a Measurable Purpose
A defensible treatment train assigns every unit operation a contaminant or control requirement, an operating indicator, and acceptance evidence. Equalization should buffer hydraulic and chemical variation; pH correction then establishes conditions for hydroxide precipitation of dissolved metals (Genesis Water Technologies; PMC review, 2024-02, as cited in HydropureWater research).
Coagulants and flocculants can aggregate suspended solids and fine metal particles into floc that can be separated. A dissolved air flotation system for mining wastewater can remove the resulting solids and floatable material, while lamella clarification provides an alternative solids-separation barrier. Multimedia filtration removes residual solids and colloids and protects downstream membranes.
Ultrafiltration is justified when fine colloids remain and a finer barrier is needed. The supplied product catalog describes a 0.03-micron UF barrier with automatic backwash and air scour; the same catalog specifies acceptance of up to 300 ppm turbidity for its UF system. Those are equipment specifications, not guaranteed site performance.
Reserve reverse osmosis for dissolved metals or salts that remain above the sewer requirement or reuse target. RO should not be added by default because it introduces a concentrate stream that must be managed. For a site using RO-enabled internal reuse, the supplied research reports a 40–60% reduction in freshwater intake compared with once-through operation, but the target must be validated through a mass balance that includes water retained in sludge, membrane concentrate, and other losses (AMPAC USA, 2025-09, as cited in HydropureWater research).
Use a PLC-controlled chemical dosing system where precipitation and floc performance depend on repeatable pH and reagent addition. The controls should preserve dose-to-flow relationships, record chemical use, and provide alarms for departure from the validated operating envelope.
| Treatment barrier | Measurable purpose | Acceptance evidence |
|---|---|---|
| Equalization | Buffer hydraulic and chemical variation. | Peak-flow operating record and equalization model. |
| pH correction and metals precipitation | Precipitate dissolved metals as separable solids. | Calibrated pH records, dosing trends, and jar or pilot results. |
| Coagulation, flocculation, and clarification | Remove suspended solids and formed metal-bearing floc. | TSS removal, solids-loading review, and sludge-generation data. |
| Multimedia filtration or UF | Remove residual solids and colloids; protect membranes. | Differential pressure, run time, turbidity, and applicable feed measurements. |
| RO | Remove dissolved metals or salts remaining above the required quality. | Validated permeate quality, recovery curve, and concentrate-management plan. |
| Sludge dewatering | Stabilize chemical-precipitation residues for a managed disposal route. | Measured cake volume, target dryness, cycle time, and receiving-site acceptance criteria. |
The supplied plate-and-frame press catalog covers filtration areas from 1 m² to 500 m² and manual, hydraulic, or fully automatic configurations (HydropureWater product catalog). Specify the press against actual precipitate properties rather than plate area alone.
Select Solids Separation by Wastewater Character
DAF and lamella clarification should be selected from the wastewater’s physical properties and the installation constraints, not from a generic preference for one technology. The supplied catalog describes DAF for suspended solids, FOG, oil and grease, and suitable colloidal matter across 4–300 m³/h and 13 standard models (HydropureWater product catalog).
DAF is the stronger candidate where buoyant floc, oil and grease, or floatable colloidal material is present. Lamella clarification is more relevant where sludge volume and available footprint constrain the installation. The supplied catalog specifies surface-loading rates of 20–40 m/h and up to 30% chemical-consumption reduction for the lamella system; these are selection values, not guaranteed project performance (HydropureWater product catalog).
| Decision factor | DAF | Lamella clarification |
|---|---|---|
| Preferred feed characteristic | Buoyant floc, FOG, oils, and suitable colloidal matter. | Precipitated or settleable solids with chemical flocculation. |
| Principal selection trigger | Floatable contaminants require effective solids capture. | Sludge volume or footprint is the governing constraint. |
| Bidder evidence required | Feed characteristics, flotation performance, float removal, and sludge handling. | Solids loading, chemical demand, settling performance, and underflow behavior. |
| Common comparison | Peak flow, TSS removal, chemical consumption, sludge generation, footprint, controls, and operator capability. | |
Require bidders to compare solids loading, chemical demand, underflow or float-removal performance, sludge generation, footprint, and utility requirements. A detailed comparison of DAF and clarifiers for mining wastewater provides the basis for that technical review, but the final selection still depends on representative effluent data.
Do not combine streams merely because they can share a tank. Separate treatment may simplify pH control, reduce chemical consumption, produce a more manageable sludge, or preserve a higher-quality stream for reuse. The high-efficiency sedimentation tank should be evaluated where compact solids separation is required, not installed merely because clarifier equipment is available.
Size from Peak Flow and Maximum Mass Loading
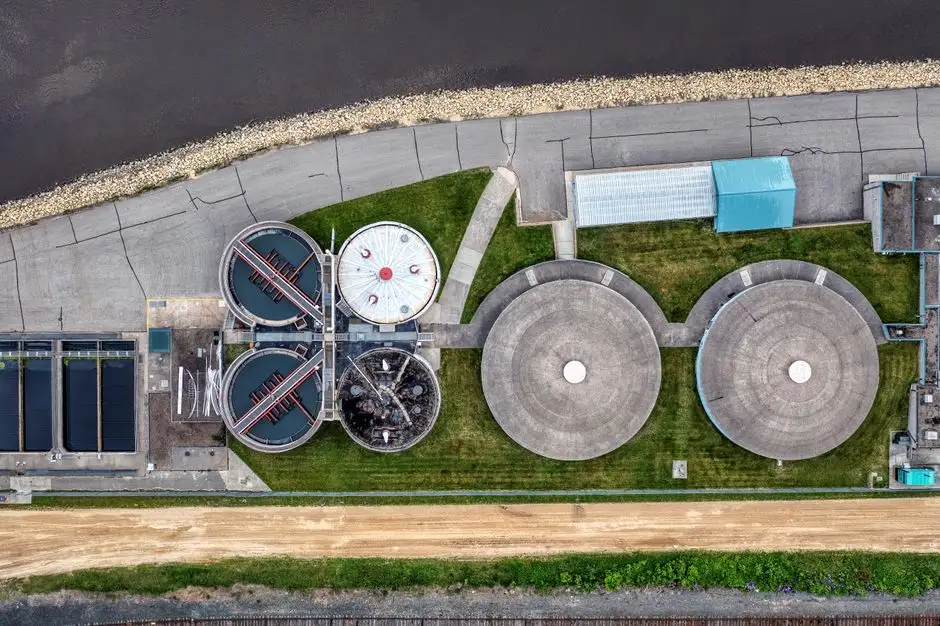
Equalization and pumping capacity must be based on the highest anticipated discharge rather than average flow (HydropureWater, 2026-02). A treatment train that meets an average-flow condition can still fail during production peaks, rainfall runoff, startup discharge, or shutdown release.
Calculate the controlling contaminant load from representative concentration and discharge flow. Equipment nameplate flow does not demonstrate adequate chemical, filtration, or membrane capacity. For each treatment barrier, require the bidder to state its design flow, maximum contaminant load, operating assumptions, and expected removal performance.
The quotation package should identify peak and average flow in m³/h, representative influent pH and metal results, POTW limits for pH, metals, and TSS, and the desired recovery percentage if reuse is in scope (HydropureWater, 2026-02). It should also provide chemical-consumption estimates, sludge-generation estimates, redundancy assumptions, and—where membranes are included—recovery and concentrate-management requirements.
For filtration and membrane stages, compare the proposed ultrafiltration system for membrane pretreatment and multimedia filtration equipment with the actual feed condition. The feed turbidity, residual solids, colloid load, operating recovery, and downstream water-quality objective determine whether those barriers belong in the train.
If reuse is part of the project, reconcile the expected freshwater reduction with a site-specific water balance. Account for sludge water, membrane concentrate, and other losses rather than transferring a generalized recovery percentage directly into the equipment guarantee (AMPAC USA, 2025-09, as cited in HydropureWater research).
The supplied research does not establish a Belle-specific pretreatment target or a universal industrial-scale cost. Those values must come from the current permit, POTW requirements, representative wastewater data, and a scoped supplier quotation.
Convert the Proposal into a Compliance and Procurement Checklist
Equipment acceptance should test the complete treatment logic, not only the completion of each vessel. A proposal should include a process flow diagram, mass balance, sample locations, chemical-storage details, residual-sludge destination, controls, redundancy, and stream-segregation plan.
| Submission item | Information the buyer should require |
|---|---|
| Design basis | Peak and average flow in m³/h; representative influent pH, metals, and TSS; controlling operating event; applicable POTW limits. |
| Process performance | Removal objectives by stage, chemical demand, sludge generation, filter or membrane operating limits, and reuse recovery where applicable. |
| Controls | pH setpoints, flow-paced dosing, alarms, data recording, fail-safe behavior, and operator interface. |
| Solids route | Residual-sludge destination, dewatering basis, cake acceptance criteria, storage, transport, and disposal documentation. |
| Compliance | Sample points, analytical methods, monitoring frequency, record-retention approach, bypass authority, notification duties, and restart criteria. |
| Delivery | Scope boundaries, manufacturing schedule, delivery schedule, site erection requirements, commissioning plan, and training deliverables. |
Define sampling points for untreated streams, equalization, chemical treatment, clarification, filtrate, and final discharge. This arrangement makes it possible to trace an excursion to source chemistry, dosing, solids separation, filtration, or membrane performance instead of treating the whole train as an unexplained failure.
Require verification of pH setpoints, dosing trends, TSS-removal performance, filter or membrane differential pressure, RO recovery where applicable, and sludge-generation records. A plate-and-frame filter press for precipitated mining sludge should be accepted against measured cake volume, target dryness, cycle time, and receiving-site criteria rather than an unqualified throughput claim.
Require written alarm, bypass, upset, and high-flow procedures. Each procedure should identify isolation points, permitted storage, sampling duties, notification responsibilities, and restart criteria. An equipment failure must not become an unpermitted discharge because the operating procedure was left to the equipment manufacturer.
Numerical monitoring frequencies, sampling methods, and compliance triggers must come from the current permit, industrial-user authorization, and POTW requirements. Keep each operating record traceable to the requirement it demonstrates.
Frequently Asked Questions
What information is needed to get a defensible pretreatment quotation for a mine or metals plant near Belle?
Request the current POTW local limits and prohibited-discharge rules, the industrial-user permit or proposed authorization, NPDES and state conditions, peak and average flow, representative pH, metals, and TSS results, the controlling operating event, reuse objectives, and the residual-sludge destination. Without the controlling limits and representative wastewater data, a supplier can quote equipment but cannot show that the proposed train satisfies the discharge condition.
Should DAF, a lamella clarifier, or UF be selected first for mining wastewater?
Start with the contaminant and separation objective. DAF is appropriate where buoyant floc, FOG, oils, or floatable colloidal material must be removed; lamella clarification is relevant where settleable solids and footprint drive the selection; UF is appropriate when fine colloids remain and a finer membrane barrier is needed. Each must still be placed within a treatment train defined by the final effluent requirement.
How much does a mining wastewater pretreatment system cost?
A defensible price cannot be stated without the site-specific treatment basis. Request a capital and operating cost breakdown covering equalization, pH correction, precipitation, solids separation, filtration, membranes, controls, chemical storage, sludge dewatering, utilities, startup, and disposal. Also request chemical-consumption and sludge-disposal assumptions. Do not accept a universal price that omits Belle’s verified limits, peak flow, wastewater chemistry, or reuse objective.
How should a supplier demonstrate that the equipment will meet the sewer limit?
Require a stage-by-stage process flow diagram, mass balance, representative influent data, calculation of the controlling mass load, and performance evidence for each removal barrier. Require a supplier comparison covering solids-separation equipment and compliance evidence, plus defined acceptance tests for pH, metals, TSS, filter or membrane conditions, and sludge generation.
What compliance risks arise if high-concentration streams are diluted before treatment?
Dilution can lower measured concentration without reducing the pollutant mass entering the sewer. It can also conceal the chemical demand, sludge yield, and peak treatment load that determine whether the equipment performs adequately. Sampling each stream separately before combining them preserves the evidence needed to demonstrate compliance at the point-of-connection discharge.