Which Rules Actually Apply to a Kelso Fabricated Metals Plant
40 CFR Part 433 (Metal Finishing) is the binding categorical standard for any fabricated metals plant near Kelso that runs an in-house plating, anodizing, or chromic acid tank, and the rule covers forming, finishing, forging, foundry, metal spraying, and machining wash operations that sit on the same site as those wet processes (per 40 CFR Part 433). A stamping-only shop that ships dry parts to an off-site finisher is generally outside the category, but a facility with its own zinc, nickel, or chromic acid line is inside it from the day the tank is filled. The rule splits its limits into PSES (Pretreatment Standards for Existing Sources) and PSNS (Pretreatment Standards for New Sources), and PSNS is the tighter of the two because it applies to sources constructed after the rule's promulgation date. Most POTW pretreatment programs enforce PSNS-equivalent local limits on all industrial users as a conservative baseline, so even a 1980s-era plant should design to PSNS numbers when it replaces equipment in 2026.
On top of the federal rule, a Cowlitz County plant must hold a Washington Department of Ecology Industrial Stormwater General Permit (ISGP) whenever any process water contacts stormwater runoff, and the local Cowlitz County POTW applies its own limits developed under 40 CFR 403.5. The practical sequence for a compliance audit is therefore: confirm Part 433 applies, pull the PSNS column, then pull the Cowlitz County local-limits table, and design to whichever value is stricter on each parameter.
The Federal-vs-Local Limits Envelope
40 CFR Part 433 sets PSES and PSNS limits for cadmium, total chromium, copper, lead, nickel, silver, zinc, and total toxic organics, while local POTW limits developed under 40 CFR 403.5 are always at least as stringent and in practice add the parameters the categorical rule underweights — copper, nickel, zinc, lead, and silver caps, plus oil and grease, total suspended solids, and pH (per 40 CFR 403.5). The plant must meet whichever limit is stricter on each parameter, which is why the design envelope is built from the POTW table rather than the federal table alone. The right mental model is: federal categorical standards are the floor, local POTW limits are the ceiling the plant has to hit, and the binding number lives in the column with the lower value.
| Parameter | 40 CFR Part 433 PSES (daily max, mg/L) | 40 CFR Part 433 PSNS (daily max, mg/L) | Typical Cowlitz County POTW local limit (mg/L) | Binding limit |
|---|---|---|---|---|
| Cadmium | 0.69 | 0.11 | 0.10 | POTW / PSNS tie |
| Total chromium | 2.77 | 0.86 | 0.50 | POTW |
| Copper | 3.38 | 0.86 | 0.50 | POTW |
| Lead | 0.69 | 0.43 | 0.20 | POTW |
| Nickel | 3.98 | 1.10 | 0.50 | POTW |
| Silver | 0.43 | 0.24 | 0.10 | POTW |
| Zinc | 2.61 | 1.48 | 1.00 | POTW |
| Oil & grease | — | — | 100 | POTW |
| TSS | — | — | 200 | POTW |
| pH (s.u.) | — | — | 6.0–9.0 | POTW |
Where the federal column shows "—", the limit is set locally rather than categorically, and the POTW column governs. For all metals except cadmium, the Cowlitz County local limit is the binding number in practice, which is why pretreatment design near Kelso is dominated by the POTW envelope and not by 40 CFR Part 433 alone.
The Four Contaminant Families a Kelso Floor Actually Generates
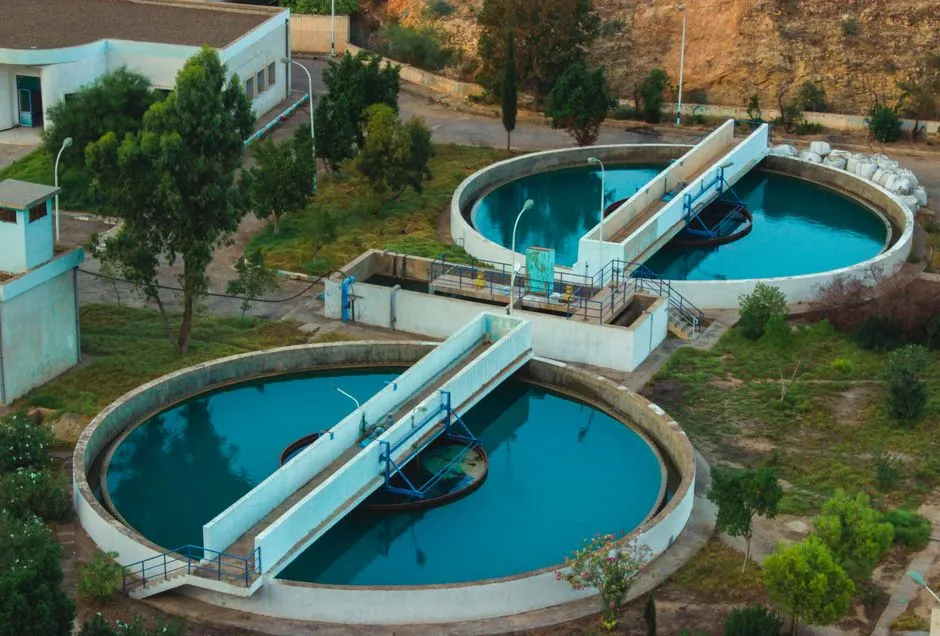
Most fabricated metals floors generate the same four contaminant families regardless of the specific process mix: free and emulsified oils from stamping, machining, and drawing compounds; dissolved heavy metals (Zn, Ni, Cu, Cr, Pb, Cd) from plating rinsewater and acid pickling; hexavalent chromium from chromic acid anodizing, hard chrome, and conversion coating; and total suspended solids from grinding swarf, casting sand, and hydroxide floc carryover (HydropureWater field data, 2026). Cyanide appears wherever alkaline cyanide plating (Zn, Cu, Cd, Ag) is still in use, and it must be destroyed before metals precipitation or it resolubilizes the precipitates downstream and turns the clarifier effluent into a violation.
Typical operating ranges for a mixed floor drain entering pretreatment are oils at 50–500 mg/L, total dissolved metals at 5–200 mg/L, TSS at 100–1,000 mg/L, and pH swinging between 2 and 12 across batch dumps (HydropureWater field data, 2026). A stamping cell may hold pH at 7 with low metals; a hard chrome line will spike Cr(VI) above 50 mg/L and drop pH below 2 on a rinse dump. Plating shops run batch dumps rather than steady flow, so equalization is not optional — it is the unit operation that makes every chemistry stage downstream work. Sample a full week of composite flow before specifying equipment, because a four-hour composite that misses the Friday afternoon dump will undersize the equalization basin and propagate that error into every downstream unit. A ZSQ series dissolved air flotation system sized off the right composite handles the FOG and colloidal fines the chemistry stage cannot reach on its own.
The Standard Treatment Train and Where Each Unit Sits
The standard sequence a fabricated metals plant uses to hit PSNS-equivalent POTW limits is: rotary bar screen, flow equalization, oil and grease removal, hex chrome reduction, cyanide oxidation, hydroxide precipitation, DAF or lamella clarification, pH trim, and final polishing. Each step has a defined purpose, a defined outlet spec, and a defined failure mode if it is skipped, and the train is best audited step by step rather than as a black box.
- Rotary mechanical bar screen. A rotary mechanical bar screen upstream of the equalization basin keeps rags, wipes, and tramp metal out of the sludge train, which is the single most common cause of premature press-cloth failure on metal hydroxide.
- Flow equalization. Outlet spec: pH smoothed to 6–9, flow coefficient of variation under 0.5. This stage makes the chemistry downstream possible at all.
- Oil and grease removal. Skim and break emulsions before metals chemistry; emulsified oil that survives into the precipitation stage coats floc and ruins settling.
- Hexavalent chrome reduction. Sodium metabisulfite (or ferrous sulfate) at pH 2–3 with ORP held at 250–300 mV reduces Cr(VI) to Cr(III); the trivalent form then precipitates as Cr(OH)3 in the pH 8.5–9.5 precipitation stage where Cr(VI) hydroxide would otherwise remain soluble.
- Cyanide oxidation. NaOCl at pH 10–11 destroys free and WAD cyanide before metals precipitation; never let cyanide into the clarifier.
- Hydroxide precipitation. NaOH or lime lifts pH to 8.5–9.5 to drop dissolved metals as M(OH)n; pH band is the most important control loop on the skid.
- DAF or lamella clarification. Solid–liquid separation; sizing rules are covered in the next section.
- pH trim. Final effluent to 6.0–9.0 before the POTW sample port.
- Sludge dewatering. Floated metal hydroxide runs 2–5% dry solids out of the DAF and dewaters to 25–35% with a plate-and-frame filter press; a belt press caps out around 22% DS on metal hydroxide.
All four chemicals — NaOH or H2SO4 for pH trim, sodium metabisulfite for chrome reduction, NaOCl for cyanide destruction, and anionic or cationic polymer for floc — are dosed through a PLC-controlled automatic chemical dosing skid with feedforward (flow-paced) and feedback (pH/ORP) control. Skid-mounting cuts field install time, forces the integrator to bench-test the interlocks before shipment, and gives the operator one panel to lock out. Alarm and shutdown interlocks on pH excursion, ORP out of range, and high TSS should automatically divert flow back to the equalization basin header so a chemistry upset does not become a discharge violation.
DAF vs Lamella for Cowlitz County Winter Conditions
The right primary for a fabricated metals floor near Kelso is not the FOG-heavy food-processing case most 2026 DAF articles default to. DAF wins on FOG, colloidal fines, footprint, and float dryness, while lamella wins on CAPEX for FOG-free streams at very high flow with sludge recycle cutting coagulant use by up to 30% (HydropureWater field data, 2026). Footprint is decisive: a DAF at 0.2–0.4 m² per m³/h is roughly one-twentieth the footprint of a conventional clarifier at 5–8 m² per m³/h, and on a space-constrained Cowlitz County industrial site that gap often swings the decision toward DAF regardless of unit CAPEX (HydropureWater field data, 2026).
| Criterion | DAF (ZSQ series) | Lamella with sludge recycle |
|---|---|---|
| Best-fit stream | FOG, cutting oil, colloidal fines, variable influent | Dense settleable hydroxide floc, high flow, no oil |
| Surface loading / hydraulic capacity | 4–20 m/h on floc density | 20–40 m/h on plate-pack projected area |
| A/S ratio | 0.005–0.060 (0.02 typical) | n/a |
| Recycle rate | 10–30% of forward flow | Internal sludge recirculation |
| CAPEX multiplier at equal flow (lamella = 1.0x) | 1.5–2.5x | 1.0x |
| Power draw | 8–15 kWh/m³ (compressor + recycle) | 0.1–0.3 kWh/m³ + much larger drive |
| Power cost at 8–12 ¢/kWh | $0.65–$1.80 per m³ treated | Negligible vs chemical savings |
| Float / underflow dry solids | 4–8% DS float | 2–5% DS underflow |
| Coagulant savings vs base dose | Base | Up to 30% via sludge recycle |
| Cold-weather performance (<10°C) | 10–15% sizing margin; heat-trace recycle and saturation vessel | Sludge-hopper freeze risk in unheated vault |
| FOG, emulsified oil, colloidal fines | Handled in primary | Not handled; requires upstream or polish step |
| 2026 role in a metals-fab train | Primary when FOG > 50 mg/L | Primary for FOG-free dense floc, or polish after DAF |
Micro-bubble nucleation kinetics slow 20–30% at 5°C versus 20°C, so a 10–15% sizing margin on the recycle pump and saturation vessel is prudent for plants that run through Kelso winters, and heat-tracing the recycle line and insulating the saturation vessel is often required (HydropureWater field data, 2026). Kelso winter ambient temperatures frequently sit in the 0–8°C range from November through March, which pushes the margin to the conservative end. The same cold snap creates a sludge-hopper freeze risk in an unheated lamella vault — a design risk a DAF skid does not carry. For a metals-fab shop with 50–200 mg/L emulsified cutting oil, a ZSQ series dissolved air flotation system is non-negotiable as primary because a lamella would discharge emulsified oil straight to the outfall and trip the 40 CFR Part 433 oil-and-grease envelope as well as the Cowlitz County TSS limit, and a lamella with sludge recirculation sits downstream as a polish step. The DAF-vs-lamella sizing logic for the lower Columbia basin covers the same trade-off in more depth on adjacent mining and metals streams.
When a Polishing Stage Is Worth Designing In Now
Most fabricated metals plants hit sewer limits with the standard train and never need polishing. The cases that do are predictable: the POTW tightens local limits below PSNS, the plant wants to reuse rinsewater and needs RO-quality feed, or a new rule forces a polish stage. For BOD/COD tightening or water reuse, a submerged PVDF MBR system delivers sub-1 μm filtration and stable effluent that can be sent to cooling-tower makeup or rinsewater reclaim. For sub-ppm TDS or specific metal caps such as nickel under 0.1 mg/L, an RO system is required, and the multi-media filter upstream must hold SDI15 below 3 or the RO membranes fail early.
For the PFAS question, anion exchange or granular activated carbon is the proven polish step for the long-chain PFAS species tied to chrome plating, and EPA has a 2026 PFAS rulemaking scoped to chrome finishing facilities with no current numerical limit (per EPA Metal Finishing Effluent Guidelines page). The right 2026 move is to design the pretreatment train so a polish skid can be bolted on later — not to install it now and pay to operate it ahead of any actual limit. Closed-loop zero liquid discharge is rarely economic for a fabricated metals plant unless water scarcity or a specific reuse-economics case supports the capital, and the 2026 PFAS removal options for chrome finishing walk through the polish-stage candidates in more detail. The chemical precipitation engineering for dissolved metals reference covers the upstream chemistry that has to be right before any polish stage is worth specifying.
Frequently Asked Questions
Does 40 CFR Part 433 apply to a stamping-only fabricated metals plant near Kelso?
No, not by itself. A stamping cell that ships dry parts to a separate off-site finisher is generally outside the Metal Finishing point source category. The rule attaches the moment the plant runs its own zinc, nickel, or chromic acid tank, or co-locates a machining wash operation with a plating or anodizing line (per 40 CFR Part 433).
What are the binding effluent limits a Cowlitz County POTW enforces in 2026?
Local limits developed under 40 CFR 403.5 are always at least as stringent as the federal categorical standards, and in practice the Cowlitz County POTW sets caps on copper, nickel, zinc, lead, silver, oil and grease (100 mg/L), TSS (200 mg/L), and pH (6.0–9.0). The plant meets whichever limit is stricter on each parameter, so the design envelope is built from the POTW table rather than the federal table alone.
What ORP and pH control bands are required for hexavalent chrome reduction?
Hexavalent chrome is reduced to trivalent chrome with sodium metabisulfite (or ferrous sulfate) at pH 2–3 with ORP held at 250–300 mV, and the trivalent form then precipitates as Cr(OH)3 at pH 8.5–9.5 in the downstream precipitation stage where Cr(VI) hydroxide would otherwise remain soluble.
How does a Kelso winter change DAF sizing versus a temperate site?
Micro-bubble nucleation kinetics slow 20–30% at 5°C versus 20°C, so the recycle pump and saturation vessel should carry a 10–15% sizing margin for plants that run through Kelso winters, and the recycle line plus saturation vessel typically need heat-tracing and insulation when ambient temperatures sit in the 0–8°C range from November through March (HydropureWater field data, 2026).
What should a fabricated metals plant do about the 2026 EPA PFAS rulemaking for chrome finishing?
EPA has a 2026 PFAS rulemaking scoped to chrome finishing facilities with no current numerical limit, so the right move is to design the pretreatment train so an anion exchange or GAC polish skid can be bolted on later, rather than installing and operating one ahead of an actual limit. RO is only worth specifying if a specific reuse case or sub-ppm nickel cap drives it.