Why High-Salinity Wastewater Demands MVR Evaporation Over Traditional Methods
MVR evaporation concentrates industrial streams with TDS above 50,000 mg/L at roughly 0.1–0.3 kWh per kilogram of evaporated water and recovers about 95% of the water as condensate. A 10 m³/h MVR system handling calcium chloride wastewater at 100,000 mg/L TDS can hold energy demand near 0.1 kWh/kg, support China's GB 31573-2015 direct-discharge limits for inorganic chemical industry, and require 50–300 kW of compressor power with 100–500 m² of heat exchanger area, while applying a Boiling Point Elevation (BPE) correction of 5–15°C.
High-salinity streams resist boiling because dissolved salts depress vapor pressure and raise the required boiling temperature by 5–15°C above pure water once TDS exceeds 50,000 mg/L. Conventional multi-effect distillation (MED) pays that penalty with 0.5–1.0 kWh/kg of steam-driven evaporation. Thermal crystallizers sit higher at 1.2–1.5 kWh/kg. MVR compresses the vapor leaving the evaporator, raises its saturation temperature by 5–10°C, and returns that vapor as the heating medium. Most plants we size for textile or chemical brine run at the lower end of the 0.1–0.3 kWh/kg band once condensate preheat is in place.
ZLD regulation is the main reason procurement teams revisit the choice today. China's GB 31573-2015 applies to inorganic chemical industry effluents, not petrochemical or coal-chemical discharges. The EU's Industrial Emissions Directive (IED) 2010/75/EU and the U.S. EPA's 40 CFR Part 437 both push operators toward Best Available Techniques (BAT) for brine management. In one Jiangsu textile plant, switching from MED to MVR at TDS 80,000 mg/L cut dye-wastewater disposal costs by 60%, largely because the brine could be concentrated instead of hauled.
| Technology | Typical Energy Consumption (kWh/kg evaporation) | Applicable TDS Range (mg/L) | Boiling Point Elevation (BPE) Impact |
|---|---|---|---|
| Mechanical Vapor Recompression (MVR) | 0.1 – 0.3 | 50,000 – 250,000+ | Managed through BPE correction & compressor design |
| Multi-Effect Distillation (MED) | 0.5 – 1.0 | 10,000 – 80,000 | Significant energy penalty for high TDS |
| Thermal Crystallizers | 1.2 – 1.5 | 100,000 – 300,000+ | High energy demand, suitable for final concentration |
How MVR Evaporation Works: Process Flow and Critical Engineering Parameters
An MVR evaporation system compresses the low-pressure vapor leaving an evaporator and reuses its latent heat inside the same vessel, so external steam input drops to almost zero once the loop is warm. The standard train starts with pre-treatment (filtration, pH trim), then evaporation, vapor compression by an electric centrifugal or axial compressor, condensation on the heat-exchanger side, and finally either brine recycle, downstream crystallization, or sludge dewatering with a high-efficiency plate and frame filter press. The compressor typically lifts the vapor by 5–10°C and 0.05–0.15 bar depending on BPE.
Four parameters decide whether a given MVR system will meet nameplate capacity. Evaporation capacity usually runs 1–50 m³/h for industrial units. Compressor power sits between 50–300 kW for that same band. Heat exchanger area of 100–500 m² covers most of the throughput range, with stainless plate or shell-and-tube geometries depending on fouling risk. BPE correction of 5–15°C at TDS 50,000–200,000 mg/L sets both compressor lift and the temperature gap driving the heat exchanger. A superheat eliminator upstream of the compressor removes entrained droplets and can shave 20–30% off compressor load on multi-effect MVR designs.
Heat integration matters as much as the compressor itself. Sensible-heat recovery from the hot condensate, usually with a plate preheater, drops the latent load the evaporator must deliver and brings the steady-state kWh/kg closer to 0.1 than to 0.3. For wastewater streams with high oil and grease content, a DAF system ahead of the MVR protects the heat exchanger from organic fouling, which is the single most common cause of capacity loss we see in operating plants.
| Parameter | Typical Range | Significance for High Salinity |
|---|---|---|
| Evaporation Capacity | 1 – 50 m³/h | Determines overall system footprint and throughput |
| Compressor Power | 50 – 300 kW | Increases with higher evaporation rates and BPE |
| Heat Exchanger Area | 100 – 500 m² | Sized for efficient heat transfer of recompressed vapor |
| Boiling Point Elevation (BPE) Correction | 5 – 15°C (for TDS 50,000–200,000 mg/L) | Directly impacts required operating temperature and energy demand |
| Superheat Eliminator Efficiency Gain | 20 – 30% reduction in compressor load | Improves vapor quality to compressor, reducing mechanical stress |
| Feed Preheating (via Condensate) | Significant energy savings | Reduces latent heat demand in the evaporator |
MVR System Design: Sizing Compressors, Heat Exchangers, and Evaporators for High-Salinity Wastewater
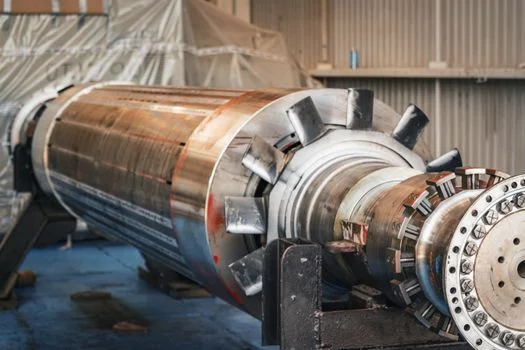
Compressor power sets both the operating cost and the electrical infrastructure, so it is sized first. The standard relation is Power (kW) = (Evaporation rate (kg/h) × Δh_vap (kJ/kg)) / (3600 × η_compressor), with η_compressor typically 0.7–0.85 for industrial centrifugal or axial units (HydropureWater internal design data, 2025). High-salinity streams raise Δh_vap because BPE forces a larger temperature lift, and the higher vapor density demands a more conservative surge margin on the compressor map.
Heat exchanger area is then calculated as Area (m²) = Q (kW) / (U × ΔT_lm). Stainless-steel plate exchangers in MVR service usually show U of 1,500–2,500 W/m²·K, and ΔT_lm drops to 5–10°C for high-salinity brine because BPE eats into the available temperature difference. That is why high-TDS MVR units look physically larger than low-TDS evaporators of the same capacity. Forced circulation is the default for viscous or scaling feeds such as calcium chloride; falling film works for clean, low-scaling liquids; plate evaporators win on footprint where fouling is mild. For organic-rich feeds, pre-treatment such as advanced oxidation reduces organic load and protects the heat transfer surface from fouling.
BPE estimation follows a rough empirical rule for NaCl: ΔT_BPE ≈ (TDS (mg/L) / 10,000) × 0.5°C. Calcium chloride and magnesium chloride brines run hotter than NaCl at the same TDS, so the rule under-predicts lift and a detailed calculation that accounts for ionic interactions is mandatory before final sizing.
| Component | Sizing Equation/Rule of Thumb | Key Considerations for High Salinity |
|---|---|---|
| Steam Compressor Power | Power (kW) = (Evaporation rate (kg/h) × Δh_vap (kJ/kg)) / (3600 × η_compressor) | Higher Δh_vap due to BPE, increased vapor density requires robust design |
| Heat Exchanger Area | Area (m²) = Q (kW) / (U × ΔT_lm) | Lower ΔT_lm due to BPE necessitates larger area (U: 1,500–2,500 W/m²·K, ΔT_lm: 5–10°C) |
| Evaporator Type | Forced Circulation, Falling Film, Plate | Forced circulation preferred for high viscosity/scaling (e.g., CaCl₂) |
| Boiling Point Elevation (BPE) | ΔT_BPE ≈ (TDS (mg/L) / 10,000) × 0.5°C (Empirical for NaCl) | Requires precise calculation for specific salt compositions; higher BPE for CaCl₂, MgCl₂ |
Cost Breakdown: MVR Evaporation vs. Multi-Effect Distillation and Crystallization
CapEx per m³/h of capacity is the easiest line item to compare across vendors. MVR systems typically land at $800–$1,500 per m³/h of installed capacity. Multi-effect distillation sits lower at $600–$1,200/m³/h because the pressure vessels are simpler, but the OPEX gap reverses the ranking within 2–3 years. Crystallizers for full ZLD are the most expensive at $1,200–$2,000/m³/h and are usually added downstream of an MVR rather than as a stand-alone concentrate.
OPEX for MVR is dominated by compressor electricity, which makes up 60–70% of the running cost, with maintenance 10–15%, labor 5–10%, and cleaning chemicals 5–10%. Steam-driven MED systems put a much larger share of OPEX into boiler fuel. Worked example: a 10 m³/h MVR unit at $120,000 CapEx that saves $50,000 a year in disposal and energy pays back in roughly 2.4 years. Ancillary equipment has to be priced in: a dissolved air flotation (DAF) unit for oil and grease, plus a plate and frame filter press for the brine sludge, each adds about 10–20% to total CapEx. A High-Efficiency Sedimentation Tank (Lamella Clarifier) is a common choice upstream of the MVR when suspended solids are the dominant foulant.
| Technology | Typical CapEx ($/m³/h) | Typical OPEX (Electricity Dominant) | Primary Advantage | Primary Disadvantage |
|---|---|---|---|---|
| MVR Evaporation | 800 – 1,500 | Low (0.1–0.3 kWh/kg) | Energy Efficiency, Low OPEX | Higher initial CapEx than basic MED |
| Multi-Effect Distillation (MED) | 600 – 1,200 | High (0.5–1.0 kWh/kg) | Lower initial CapEx | High energy consumption, less suitable for high TDS |
| Crystallization | 1,200 – 2,000 | Moderate to High (depends on downstream dewatering) | Near-complete solid recovery, ZLD compliance | Highest CapEx, complex operation |
Compliance and Zero-Liquid Discharge: How MVR Effluent Meets Global Standards
MVR handles dissolved salts but not residual organics or ammonia, so the condensate still needs polishing to meet ZLD discharge numbers. Under China's GB 31573-2015 for inorganic chemical industry, Table 1 direct discharge requires COD below 50 mg/L and ammonia below 10 mg/L (MEE, 2015), which is why most ZLD trains pair the MVR with an MBR (Membrane Bioreactor) system on the condensate line; an MBR polish typically lands below 30 mg/L COD and below 5 mg/L ammonia in operating plants. In the EU, IED 2010/75/EU frames BAT Reference Documents (BREFs) for chemical-sector wastewater management, which gives a defensible compliance route for facilities pursuing BAT-AELs. The U.S. EPA's 40 CFR Part 437 covers centralized waste treatment (CWT) facilities and sets limits for metals, oil and grease, TSS, and selected organics; it does not set a TDS cap, and metal-products and machinery oily wastes are regulated under 40 CFR Part 438 rather than Part 437. A Zhejiang petrochemical plant reached full ZLD with an MVR + crystallizer train, taking TDS from 150,000 mg/L in the raw brine to under 50 mg/L in the final effluent. Operators should also review regional rules such as the UK industrial wastewater treatment guidelines before locking the design.
Who This Guide Is For, Who Should Look Elsewhere, and the Next Step
This page is for plant engineers, EPC contractors, and procurement managers sizing brine concentration or ZLD trains for TDS above 50,000 mg/L in chemical, petrochemical, textile, refinery, or metal-finishing service. It is not the right starting point for low-salinity reuse (typically RO or ion exchange), for thermal desalination of seawater at TDS around 35,000 mg/L, or for very small flows under 1 m³/h where packaged MED still wins on capital. Selection checklist before issuing an inquiry: confirm influent TDS and salt species (NaCl vs CaCl₂ vs mixed), required distillate quality (COD, ammonia, TDS), available electrical capacity for the compressor, footprint and headroom, BPE estimate at design point, pre-treatment for oils and suspended solids, sludge-handling plan for the brine, and the payback horizon your finance team expects. Send the feed analysis and target recovery to HydroPure Water for a sized proposal and CAPEX/OPEX breakdown tailored to your duty point: request a quote for an MVR evaporation system.
Frequently Asked Questions
What is the maximum salinity MVR can handle?
MVR systems routinely handle salinities up to about 250,000 mg/L TDS, including NaCl and CaCl₂ brines. Above 100,000 mg/L, BPE rises sharply, so compressor power and heat-exchanger area both increase. Beyond 250,000 mg/L, most designs shift to a hybrid MVR-plus-crystallizer train for final solids recovery.
What limits MVR evaporation on high-salinity brine?
BPE, fouling, and compressor lift set the practical ceiling. Higher salt load forces a larger temperature rise and denser vapor, which raise power draw and exchanger area. Oils, organics, and scale formers cut heat-transfer rates unless pre-treatment is sized correctly. Electrical capacity and available footprint often constrain the duty before the evaporator itself does.
How does MVR compare to reverse osmosis (RO) for high-salinity wastewater?
RO is generally limited to TDS below about 70,000 mg/L and needs heavy pre-treatment against fouling and scaling. High-salinity streams often exceed RO operating limits and membrane life. MVR treats much higher salinities with less sensitivity to dissolved-salt fouling, so it is usually the more robust option once TDS leaves the RO window.
What recovery can MVR reach before crystallization is required?
Most high-salinity MVR trains recover about 95% of the feed as condensate when TDS starts above 50,000 mg/L. Further concentration toward 250,000 mg/L or solid salt needs a crystallizer or hybrid step. Scaling risk and BPE, not pump capacity alone, usually decide when to stop the MVR stage.
What are the energy consumption benchmarks for MVR?
For high-salinity streams at TDS 50,000–200,000 mg/L, MVR typically uses 0.1–0.3 kWh/kg of evaporated water. MED often needs 0.5–1.0 kWh/kg on similar duties. Thermal crystallizers commonly require 1.2–1.5 kWh/kg for final concentration.