Why Chrome 6 Free Pretreatment Matters in 2026
Hexavalent chromium is classified as a substance of very high concern under regimes such as EU REACH (Qualicoat UK & Ireland). For an industrial plant, EHS, or pretreatment engineer, the benefits of switching to chrome-6-free processes cluster into four categories: environmental, occupational health, regulatory, and operational/performance. Each category maps to a different stakeholder in a project meeting: the wastewater engineer hears the first, the safety manager hears the second, the compliance lead hears the third, and the production manager hears the fourth. Treating them as separate lines of an internal justification memo is the most defensible way to build the case for capital approval.
The transition is not new or speculative. QUALICOAT UK & Ireland notes that some of its members have operated chrome-free systems for over twenty years, and globally collated test results from the QUALICOAT Association confirm chrome-free pretreatment systems offer the same protection as their chrome counterparts (Qualicoat UK & Ireland). That track record matters because pretreatment engineers are typically asked to demonstrate long-term field performance on the specific alloys and paint systems in their facility before qualifying a new chemistry, and a two-decade commercial reference base is a strong starting point.
The NCCA also documents the industry-wide conversion on aluminium coil lines, noting that by the year 2000 successful uses of chrome-free treatments were being demonstrated on aluminium extrusion lines, and that the AAMA standard compliance of those systems drove broader adoption (NCCA, 2015). Technical shifts in chemistry facilitate these operational changes.
Environmental Benefits: Removing Hexavalent Chromium from the Wastewater Train
Chromate-bearing rinse waters contain hexavalent chromium, a pollutant of concern for water sources and ecosystems (Qualicoat UK & Ireland). The NCCA describes how the historical chromating sequence generated large volumes of chromate wastewater that required dedicated treatment to meet tightening EPA and OSHA limits throughout the late twentieth century, driving the search for non-chrome alternatives (NCCA, 2015). For a pretreatment engineer, hexavalent chromium is not just a PPE story; it is a unit process with its own tanks, dosing skids, and sludge line.
The treatment workflow for chrome-bearing waste is well documented and operationally heavy. Qualicoat UK & Ireland describes it as a two-stage process: first, pH and ORP adjustment to reduce hexavalent chromium to trivalent, visible as a colour shift from yellow to blue/green; then precipitation after a second pH adjustment, often aided by anionic or cationic polymer coagulants/flocculants, followed by mechanical filtration (Qualicoat UK & Ireland). The filtered effluent can be discharged if it meets limits, and the solid waste is managed under hazardous-waste rules. That entire reduction-precipitation-filtration train, plus its polymer dosing and sludge handling, exists solely because hexavalent chromium is in the bath.
By contrast, chrome-free pretreatment relies on benign chemistries such as zirconium, titanium, or silane-based solutions, eliminating toxic byproducts and reducing hazardous waste volume (Qualicoat UK & Ireland). The downstream effect on a plant's wastewater train is concrete: the reduction tanks, the SO₂ or ferrous-sulfate reduction chemistry, and the chrome-specific precipitation step can be decommissioned, and the rinse waters route directly to the general metal-finishing wastewater system. Less chrome-laden sludge also means smaller dewatering equipment, lower polymer consumption, and lower disposal cost, which is where a piece of equipment like a plate and frame filter press for sludge dewatering becomes relevant to the operating case for switching.
Worker Safety and Occupational Health Gains
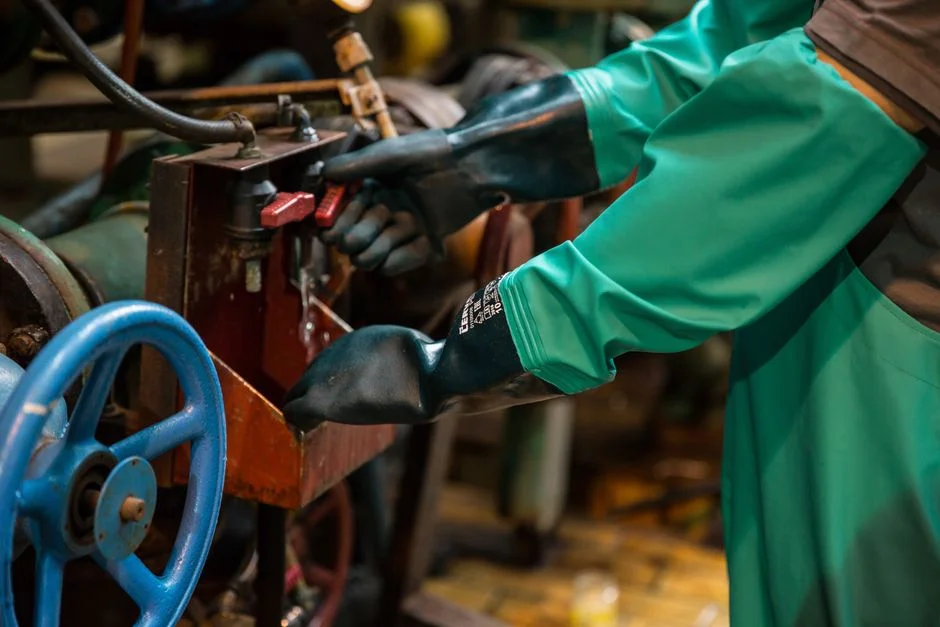
Exposure to hexavalent chromium is associated with respiratory issues, skin irritation, and an increased risk of cancer (Qualicoat UK & Ireland). For an EHS manager evaluating a chemistry switch, those three endpoints drive most of the regulated programme: medical surveillance, exposure monitoring, designated regulated areas, and the carcinogen-specific provisions of the OSHA hexavalent chromium standard. Removing the source chemical removes the regulatory trigger for the most expensive layers of that programme.
Chrome-6-free systems use safer chemicals that do not carry the same health threats, mitigating these risks (Qualicoat UK & Ireland). In practice, that allows the facility to right-size the PPE specification at the pretreatment line. Respirator fit-testing, hexavalent-chromium-specific gloves and coveralls, and dedicated exhaust ventilation can be relaxed or removed, with the result that the EHS burden drops on a per-line basis. Qualicoat UK & Ireland explicitly links this shift to a reduction in the need for extensive PPE and complex ventilation systems, creating a safer and more cost-effective working environment.
The downstream benefits accumulate even where they are not purchased as a chemistry line item: medical surveillance frequency tied to a regulated carcinogen, the training and recordkeeping burden for hexavalent-chromium-exposed tasks, and the incident-response capability maintained for a known carcinogen. Each becomes eligible for review and reduction once the source chemical is gone.
Regulatory and Market Compliance Benefits
Policies such as the EU's REACH regulation impose significant restrictions on hexavalent chromium, and compliance is mandatory for manufacturers operating in global markets (Qualicoat UK & Ireland). For a fabricator shipping architectural aluminium into the EU, the practical move is to specify QUALICOAT-grade chrome-free pretreatment in procurement documents so that compliance is locked in at the coating supplier rather than re-checked on every shipment (Qualicoat UK & Ireland). Qualicoat UK & Ireland recommends requesting the involvement of a specialist coater at the early design stages of any project located in harsher environments, such as near to coastal waters.
For U.S. metal finishers and fabricated-metals plants, the same trend feeds EPA categorical pretreatment standards and the buyer audit checklists used by large OEM customers. A plant that documents its switch to chrome-free pretreatment in its environmental management system has a cleaner story for any third-party audit, including an ISO 14001 surveillance review. A useful starting point is a fabricated metals pretreatment compliance guide that frames the same shift in the regional regulatory context.
Reaching equivalence with REACH also simplifies access for products shipped into the EU, and many non-EU jurisdictions are tightening parallel rules. The strategic value of the switch is staying legal while removing a recurring regulatory retrofit from the five-year capex plan.
Operational and Performance Benefits: Coating Mass, Energy, and Corrosion Resistance
Modern chrome-free systems are engineered to match or exceed traditional chromate-based processes for corrosion resistance and paint adhesion (Qualicoat UK & Ireland). The NCCA confirms this on the coil side, reporting that chrome-free pretreatments were demonstrated to meet AAMA standards by the year 2000 and that the chrome-free conversion to titanium-based non-chrome dry-in-place treatments was completed with good results on aluminium coil coating lines (NCCA, 2015). For a production engineer, the performance gate is passed at the substrate and paint-system level.
The biggest operating envelope change is coating mass. NCCA industry data shows chrome-free pretreatments on aluminium coil typically run at 6–12 mg/ft², compared to 60–120 mg/ft² for chromate phosphate coatings, an order of magnitude reduction in coating mass (NCCA, 2015). The chemistry that delivers that reduction is also different: NCCA reports that the new chrome-free treatments typically replaced the chromate chemicals (which included phosphoric and hydrofluoric acid) with fluocomplexes of zirconium and titanium with specialty polymers (NCCA, 2015). Less coating mass, less drag-out, and a different acid system all flow through to the wastewater train.
Many chrome-free formulations operate at lower bath temperatures, which reduces energy consumption and operational cost, and they generate less sludge and waste, which cuts maintenance and disposal expense (Qualicoat UK & Ireland). The combination of lower coating mass, lower bath temperature, and reduced sludge volume is what makes the operating case quantitative, even when the specific energy and chemical savings depend on the line being modified.
Chemistry Comparison: Zirconium, Titanium, Silane, and Polymer Blends
For a pretreatment engineer choosing between chrome-6-free families, the right framing is substrate, line geometry, and downstream wastewater impact. The NCCA's summary of the available chemistries, which the table below organises, provides a defensible reference point (NCCA, 2015).
| Chemistry family | Typical substrate and line | Process notes | Wastewater impact to verify |
|---|---|---|---|
| Zirconium-based fluocomplexes | Aluminium extrusion; many general metal finishing lines | Tolerates short contact times; widespread in the post-2000 conversion (NCCA, 2015) | Fluoride and zirconium load in rinse water; check clarifier performance and sludge solids |
| Titanium-based with polymer additives | Aluminium coil lines; dried-in-place applications | Aggressive to mild steel; trays, pick-up rolls, and processing equipment must be acid-resistant (NCCA, 2015) | Low pH excursions; fluoride and titanium carryover; rinse pH profile |
| Silane-based and novel polymer systems | Active R&D across all substrates | No single set of industry standards yet established (NCCA, 2015) | Organic load in rinse; potential for foaming in DAF; verify with jar tests |
Chemistry choice drives three wastewater parameters that the downstream equipment has to handle: rinse-water pH, fluoride concentration, and sludge volume. A line moving to zirconium fluocomplexes will see a different fluoride loading profile than a line moving to titanium with polymer additives, and that in turn determines whether a dissolved air flotation system, a lamella clarifier for sludge recirculation, or a PLC-controlled chemical dosing skid is the right unit operation to specify. Where detailed DAF sizing is needed, the DAF design parameters guide is a useful companion reference.
What to Verify in Your Plant Before Switching
Confirm substrate compatibility: chrome-free systems that meet AAMA standards on aluminium are documented (NCCA, 2015), but the team should validate on the specific alloy mix used in the plant. Different alloying elements change both the surface chemistry and the XRF blank, so a single test panel is not enough; pull representative lots from each alloy in production.
Audit the wastewater train before the bath change. Identify where hexavalent chromium reduction and precipitation equipment can be decommissioned, where chrome-free rinse chemistry interacts with existing DAF or clarifier performance, and where a multi-media filter for rinse-water polishing might be added to protect downstream reverse-osmosis or ion-exchange polishing steps. The goal is to make sure the new chemistry does not push existing equipment outside its design window.
Review bath temperature, contact time, and coating-weight measurement. NCCA notes that XRF measurement of chrome-free pretreatments is challenging because coating masses are very low and the measured elements overlap with alloying elements in the substrate, so careful blank measurements and subtraction of this blank is necessary (NCCA, 2015). Operator training, PPE, and ventilation requirements for the new chemistry also need to be updated, and SOPs and emergency response plans revised to reflect the new bath chemistry.
Frequently Asked Questions
What is the realistic cost impact of switching from chromate to a chrome-6-free pretreatment line?
Qualicoat UK & Ireland frames the operating savings in qualitative terms: lower energy consumption from reduced bath temperatures, lower polymer consumption from less sludge, and lower disposal expense from less hazardous waste (Qualicoat UK & Ireland). NCCA's 2015 data point that chrome-free pretreatments run at roughly 6–12 mg/ft² versus 60–120 mg/ft² for chromate phosphate (about an order of magnitude less coating mass) is the main quantitative lever (NCCA, 2015). A buyer should request line-specific quotes for chemistry, energy, sludge hauling, and PPE/ventilation from at least two qualified suppliers before approving the project, since the savings depend heavily on local utility rates, hauling rates, and labour.
How do I choose a chrome-6-free chemistry supplier and what compliance evidence should I ask for?
For aluminium architectural supply into the EU,
Frequently Asked Questions
What are the main benefits of switching from chrome 6 to chrome-free pretreatment in an industrial plant?
The primary benefit is the elimination of hexavalent chromium, a known human carcinogen, which significantly reduces regulatory compliance burdens under OSHA and REACH standards. By removing hazardous waste streams, plants eliminate the need for costly hexavalent chromium reduction processes and minimize long-term environmental liability.
Operational efficiency increases due to simplified maintenance and reduced water consumption. Chrome-free chemistries typically operate at lower temperatures, often between 20°C and 40°C, leading to substantial energy savings compared to traditional chromate conversion coatings that require more intensive process control.
Does chrome-free pretreatment perform as well as chromate for corrosion resistance on aluminium?
Modern chrome-free conversion coatings, particularly those based on zirconium and titanium, now meet or exceed the performance requirements of MIL-DTL-81706 and MIL-DTL-5541 specifications. In standardized salt spray testing (ASTM B117), high-performance chrome-free systems consistently provide over 1,000 hours of protection on 2024-T3 and 6061-T6 aluminum alloys.
While chromate coatings offer self-healing properties that chrome-free alternatives lack, the barrier protection provided by advanced metal oxides is superior in multi-metal applications. When paired with high-quality powder or liquid topcoats, chrome-free systems provide adhesion and corrosion resistance parity for virtually all commercial and industrial exterior applications.
How does a chrome-6-free line change the wastewater treatment system I need to design?
Removing hexavalent chromium eliminates the requirement for a dedicated reduction stage where pH must be lowered to 2.0–2.5 for the chemical reduction of Cr(VI) to Cr(III) using sodium metabisulfite. This removes the risk of toxic chromium sludge generation, which is classified as hazardous waste, thereby simplifying the dewatering and disposal process.
Wastewater treatment systems for chrome-free lines are generally smaller and less complex, focusing primarily on pH neutralization and the precipitation of fluorides or transition metals like zirconium. This shift often allows for direct discharge or easier water recycling, significantly reducing the chemical consumption and operational costs of the effluent treatment plant.
What is the typical payback period or cost saving from removing hexavalent chromium from a pretreatment line?
The payback period for transitioning to a chrome-free line typically ranges from 12 to 24 months, depending on the volume of hazardous waste formerly generated. Significant savings are realized through the elimination of hazardous waste disposal fees, which can account for 20% to 40% of total pretreatment operating costs in facilities with high throughput.
Additional savings are accrued through reduced PPE requirements, lower insurance premiums related to hazardous materials handling, and the elimination of mandatory air monitoring and medical surveillance programs required for workers exposed to hexavalent chromium. Process energy savings can further reduce the total cost of ownership by an additional 5% to 10% annually.
Which chemistry — zirconium, titanium, or silane — is best for high-volume metal finishing operations?
Zirconium-based chemistries are currently the industry standard for high-volume metal finishing due to their robustness, ease of control, and multi-metal compatibility. They provide a dense, uniform conversion coating that performs exceptionally well as a base for powder coating, offering excellent adhesion and corrosion resistance across steel, galvanized steel, and aluminum.
While titanium chemistries are cost-effective, they are often more sensitive to pH fluctuations, and silane-based chemistries, while providing excellent adhesion, may lack the long-term corrosion resistance required for exterior-grade products. For high-volume lines requiring consistent quality across diverse substrates, zirconium-based thin-film technologies offer the best balance of performance and process stability.