Why a Delhi Food or Beverage Plant Lives by an NOV, Not an EPA Inspection
For a Delhi food processor receiving a notice, verify its actual issuer, violated conditions, sampling result and deadline. A universal 30–60 day compliance-plan window or one specific local authority cannot be inferred from a food-industry label. Record the real sewer control mechanism and agreed corrective milestones.
The enforcement escalator is steep and worth naming explicitly. A first violation is typically a notice plus a civil penalty that can run from hundreds to tens of thousands of dollars per parameter per day of discharge (per 40 CFR 403.8 enforcement authorities). Repeated violations add administrative surcharges, increase monitoring frequency to monthly or even continuous, and can require the plant to post a performance bond. Permit revocation halts production — the discharge permit is the legal authority to send anything to the sewer, and pulling it shuts the line. The engineer who sizes to the average discharge is the engineer who eventually meets the worst-case arm of that escalator.
The Four Rule Layers a 2026 NOV Will Cite
For Delhi food wastewater, Part 403 provides the general industrial-sewer pretreatment framework. Part 432 is Meat and Poultry Products for specified direct discharges, not five dairy, grain, fruit/vegetable and beverage sewer subparts. EPA withdrew proposed new meat/poultry pretreatment standards in 2025. Establish actual process coverage and the receiving authority’s conditions before extracting limits.
Confirm whether each Louisiana outfall is direct under its authorization or indirect to a POTW, and obtain the actual permit, ordinance and control mechanism. A local authority cannot waive an applicable federal pretreatment standard, but direct effluent tables must not be applied as sewer limits automatically. Follow the dates and obligations in the real notice.
An applicable federal pretreatment standard and 403 prohibition remain independently enforceable alongside actual local conditions. Establish process coverage and the sewer route first. There is no evidence here that invented 432 dairy/beverage ceilings cause most Delhi notices, or that an industry table replaces the actual authority’s requirements.
Match the Delhi process and discharge route to the actual category
Review 405 for dairy,406 grain milling,407 preserved fruit/vegetables and 408 seafood according to their actual scope. 432 covers meat/poultry, not these other products. Identify processes and source status rather than treating an SIC/NAICS code as sufficient proof of a numeric standard.
The following matrix identifies the verified documents and acceptance basis needed for a Delhi sewer project. It replaces the mistaken comparison between a generic local range and a supposed 432 meat/dairy sewer ceiling.
| Parameter | Requirement to obtain | Acceptance record |
|---|---|---|
| BOD₅ /TSS /FOG /nutrients | Actual applicable limit from the actual Delhi receiving authority, units and period; not a universal 432 food sewer value | Representative load profile, sample method and measured inlet/outlet |
| pH | Actual local range plus 403.5(b)(2): corrosive structural damage and below 5.0 unless POTW designed for it | Calibrated measurement at specified point; no universal 403 range 6–9 |
| Heat | 403.5(b)(5): interference prohibition; 40°C at POTW treatment plant unless approved alternative | Confirm plant-point basis and any stricter local condition |
For oil and grease, record the actual applicable limit, method, sampling point and period. A poultry deboning line does not automatically inherit a direct 432 concentration at its sewer connection. Separate any high-strength tariff from a concentration or mass restriction; payment does not authorize a prohibited discharge.
Splitting the Flow Into Four Characteristically Different Streams
Engineers who treat "food and beverage wastewater" as a single stream consistently oversize or undersize unit operations; the first design step is splitting the flow into four characteristically different streams and assigning each to the right piece of equipment.
Process water from washing, cooking, cooling, and packaging carries the bulk of the BOD and suspended solids load — high organic strength, often 1,500–5,000 mg/L BOD₅ for a mid-size further-processing line — and it is the stream that sets the size of the equalization basin and the downstream biological stage. CIP caustic and acid rinses drive pH swings that are the dominant reason equalization is non-negotiable: a fruit wash can leave the line at pH 3.5, the next CIP cycle can exit at pH 12, and any treatment program built around averages will fail at those moments. Cooling-water blowdown is generally lower in organics but can carry lubricants, trace metals, and heat; it is normally segregated and either discharged under a separate non-contact permit or screened and recombined upstream of biological treatment. Sanitation and floor wash is where the FOG load concentrates, and it is the stream a DAF unit is sized to capture before the load ever reaches the aeration basin.
Routing matters as much as characterization. For a Delhi-area line the typical routing puts floor-wash and sanitation flow to the DAF, process and CIP flow into equalization, non-contact cooling blowdown around biological treatment when segregable, and only the polished DAF plus biological effluent going to pH trim and discharge.
The 2026 Five-Stage Treatment Train and Where Each Sub-Sector Overloads It
The defensible 2026 train for a Delhi food or beverage plant follows a five-stage sequence: (1) screening and equalization, (2) primary solids removal via a dissolved air flotation system or lamella clarifier, (3) biological treatment (MBR, MBBR, or activated sludge), (4) pH trim and disinfection, and (5) sludge dewatering with a plate-and-frame filter press. Each performance metric in that sequence is justified to the local authority during the NOV response, and the metric is sized to the strictest number in the four-layer stack rather than the federal minimum.
Product and cleaning profiles place different loads on the treatment stages; identify the bottleneck from measured water rather than 432 subpart labels. Meat and poultry plants carry the highest FOG load — often 800–2,000 mg/L in the raw stream — and overload Stage 2 (the DAF). Dairy and cheese plants discharge protein-rich waste that overloads Stage 3 (the biological stage). Beverage, brewery, and confectionery lines produce sugar- and starch-dominated waste that spikes BOD within hours of a batch and overloads Stage 1 (equalization). Bakery, snack, and ready-meal plants carry high suspended solids from pulp, seeds, and grains that overload screening in Stage 1, and screen sizing for these solids-heavy lines is the difference between a clean Stage 2 and a flooded one.
The defensive posture in the NOV response is to map your sub-sector to the stage it overloads and show the local authority where you have added headroom. A poultry plant with FOG in the 800–2,000 mg/L range and a DAF sized only to the average load is the plant that signs a consent order; the same plant with a DAF sized to the 95th percentile feed condition is the one that gets the compliance plan accepted.
DAF vs Lamella Clarifier: The ~200 mg/L FOG Breakpoint
For the 10–100 m³/h envelope typical of mid-size Delhi-area food and beverage plants, the primary-solids decision comes down to dissolved air flotation or a lamella clarifier. Both technologies are well-proven, but they solve different problems and the operating-cost delta is significant.
| Criterion | DAF | Lamella Clarifier |
|---|---|---|
| Flow range | 4–300 m³/h across 13 standard models | 20–40 m³/m²/h surface loading |
| Best at removing | FOG, emulsified oils, colloidal TSS | Bulk TSS, settleable solids |
| Primary strength | Down to < 50 mg/L on conditioned feed | Up to 30% lower coagulant consumption vs. conventional clarifiers |
| Specify when | FOG or emulsified oils > ~200 mg/L, or line is poultry/meat/dairy | TSS-dominant influent with chemical-OPEX sensitivity |
| Watch-out | Chemical OPEX rises if FOG is over-driven | Cross-flow risk if influent FOG is not low |
The decision rule: specify DAF when FOG or emulsified oils exceed ~200 mg/L or when the line is poultry, meat, or dairy; specify a high-efficiency lamella clarifier when TSS is the dominant parameter and the plant's priority is minimizing coagulant and polymer OPEX. For most Delhi-area F&B lines the FOG load tilts the decision toward DAF, with a lamella more commonly used as a polish stage after biological treatment. Pair the primary stage with an automatic chemical dosing skid to keep coagulant demand from drifting upward as feed composition changes — chemical OPEX is the line item that erodes fastest when dosing is left on manual trim.
MBR vs Activated Sludge: Sizing the Biological Stage for 10–100 m³/h
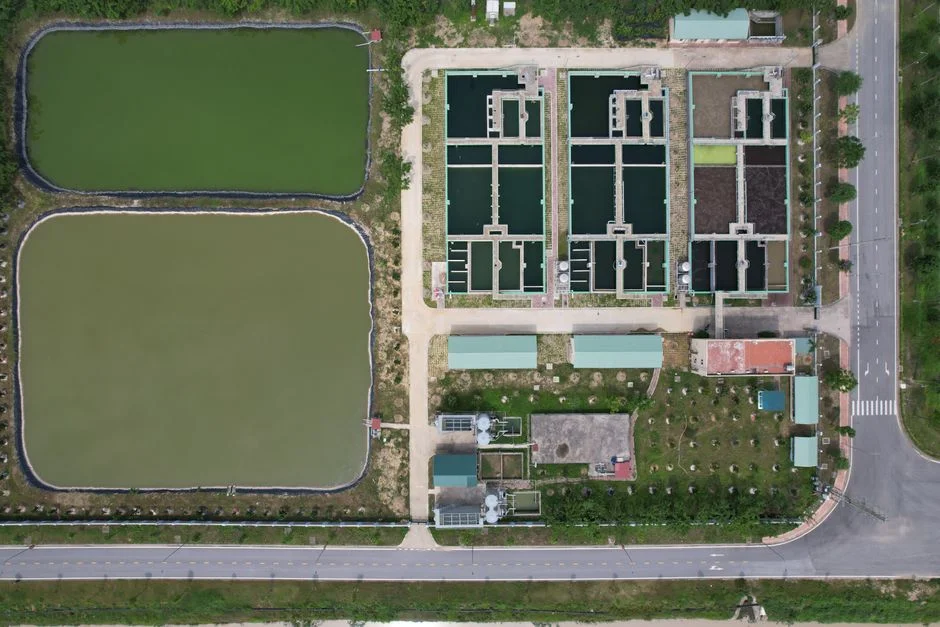
For the biological stage, compare CAS, MBBR or an MBR system using actual biodegradable load, inhibition, nutrient requirements and the verified outlet targets. A generic below 30 mg/L result is not proof of meeting a 26 mg/L target, nor evidence that 432 sets a dairy sewer limit. Require a guaranteed inlet envelope and representative performance testing.
Adding an MBR biological stage to a packaged DAF brings installed cost to roughly 1.4–1.8× the DAF cost for a complete system (HydropureWater field data, 2026). The MBR premium is justified when the categorical ceiling is the binding constraint rather than the local POTW limit. DF series PVDF flat sheet membrane modules at 0.1 μm pore size, individually replaceable elements, 10–20× lower energy consumption than external cross-flow systems, available in 80–225 m² configurations, are the workhorse component. Conventional activated sludge still wins on CAPEX for plants with a local POTW BOD ceiling of 250+ mg/L and no categorical binding constraint, and an MBBR is the middle path for plants that need nitrification but cannot justify the MBR footprint. A full MBR vs conventional activated sludge trade-off is laid out in the East Saint Louis chemicals comparison.
Sludge Dewatering and the NOV Response Sequence
OPEX is dominated by three line items: polymer and coagulant (which is exactly why the lamella's 30% chemical reduction is operationally meaningful), sludge-hauling cost per wet ton at Louisiana rates, and aeration power for the MBR or activated-sludge basin. A plate-and-frame filter press dewatering the DAF float and waste activated sludge in Stage 5 typically reaches 20–25% cake solids, cutting disposal volume 75–80% versus lagooned float and usually paying back the press inside 18–30 months at Louisiana hauling rates.
The corrective sequence is to verify the actual category and route, compile the applicable limit/method/period matrix, characterize production and cleaning batches, test oil/solids separation and biological needs, then agree the temporary and permanent milestones with the authority. Specify sludge handling and monitoring from actual duties. A reference installation does not prove a universal 10-day delivery or 8–16 week build.
Frequently Asked Questions
How does a Delhi food plant establish its applicable category?
Identify actual dairy, grain, preserved-produce, seafood or meat/poultry operations; review 405/406/407/408/432 as applicable and their direct/indirect provisions. Obtain the receiving authority’s actual control mechanism. Do not search for an invented 432.21–30 dairy or 432.71–80 beverage sewer category.
What is the decision rule for DAF versus a lamella clarifier in a Delhi F&B plant?
Specify DAF when FOG or emulsified oils exceed ~200 mg/L or when the line is poultry, meat, or dairy. Specify a lamella clarifier when TSS is dominant and the plant's priority is minimizing coagulant and polymer OPEX — lamellas cut coagulant consumption up to 30% versus conventional clarifiers.
When is an MBR justified over conventional activated sludge for a 10–100 m³/h Delhi F&B line?
Choose MBR when tests and lifecycle evaluation support its role against the actual targets. Neither a supposed 432 meat/dairy sewer ceiling nor a general below 30 mg/L BOD claim demonstrates compliance. Check the specific limit, averaging period, temperature and feed envelope in the acceptance test.
What is the typical NOV response window for a Delhi food or beverage plant in 2026?
The notice and control mechanism determine the response and reporting dates. Agree the interim and permanent scope, approvals and delivery schedule with the actual authority and suppliers. Do not assume 30–60 days, automatic 10-day temporary treatment or a universal 8–16 week build.