Which Rules Apply to a Canfield Fabricated Metals Plant
Federal regulation 40 CFR Part 433, the Metal Finishing point source category, sets categorical pretreatment standards for any facility that performs forming, finishing, forging, foundry, metal spraying, or machining wash co-located with plating or anodizing lines. A stamping shop that ships only dry parts to a separate finisher is generally outside the category; a facility that runs its own zinc, nickel, or chromic acid tank is inside it (per 40 CFR Part 433, 2026). The rule splits limits into PSES (Pretreatment Standards for Existing Sources) and PSNS (Pretreatment Standards for New Sources), with PSNS tighter because it applies to sources constructed after the rule's promulgation date. Most POTW pretreatment programs enforce PSNS-equivalent local limits on all industrial users as a conservative baseline, so even an existing plant should usually design to PSNS numbers.
Layered on top of Part 433 is the 40 CFR 403.5 local-limits framework, which requires every POTW to develop pollutant-specific caps that prevent pass-through and interference at the receiving plant (per EPA, 2026). Local limits are at least as stringent as the categorical standards, and in practice they add the parameters the federal rule underweights: copper, nickel, zinc, lead, silver, oil and grease, TSS, and pH. Ohio EPA holds delegated authority to layer additional requirements on top of federal categorical standards, and a Canfield-area discharger into the Mahoning County/Youngstown POTW system must satisfy that local sewer ordinance as well. The plant must meet whichever limit is stricter on each parameter, which is why the design envelope is built from the POTW table, not from the federal table alone.
| Regulatory layer | Codified at | What it caps | Stringency vs. Part 433 |
|---|---|---|---|
| Federal categorical — PSES | 40 CFR Part 433 | Cd, Cr, Cu, Pb, Ni, Ag, Zn, TTO | Baseline for existing sources |
| Federal categorical — PSNS | 40 CFR Part 433 | Cd, Cr, Cu, Pb, Ni, Ag, Zn, TTO | Tighter; new sources post-promulgation |
| Federal local-limits framework | 40 CFR 403.5(c) | Pass-through and interference pollutants | At least as stringent as categorical |
| Ohio EPA / Mahoning County POTW ordinance | Ohio Administrative Code + local sewer use ordinance | Adds O&G, TSS, pH, plus site-specific metals | Frequently stricter than federal |
The Four Contaminant Families Coming Off a Fabricated Metals Floor
Most fabricated metals floors generate the same four contaminant families regardless of the specific process mix, and the 2026 design must handle all of them in series rather than collapsing them into one reaction stage. Free and emulsified oils come from stamping, machining, and drawing compounds and typically run 50–500 mg/L on the mixed floor drain (HydropureWater field data, 2026). Dissolved heavy metals — zinc, nickel, copper, chromium, lead, cadmium — arrive in plating rinsewater and acid pickling waste at 5–200 mg/L and will not drop out of solution without an explicit pH-driven precipitation step. Hexavalent chromium from chromic acid anodizing, hard chrome plating, and conversion coating is the single most aggressive parameter; a hard chrome line can spike Cr(VI) to 50+ mg/L and drop pH below 2 on a rinse dump.
Total suspended solids from grinding swarf, casting sand, and hydroxide floc carryover run 100–1,000 mg/L and foul clarifiers and DAF units when not addressed at the head of the train. Cyanide appears wherever alkaline cyanide plating (Zn, Cu, Cd, Ag) is still in operation, and it must be oxidized before metals precipitation or it resolubilizes the precipitates downstream. pH swings from 2 to 12 across batch dumps make equalization mandatory, not optional, because a downstream pH probe that is simultaneously chasing acid and caustic spikes cannot hold the 8.5–9.5 precipitation setpoint reliably. The four families do not all respond to the same chemistry: oils need physical separation or chemical break, hex chrome needs reduction, cyanide needs oxidation, and dissolved metals need pH-driven precipitation, which is why the unit operations must be ordered correctly.
The Engineered Treatment Train for 2026 Compliance
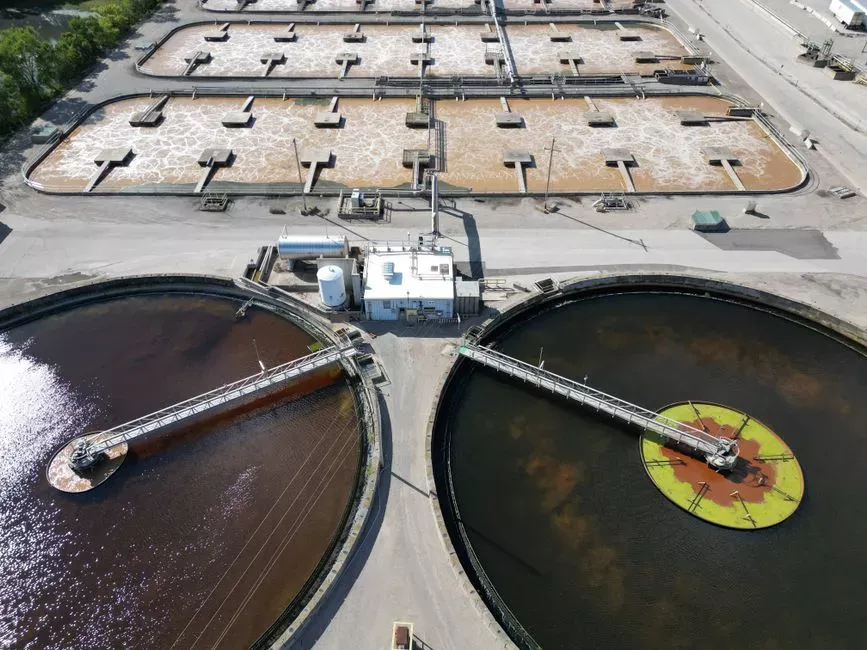
The standard 2026 train for a Canfield-area fabricated metals plant runs equalization → oil and grease removal → hexavalent chrome reduction → cyanide oxidation (where applicable) → hydroxide precipitation → DAF or lamella clarification → pH trim. A rotary mechanical bar screen for rags and tramp metal removal sits upstream of equalization to keep wipes and stringy debris out of the sludge train, which is the single most common cause of premature press-cloth failure downstream. Equalization smooths pH into a 6–9 band and drops the flow coefficient of variation below 0.5; sample a full-week composite before sizing the basin, because a 4-hour composite that misses the Friday afternoon dump will undersize the equalization basin (HydropureWater field data, 2026).
Step 2 is oil and grease removal via a dissolved air flotation system for oil and metal-hydroxide separation or a lamella plate ahead of chemistry. DAF is governed by three knobs: hydraulic surface loading of 4–20 m/h depending on model and floc density, an air-to-solids ratio of 0.005–0.060 with 0.02 a typical design point, and a recycle rate of 10–30% of forward flow. Pushing A/S higher produces a drier float but costs blower power and can shatter fragile floc; pushing recycle rate higher improves TSS removal but dilutes the chemistry and inflates equalization demand. Step 3 reduces hexavalent chrome with sodium metabisulfite (or ferrous sulfate) at pH 2–3, with ORP controlled at 250–300 mV. Step 4 oxidizes cyanide with NaOCl if alkaline cyanide plating is present, and this step must precede metals precipitation. Step 5 precipitates dissolved metals as Cr(OH)3, Zn(OH)2, Ni(OH)2, Cu(OH)2, Pb(OH)2, and Cd(OH)2 at pH 8.5–9.5. Step 6 floats the floc in a DAF or lamella clarifier; chemical feed is governed by a PLC-controlled chemical dosing skid for pH and ORP trim with feedforward (flow-paced) and feedback (pH/ORP) control. Step 7 trims pH to 6–9 and polishes residual TSS. Alarm and shutdown interlocks on pH excursion, ORP out of range, and high TSS should auto-divert flow back to the equalization basin header so a chemistry upset does not become a discharge violation. For a comparison of clarifier vs. DAF on mining and metals wastewater, see the analysis at DAF vs clarifier for mining and metals wastewater.
| Step | Unit operation | Operating envelope | Failure mode if skipped |
|---|---|---|---|
| 1 | Equalization | pH 6–9, flow CV < 0.5 | Downstream chemistry hunts setpoint |
| 2 | Oil/grease removal (DAF or lamella) | 4–20 m/h, A/S 0.02, recycle 10–30% | Oil bleed-through fouls precipitation |
| 3 | Hex chrome reduction (Na2S2O5 / FeSO4) | pH 2–3, ORP 250–300 mV | Cr(VI) passes through soluble |
| 4 | Cyanide oxidation (NaOCl) | pH > 10, ORP > 600 mV | CN resolubilizes metal precipitates |
| 5 | Hydroxide precipitation | pH 8.5–9.5 | Dissolved metals exceed PSNS caps |
| 6 | DAF or lamella clarification | Floc blanket, surface loading per step 2 | High TSS carryover to discharge |
| 7 | pH trim + TSS polish | pH 6–9, TSS < 30 mg/L | POTW violation, surcharge risk |
Parameter Table: Influent, Design Targets, and Effluent Envelope
The table below consolidates the design numbers a Canfield-area engineer should hand to a vendor or use to bench-check a proposal. The plant must meet whichever limit is stricter between 40 CFR Part 433 and the local Mahoning County POTW table, and the Cr(VI) and cyanide rows only apply when those processes are on site. Values marked "typical" reflect HydropureWater field data collected in 2026 from mixed floor drains at fabricated metals operations; values marked "PSNS-equivalent" track the Part 433 new-source daily-maximum caps and are the practical design target even for existing sources.
| Parameter | Raw wastewater, typical range | Design target (post-train) | PSNS-equivalent effluent cap |
|---|---|---|---|
| pH | 2–12 (batch dumps) | 6–9 | 6–9 (per 40 CFR 403.5) |
| Oil & grease | 50–500 mg/L | < 25 mg/L | Local POTW cap, often 50 mg/L |
| TSS | 100–1,000 mg/L | < 30 mg/L | Local POTW cap, often 30–50 mg/L |
| Total dissolved metals (sum) | 5–200 mg/L | < 2 mg/L | Per-metal PSNS, see below |
| Cadmium | 0.1–5 mg/L | < 0.05 mg/L | 0.11 mg/L (Part 433 PSNS) |
| Chromium (total) | 1–50+ mg/L | < 0.5 mg/L | 2.77 mg/L (Part 433 PSNS) |
| Copper | 1–50 mg/L | < 1 mg/L | 3.38 mg/L (Part 433 PSNS) |
| Lead | 0.5–20 mg/L | < 0.2 mg/L | 0.69 mg/L (Part 433 PSNS) |
| Nickel | 1–80 mg/L | < 1 mg/L | 3.98 mg/L (Part 433 PSNS) |
| Silver | 0.05–5 mg/L | < 0.1 mg/L | 0.43 mg/L (Part 433 PSNS) |
| Zinc | 5–100 mg/L | < 1 mg/L | 2.61 mg/L (Part 433 PSNS) |
| Cr(VI) (where applicable) | Up to 50+ mg/L | < 0.05 mg/L | 0.5 mg/L (typical POTW) |
| Cyanide (where applicable) | 1–50 mg/L | < 0.1 mg/L | 1.0 mg/L (typical POTW) |
| DAF float dry solids | — | 2–5% | n/a (internal to sludge train) |
Sludge Handling and the Plate-and-Frame Payback
Floated metal-hydroxide sludge typically runs 2–5% dry solids out of the DAF and dewateres to 25–35% with a plate and frame filter press for metal hydroxide sludge (HydropureWater field data, 2026). A belt press is cheaper and continuous but caps out around 22% dry solids on metal hydroxide, so if the hauler bills by wet ton, the plate and frame pays back the incremental capex within a measurable window. A rotary mechanical bar screen for rags and tramp metal removal upstream of the equalization basin keeps wipes, rags, and tramp metal out of the sludge train, which is the single most common cause of premature press-cloth failure in metal hydroxide service. Alarm and shutdown interlocks on pH excursion, ORP out of range, and high TSS should auto-divert flow back to the equalization basin header so a chemistry upset does not become both a discharge violation and a contaminated sludge batch. For polymer selection ahead of the DAF, the PAC dosing system working principle and selection guide covers feed-rate curves that also apply to flocculant selection. A similar lifecycle story for mining and metals plants is mapped in the parallel post on how mining and metals plants near Franklin, US meet 2026 pretreatment limits.
When Polishing Is Needed — and the 2026 PFAS Question
Most fabricated metals plants hit sewer limits with the train above and never need a polishing step. The cases that do are predictable: the receiving POTW tightens local limits below PSNS, the plant wants to reuse rinsewater and needs RO-quality feed, or a new rule forces a polish stage. For BOD/COD tightening or water reuse, a submerged PVDF MBR membrane bioreactor system delivers filtration below 1 μm and stable effluent that can be sent to cooling tower makeup or rinsewater reclaim. For sub-ppm TDS or specific metal caps such as nickel below 0.1 mg/L, an RO system is required, and the multi-media filter upstream must hold SDI15 below 3 or the RO membranes fail early.
On PFAS: EPA's 2026 PFAS rulemaking is scoped to chrome finishing facilities, and there is no current numerical PFAS limit for chrome finishers today (per EPA Metal Finishing Effluent Guidelines, 2026). The right 2026 move is to design the train so anion exchange or GAC can be bolted on later, not to install it now and pay to operate it ahead of any actual limit. Closed-loop ZLD is rarely economic for a fabricated metals plant unless water scarcity or a specific reuse case supports the capital. A skid-mounted automatic chemical dosing system with PLC feedforward/feedback is the integration point that lets any future polish skid drop into the existing control architecture without rewiring the wet end.
Canfield-Area Compliance Checklist for 2026
- Confirm whether the plant falls inside 40 CFR Part 433 — a stamping shop that ships only dry parts to a separate finisher is generally outside; an on-site zinc, nickel, or chromic acid tank pulls the facility inside the category.
- Pull the receiving Mahoning County/Youngstown-area POTW's current local-limits table; the design envelope is built from the POTW table, not the federal table alone, because local limits are at least as stringent as Part 433 (per 40 CFR 403.5).
- Sample a full week of composite flow before specifying the equalization basin — a 4-hour composite that misses the Friday afternoon dump will undersize the basin and overload the chemistry downstream.
- Verify automatic chemical dosing interlocks on pH and ORP, and confirm a calibration column and stroke-count totalizer on every pump; without those, the operator is dosing blind.
- Plan a future polish skid footprint and floor drain routing now, even if the polish skid is not installed in 2026 — it is far cheaper to pour the pad and stub the drain today than to retrofit during a future PFAS-driven compliance event.
Frequently Asked Questions
Does 40 CFR Part 433 apply to every fabricated metals plant near Canfield?
No. Part 433 covers forming, finishing, forging, foundry, metal spraying, and machining wash co-located with plating or anodizing lines. A stamping shop that ships only dry parts to a separate finisher is generally outside; a facility that runs its own zinc, nickel, or chromic acid tank is inside (per 40 CFR Part 433, 2026).
What is the difference between PSES and PSNS for a fabricated metals discharger?
PSES is the Pretreatment Standard for Existing Sources and PSNS is the tighter standard for New Sources built after the rule's promulgation date. Most POTWs enforce PSNS-equivalent local limits on all industrial users as a conservative baseline, so design to PSNS numbers unless the local POTW table is stricter (per 40 CFR Part 433).
How is hexavalent chromium removed before the metals precipitation step?
Hexavalent chrome is reduced to trivalent chrome using sodium metabisulfite or ferrous sulfate at pH 2–3 with ORP controlled at 250–300 mV. The trivalent form then precipitates as Cr(OH)3 in the pH 8.5–9.5 precipitation stage, where Cr(VI) hydroxide would otherwise remain soluble.
When does a fabricated metals plant need a polishing step beyond the standard train?
Polishing is needed when the Mahoning County POTW tightens local limits below PSNS, when the plant reuses process water, or when a future rule forces it. MBR handles BOD/COD tightening and water reuse, RO handles sub-ppm TDS or nickel below 0.1 mg/L, and anion exchange or GAC handles the PFAS rulemaking EPA has in motion for chrome finishing facilities in 2026.