Confirm direct discharge or sewer pretreatment in Chehalis
Determine the category from the mineral, actual operation and wastewater source before selecting a separator. Part437 is Centralized Waste Treatment: it covers specified treatment/recovery of wastes received from off-site, with subcategories for metals, oils, organics and multiple wastestreams, and exclusions. It is not an ore-mining category and does not automatically cover a mine treating its own wastewater. Part440 concerns covered ore mining/dressing; Part436 concerns covered mineral mining/processing, with several reserved subparts. Other operations can require different category assessments, including covered metal finishing under433.10. A reserved subpart does not establish that no other permit or numerical requirement applies.
| Discharge route | Design document to obtain | Key distinction |
|---|---|---|
| Surface-water discharge | Applicable NPDES authorization, process category/subcategory and site limits | Do not substitute a generic437 table or sewer limits. |
| Connection to a POTW | Actual receiving authority, applicable pretreatment category determination, local limits and control mechanism | 403.5 prohibitions apply to each user; not every POTW must operate an approved local programme under 403.8. |
| Process reuse | End-use quality specification, concentrate and residual destinations, any applicable authorization | A reuse specification is not a discharge permit. |
Compare only requirements that actually cover the same discharge, pollutant, units and statistical period. This article establishes no common local copper, zinc, lead or TSS limit for all plants in the area. Drinking-water lead action levels, an unverified rulemaking date and a city name cannot supply that missing sewer limit. Obtain the current written conditions before fixing a performance guarantee.
The Pollutant Profile That Drives the Rule Set in Lewis County
The influent that hits the equalization basin determines the rule set that controls the discharge. Raw acid mine drainage and spent process solutions routinely arrive at pH 2–4, with total suspended solids in the hundreds to several thousand mg/L and dissolved heavy metals (Pb, Cu, Zn, Cd, Ni, As) driving most of the local limit table. Elevated sulfate and total dissolved solids are typical of leach-pad runoff and brine streams; high-TDS streams push operators toward NaOH rather than lime because lime generates 3–5× more sludge at the same neutralization capacity, and that extra volume of metal-hydroxide solids shows up in the hauling bill before it shows up in the discharge monitoring report.
Lewis County does not host a large active hardrock mine, so the realistic CIU population in the City of Chehalis WWTP service area is aggregate washing (sand-and-gravel classification, fines recovery), co-located metal-fabrication shops (forming, stamping, machining, light plating), and food processors sharing the collection system. A combined aggregate-washer-plus-fabrication-shop discharger carries 200–1,500 mg/L TSS from aggregate fines, 50–500 mg/L oil/grease from machining wash, 5–200 mg/L total dissolved metals from plating rinsewater, and pH swings of 2 to 12 across batch dumps (HydropureWater field data, 2026). That is the design envelope to size the equalization basin against, not a hardrock-mill effluent profile.
Obtain the applicable federal and local requirements
Obtain the actual receiving authority’s written requirements. Compare only requirements covering this operation, discharge route, pollutant, units and averaging period. A city name or a general federal category does not establish a common local numeric ceiling, a tightening date or an automatic percentage below federal values.
Verify current authorizations before expansion
Obtain the actual receiving authority’s written requirements. Compare only requirements covering this operation, discharge route, pollutant, units and averaging period. A city name or a general federal category does not establish a common local numeric ceiling, a tightening date or an automatic percentage below federal values.
The Treatment Train, Stage by Stage
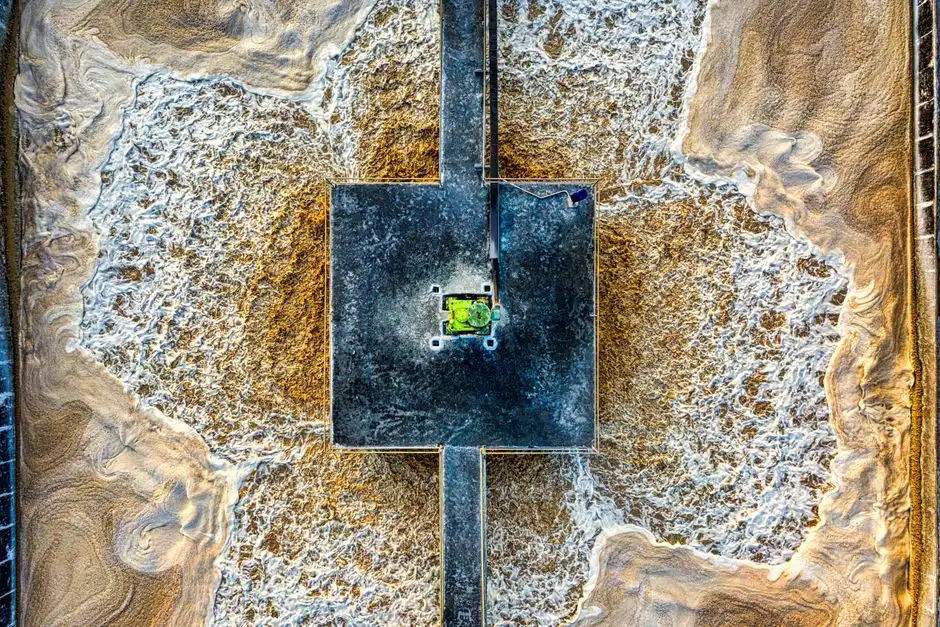
Stage 1 — Equalization. Spec the equalization basin at 8–24 hours of average daily flow; a 4-hour basin passes every batch discharge (shift change, dump-leach cycle, plating-tank dump) straight into the clarifier and overwhelms it. Target a flow coefficient of variation below 0.5 at the head of the plant. A rotary mechanical bar screen ahead of the basin keeps rags, wipes, and tramp metal out of the sludge train — the single most common cause of premature press-cloth failure downstream.
Stage 2 — pH correction. NaOH or lime to pH 6.5–9.0. Each 1 pH unit away from the metals-precipitation optimum can cut removal efficiency by an order of magnitude, sending zinc from <1 mg/L to 10+ mg/L with no other change to the chemistry. High-TDS streams justify the higher reagent cost of NaOH over lime because lime generates 3–5× more sludge at the same neutralization capacity. Stage the dosing across two reactors if the influent swings more than 2 pH units across batch dumps.
Stage 3 — Automatic chemical dosing. A PLC-controlled automatic chemical dosing skid that handles pH adjustment, coagulant, and polymer feed on a single panel keeps pH inside a ±0.2 band — the difference between meeting and missing a 0.3 mg/L zinc monthly average. Skid-mounting cuts field install time and forces the integrator to bench-test the interlocks before shipment.
Stage 4 — Precipitation. Hydroxide is the default, routinely achieving 85–95% total metals removal (per Fluence, 2024-11). Sulfide (NaHS, FeS, Na₂S) is reserved for streams where residual metal must drop below 0.1 mg/L: sulfide residuals are typically 0.01–0.05 mg/L for Cu, Zn, Cd, and Ni, an order of magnitude lower than hydroxide. Reagent cost runs 2–4× higher and the system requires sealed reactors with H₂S scrubbing on the vent. A polymer coagulant aid dosed at 0.5–3 mg/L flocs the metal-hydroxide particles fast enough for the clarifier to operate at 20–40 m/h hydraulic loading without carryover.
Stage 5 — Solid–liquid separation. Dissolved air flotation system covers 4–300 m³/h across 13 models at 5–25 m/h hydraulic loading, 90–98% TSS removal, and 85–95% oil/grease removal in mining/metal-finishing service. A HydropureWater lamella clarifier operates at 20–40 m/h surface loading in roughly one-third the footprint of a conventional clarifier, with lower chemical consumption because the sludge blanket is denser, but it does not remove free oil or colloidal fines as effectively as DAF.
Stage 6 — Multimedia polish. A multimedia filter (anthracite over sand over garnet) at 1–2 m/h filtration rate strips residual TSS to <10 mg/L and provides a buffer for the days the clarifier underperforms because of a polymer mis-dose or a hydraulic surge. Size the unit for the backwash cycle, not the average forward flow.
Stage 7 — Disinfection. UV or chlorine dioxide at 1–5 mg/L when the POTW ordinance requires a residual. Chlorine dioxide avoids the regulated trihalomethanes that chlorine produces.
Stage 8 — Sludge dewatering. A plate and frame filter press dewateres metal-hydroxide sludge to 25–35% dry solids, producing a stackable cake that can be hauled to a Subtitle-D landfill or sent to a smelter for recoverable metals. A belt press is cheaper and continuous but caps at ~22% dry solids on metal hydroxide — if the hauler is paying by wet ton, plate and frame pays back.
DAF vs Lamella — The Chehalis Decision Matrix
Use the heuristic: DAF when the stream carries oil, grease, or colloidal metals; lamella when the stream is primarily metal-hydroxide sludge at high flow and the footprint is constrained. For a Chehalis aggregate washer with a co-located metal-fabrication shop, the realistic answer is a single DAF (oil/grease from machining wash, colloidal fines from grinding) followed by a lamella on the metal-precipitation slipstream — a hybrid configuration that the Kelso mining DAF vs clarifier decision guide walks through in detail.
Frequently asked questions
Does Part437 establish a universal mining discharge table?
No. It is a CWT category with specified off-site-waste coverage and exclusions. Determine the actual mine, processing, metal-finishing or waste-treatment category and the discharge route before selecting any table.
Does compliance require DAF followed by a clarifier?
The category name does not establish a mandatory separator sequence. Compare settling and flotation on representative conditioned wastewater. Measure residual suspended and dissolved pollutants, chemical use, sludge and energy; a dissolved-metal problem may require precipitation or another treatment before solids separation.
What must a supplier prove before equipment acceptance?
Provide actual written requirements and measured feed variability. Require an agreed mass balance, throughput and residual-pollutant tests, consumables, residual handling and safe upset response. Equalization moderates load variations; it does not remove pollutant mass or authorize dilution instead of treatment.