Start With the Chemical Wastewater, Not the Equipment
Greensboro chemical factories should choose DAF when oil, grease, colloids, precipitated solids or floatable contaminants require effective separation, especially when downstream biological treatment needs a protected, low-solids stream. Choose a conventional clarifier when wastewater is predominantly settleable solids and the plant values a simpler gravity-separation system. No single option fits every chemical stream: characterize flow, pH, TSS, O&G, COD, metals and settling behavior, then pilot-test the selected train. S1 reports over 99% TSS and O&G removal across various industrial applications, but this is not a guaranteed chemical-wastewater result.
Begin by segregating each discharge stream and recording flow, TSS, O&G, COD, pH, metals, conductivity, temperature, settleable solids and every chemical addition. Soluble product loss, suspended raw materials, oily waste, precipitation floc and biological solids are different separation problems. S1 identifies high-O&G, metal-bearing and biological-solids applications as distinct DAF use cases, so combining them into one untreated “chemical wastewater” stream can obscure the required treatment mechanism.
Characterization should be event-based rather than a single grab sample. Include routine production, cleaning, dumping and upset periods. Variable batches and changing chemical feeds belong in the sizing basis because they affect equalization, conditioning dose, hydraulic loading and float or sludge handling. A poultry-processing study illustrates why sampling discipline matters: S5, published in 2012 by the American Society of Agricultural and Biological Engineers, reports mean raw COD of 5,263 mg/L and mean total solids of 3,355 mg/L. Those poultry values describe that study only and must not be applied to a Greensboro chemical plant.
| Input | Why it affects equipment selection | Evidence required before quotation |
|---|---|---|
| Flow regime | Sets hydraulic and equalization requirements. | Average, peak, batch-dump, minimum and permitted discharge flows. |
| Solids and oil | Distinguishes settleable solids from floatable and colloidal material. | TSS, settleable TSS, O&G and settleability observations across production conditions. |
| Chemical condition | Determines whether precipitation, coagulation or flocculation must precede separation. | pH range, metals, COD, alkalinity and proposed chemical additions. |
| Batch variability | Changes feed concentration, dose and hydraulic shock. | Event records and representative samples from routine, cleaning and upset periods. |
If treatment depends on precise chemical dosing, define the feed system with the PLC-controlled chemical dosing system in the design package. For plant-wide limits, compare the required outlet with the approach in organic chemical plant pretreatment limits, then confirm the applicable Greensboro permit conditions rather than assuming another facility’s limits apply.
How DAF and Conventional Clarifiers Separate Wastewater
Dissolved air flotation separates floatable material by attaching fine bubbles to particles or droplets and carrying them to the surface for skimming; a conventional clarifier separates settleable solids through gravity and sludge withdrawal. The choice therefore depends on whether the target material sinks, floats, or must first be conditioned into either fraction.
A typical DAF train consists of equalization where needed, chemical conditioning or flocculation, saturation and recycle, flotation, and automatic skimming. Pressurized recycle water dissolves air, and the resulting fine bubbles attach to floc or floatable material. This makes DAF relevant where free oil, emulsions, light precipitates or colloids dominate the removal problem. The industrial dissolved air flotation system should therefore be evaluated on whitewater performance, chemical conditioning and float handling—not just tank surface area.
A conventional clarifier normally receives equalization where needed, optional coagulation and flocculation, a settling zone, sludge withdrawal and clarified-effluent collection. It is most credible where solids have suitable settling characteristics and the loading regime does not repeatedly disrupt the sludge blanket or scour settled material. A lamella clarifier for chemical wastewater is an inclined-plate option for suitable settleable solids; it should not be presented as a substitute for flotation of oily or colloidal material.
S3, the U.S. EPA’s Process Design Manual for Suspended Solids Removal published in January 1975, treats coagulation, flocculation, sedimentation and flotation as distinct but related operations. Chemical treatment can alter particle characteristics so that a later separation step can work effectively. That distinction matters: “DAF” and “clarifier” are separation technologies, while chemical coagulation and flocculation are upstream conditioning operations. A factory may need both, not as alternatives.
Neither process independently removes dissolved contaminants that do not precipitate, partition into a removable phase, or require biological or advanced treatment. Define the objective as a removal or protection requirement for the next process—for example, oil and grease reduction before biological treatment—rather than as a vague need for “better water.”
Performance Evidence and Where It Applies
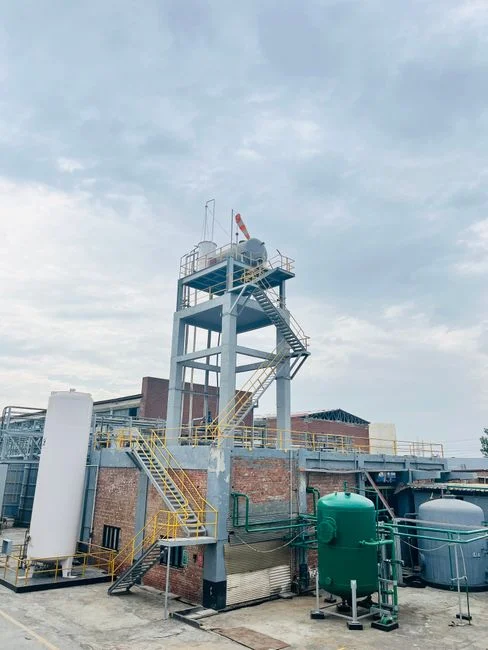
S1 reports removals above 99% for TSS and O&G across various industrial applications, but it does not establish a guaranteed result for every chemical-wastewater stream. The performance figure is a multi-application benchmark, not a design value that can be transferred without site chemistry, loading and pilot evidence.
The poultry further-processing case in S1 documents a dual-DAF arrangement. An initial DAF removed production TSS and O&G before an aerated pond; the existing DAF later clarified the treated effluent and removed phosphorus through metal-salt dosing. S1 reports TSS and O&G removals above 99% and reports that COD was reduced sufficiently for downstream anaerobic-lagoon and aerobic-SBR treatment. The useful procurement lesson is process integration: pretreatment was designed around the downstream biological train.
The acid-mine-drainage case shows why precipitation chemistry matters. S1 reports reductions of 87–89% for iron, manganese and aluminum, while pH moved from approximately 3 to pH 7–9. That evidence is consistent with metal precipitation followed by DAF; it is not a universal chemical-wastewater performance claim. The corn-dog plant case addresses a different target: S1 reports wastewater O&G concentrations as high as 8,000 mg/L in a high-oil application treated by DAF.
| Evidence in S1 | Reported result and scope | What a chemical factory may infer |
|---|---|---|
| Industrial DAF applications | Above 99% TSS and O&G removals across various industrial applications. | DAF can provide strong separation; a plant-specific guarantee still requires representative testing. |
| Poultry further processing | Above 99% TSS and O&G removal; COD reduction sufficient for downstream anaerobic lagoon and aerobic SBR treatment. | Pretreatment objectives should be linked to the complete downstream process. |
| Acid mine drainage | 87–89% reductions for iron, manganese and aluminum; pH moved from approximately 3 to pH 7–9. | Precipitation chemistry can make particulate metal separation effective. |
| Corn-dog plant | O&G concentrations as high as 8,000 mg/L in a high-oil pretreatment application. | High oil can be a DAF application, but skimming, conditioning and upset behavior need verification. |
S1 is undated and includes underlying project material from 2003; S3 dates to 1975. Treat both as foundational technical sources, not newly issued 2026 standards. For a current equipment comparison, use the chemical-wastewater scope rather than the headline efficiency, as discussed in DAF efficiency, cost and compliance considerations.
DAF or Clarifier for Chemical Wastewater: Scenario Decision Matrix
DAF is the stronger candidate when floatable O&G, colloids or light precipitate are central targets and the plant can control pH, conditioning chemicals, recycle pressure and float removal. A conventional clarifier is more defensible when settleable solids dominate, flow and loading are relatively stable, and a gravity process can meet the stated objective with lower process complexity.
Consider lamella clarification when compact inclined-plate separation is appropriate for settleable solids. The supplied equipment catalog lists surface loading rates of 20–40 m/h and chemical-consumption reductions of up to 30% for HydropureWater’s system. Those are catalog claims, not independent performance evidence; require the bidder to define the wastewater basis, chemical package and guarantee behind them.
| Wastewater condition | Preferred starting point | Required qualification |
|---|---|---|
| Free or emulsified oil is the main target | DAF | Verify conditioning, float removal and high-oil upset response. |
| Colloids or light precipitates are the main target | DAF | Confirm pH control, floc strength and recycle-system performance. |
| Settleable solids dominate and loading is stable | Conventional or lamella clarification | Verify settling velocity, sludge withdrawal and clarification-area basis. |
| Metals must be chemically precipitated | Precipitation followed by clarification or DAF | Establish pH, dose, residual metal and sludge route. |
| Biological solids require separation | DAF or gravity clarification based on solids behavior | Set the downstream biological objective and thickening requirement. |
| Mixed oil, biological solids and precipitate | Pilot-compare DAF and hybrid trains | Do not average unlike streams; evaluate independently and in combination. |
A hybrid train may be necessary when chemical precipitation must precede clarification, or when DAF must protect biological treatment. S1 documents DAF both as initial pretreatment and as later clarification in the poultry plant. That precedent supports process integration, but it does not establish the best arrangement for a Greensboro chemical stream.
Do not select on footprint alone. S1 states that rectangular DAF units can be more space-efficient and cost-effective than circular designs but are limited in flow capacity. The comparison between a DAF system and a lamella clarifier must therefore include future flow, maintenance access, float or sludge removal and expansion constraints.
Size the System From Factory Data and Pilot Results
A defensible quotation begins with five flow inputs: current average flow, peak flow, batch-dump flow, minimum flow and permitted discharge flow. Add TSS, settleable TSS, O&G, COD, metals, pH range and relevant process chemical additions. These inputs establish both hydraulic loading and whether chemical conditioning is required.
| Supplier response | Information to require | Reason for review |
|---|---|---|
| Hydraulic basis | Surface-overloading and hydraulic method; clarification-area method; detention basis. | Prevents an undisclosed flow or loading assumption from driving the proposal. |
| DAF design | Recycle ratio, whitewater-pressure design and saturation basis. | Links bubble availability to flotation performance. |
| Startup basis | Startup, upset and variable-batch assumptions. | Tests whether the design reflects plant operation. |
| Commercial scope | Equipment, installation, chemical storage, controls, utilities, civil work, float or sludge handling, commissioning and operator training. | Allows like-for-like total-cost comparison. |
Use the pressure question as a design review, not a vendor guarantee. S1 reports that at 20°C, maximum air saturation at 80 psig is 46% greater than at 50 psig. Higher recycle pressure can increase air availability and support smaller bubbles, so the supplier must state the whitewater design basis. The chemical dosing system should also be included where conditioning depends on measured pH, flow or solids conditions.
Pilot-test the actual wastewater when chemistry or loading is variable. S3 says its design criteria are guides that should be tempered by sound engineering judgment based on a complete analysis of the specific application. A useful pilot addresses peak conditions, chemical shock, float or sludge removal, downstream effects and sustained operation—not only a short run at average flow. Supplier maintenance assumptions can then be reviewed within the broader industrial wastewater equipment maintenance protocols for 2025.
Control Cost, Reliability and Permit Risk Before Purchase
Compare bids by operating burden and residual risk, not by equipment price alone. For DAF, include conditioning chemicals, recycle-pump energy, compressed-air demand, float handling and cleaning labor. For clarification, include coagulant or flocculant use, sludge withdrawal, sludge conditioning and downstream residual solids. Include the fate of separated material in every comparison.
| Review area | Check required from each bidder | Risk addressed |
|---|---|---|
| Variable chemistry | Control response to chemical shock, pH excursions, high O&G and batch discharges. | Underperformance and permit exceedance. |
| Controls and redundancy | Automatic skimming or sludge withdrawal, level control, interlocks and critical-condition monitoring. | Loss of containment or untreated bypass. |
| Application evidence | References with similar chemistry, pilot evidence, acceptance criteria and guarantee exclusions. | Transfer of performance from an unrelated stream. |
| Downstream treatment | Expected effect on biological, membrane and discharge requirements. | Passing pretreatment but loading the next process beyond its capability. |
| Total delivered cost | Equipment, installation, utilities, chemicals, civil work, residuals, maintenance, commissioning and training. | Hidden scope and lifecycle-cost differences. |
Flow variation, equalization and application-specific engineering judgment are central topics in EPA’s January 1975 Process Design Manual for Suspended Solids Removal. Treat that manual as foundational guidance, not a 2026 regulation. The factory’s current permit and downstream process design must establish present obligations.
Evaluate the complete treatment train. S1’s poultry installation reduced COD sufficiently for downstream anaerobic-lagoon and aerobic-SBR treatment, showing why pretreatment acceptance criteria should be expressed in terms of downstream protection. If separated solids require further concentration, compare downstream handling with the available plate-and-frame filter press while keeping its suitability conditional on the actual sludge and float properties.
The supplied evidence contains no defensible 2026 equipment-price range for chemical-wastewater DAF or clarifier systems. Do not accept an unsupported price. Request a quotation and identify broader cost-control questions through wastewater disposal cost-reduction measures for 2026.
Greensboro Factory Selection Checklist
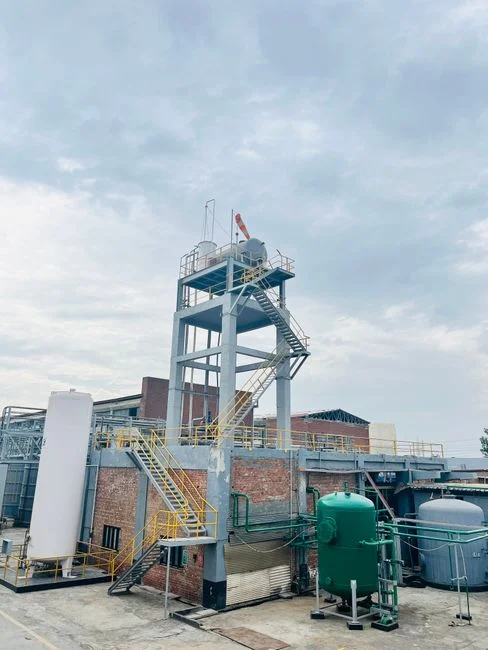
- Map every discharge stream and classify the contamination as soluble, suspended, oily, precipitated or biological.
- Define the separation target before selecting equipment: TSS, O&G, metals, COD reduction for downstream treatment or sludge thickening.
- Issue the same characterization, flow and operating data package to DAF and clarifier suppliers.
- Require each bidder to state its treatment objective, design basis, chemicals, utilities, footprint, controls, maintenance, sludge route and guarantee conditions.
- Use representative pilot evidence for uncertain or variable streams, including peak and upset conditions.
- Select the train with the lowest acceptable total cost that remains within compliance and reliability requirements.
- Confirm that pretreatment, downstream biological or membrane treatment, and final discharge requirements operate as one process.
This sequence prevents equipment from setting the treatment objective by default. It also gives the factory a defensible record for internal review and permitting discussions. The chemical-specific framing is consistent with the broader question of how an industrial wastewater COD-removal guide connects pretreatment to downstream biological treatment.
Frequently Asked Questions
Which equipment is cheaper for chemical wastewater: DAF or a clarifier?
Neither option can be ranked by price from the supplied evidence, and no defensible 2026 chemical-wastewater price range is available. Request installed quotations with identical scope: equipment, civil work, chemical storage and dosing, utilities, controls, float or sludge handling, commissioning, training and maintenance. Compare the resulting bids against each stream’s removal target and residual-disposal cost.
How should a Greensboro factory size a DAF or clarifier?
Size from current average, peak, batch-dump, minimum and permitted discharge flows, together with representative TSS, settleable TSS, O&G, COD, metals and pH data. Require the bidder to state its surface-overloading or clarification-area method, hydraulic basis and startup assumptions. Pilot-test variable chemistry and verify that future expansion remains within the proposed hydraulic and treatment envelope.
What wastewater data should be given to a wastewater-equipment supplier?
Provide a segregated stream profile with flow, TSS, settleable solids, O&G, COD, pH, metals, conductivity, temperature and chemical additions. Include samples and operating records from routine production, cleaning, dumping and upset periods. Also provide downstream biological, membrane and permit requirements so the supplier is designing to the same treatment objective.
Is DAF suitable when chemical wastewater contains high oil and grease?
DAF can be suitable when oil is a primary floatable target, but suitability depends on the oil form, concentration, conditioning needs and float-removal system. S1 documents a corn-dog plant application with wastewater O&G concentrations as high as 8,000 mg/L; that case is evidence of applicability, not a performance guarantee. Pilot-test the factory’s actual oil and confirm upset response.
When does a chemical factory need both chemical pretreatment and clarification?
It needs both when dissolved contaminants must first be converted into removable precipitate or when particles must be conditioned before physical separation. The 1975 EPA manual distinguishes coagulation, flocculation, sedimentation and flotation. A practical test is whether the proposed conditioning step creates floc with the settling or flotation characteristics required by the downstream separator.