The federal-local stack near Coleman: 40 CFR Part 436 plus the POTW pretreatment layer
Mining and metals plants near Coleman, US that discharge to a municipal sewer in 2026 do not get to pick between federal and local authority — those authorities stack on a single discharge. The federal floor is the Mineral Mining and Processing Effluent Guidelines and Standards at 40 CFR Part 436, which EPA promulgated in 1975 and amended in 1976, 1977, 1978, and 1979 (EPA, 2026-02). The rule covers wastewater discharges from mine drainage, mineral processing operations, and stormwater runoff, and its requirements are incorporated into NPDES permits (EPA, 2026-02). A permit issued to a Coleman-area mine will cite the 40 CFR Part 436 limits for the parameters the active subpart covers, and the Washington State Department of Ecology and the local sewer authority add their own conditions on top of those (EPA, 2026-02).
Every POTW that accepts industrial discharge runs a pretreatment program, and the local sewer authority reconciles EPA categorical standards with locally established limits for heavy metals, pH, and TSS. For a Coleman-area operation that means both sets of numbers have to be in front of the engineer at the same time when a treatment train is sized — not one or the other. The same dual-permit logic shows up in the parallel Montrose-area 2026 mining pretreatment guide and the Dayton 2026 mining pretreatment guide, and it is the first thing an auditor will check when a discharge hits a problem. Skipping either layer is the most common small-operator mistake and the most expensive one to fix after the fact.
The reserved-subpart trap: when 40 CFR Part 436 has no numbers for your mineral
Seven Pacific Northwest-relevant subparts in 40 CFR Part 436 are reserved as of EPA, 2026-02, and a reserved subpart carries no current numeric effluent limits. The reserved list includes Dimension Stone (Subpart A), Lightweight Aggregates (Subpart H), Lithium (Subpart U), Ball Clay (Subpart AH), Feldspar (Subpart AI), Talc/Steatite/Soapstone/Pyrophyllite (Subpart AJ), and Garnet (Subpart AK) (EPA, 2026-02). For a Coleman-area operator, that list is not academic: a dimension-stone quarry, a lightweight aggregate producer, and a lithium-exploration site all need to confirm subpart status before they ever size a clarifier, because the answer changes whether federal limits exist at all before the local layer kicks in (EPA, 2026-02).
The EPA NPDES industrial wastewater index documents how the categorical framework maps to active and reserved subparts, and that index is the first document an engineer should pull before opening a basis-of-design spreadsheet. Where a subpart is active, the NPDES permit cites 40 CFR Part 436 numeric limits for the parameters the subpart covers, and the local sewer authority adds its own conditions on top. Where a subpart is reserved, the operator gets no federal numeric anchor and has to build the design basis directly off the local POTW's discharge limits and the influent profile (EPA, 2026-02). Cross-check the subpart list against the EPA industrial wastewater page before any quotation goes out the door.
| Subpart | Mineral | Status (EPA, 2026-02) | Implication for a Coleman-area operator |
|---|---|---|---|
| A | Dimension Stone | Reserved | No federal numeric effluent limits; design basis is set by the local POTW and influent characterization. |
| H | Lightweight Aggregates | Reserved | No federal numeric effluent limits; local metal, pH, and TSS limits govern the basis of design. |
| U | Lithium | Reserved | No federal numeric effluent limits; lithium-exploration sites must design off local limits and the actual influent profile. |
| AH | Ball Clay | Reserved | No federal numeric effluent limits; confirm whether the operation falls under another active subpart before sizing. |
| AI | Feldspar | Reserved | No federal numeric effluent limits; local layer drives the design. |
| AJ | Talc, Steatite, Soapstone, Pyrophyllite | Reserved | No federal numeric effluent limits; local layer drives the design. |
| AK | Garnet | Reserved | No federal numeric effluent limits; local layer drives the design. |
Characterize the influent stream by stream before you talk to a supplier
Acid mine drainage is the most prevalent mining water quality problem, and the chemistry is well documented: when sulfide minerals such as pyrite and pyrrhotite are exposed to oxygen and water, oxidation reactions produce sulfuric acid that leaches iron, manganese, copper, zinc, arsenic, and cadmium at concentrations far exceeding regulatory limits (AMPAC USA, 2025-09). A copper mine, a coal operation, and a dimension-stone quarry cannot share a single default train — the chemistry is fundamentally different — which is why influent characterization by stream is a prerequisite to sizing (AMPAC USA, 2025-09).
Process water from ore processing — flotation, heap leaching, cyanide gold extraction, and chlorination circuits — typically runs high TDS and carries cyanide, ammonia, or chloramines depending on the circuit (AMPAC USA, 2025-09). Tailings pond effluent is the liquid fraction of tailings impoundments and contains fine solids, processing chemicals, and leached metals (AMPAC USA, 2025-09). Dewatering discharge is water pumped from underground mines or open pits to maintain access, and its composition varies by geology — in some settings, it is relatively clean; in others, it carries significant metal loading (AMPAC USA, 2025-09). The same stream-by-stream logic is used in the Montrose-area 2026 mining pretreatment guide, and skipping the characterization step is the fastest path to a train that does not hit setpoints on the worst stream.
| Stream | Typical character | Driver of unit-operation choice |
|---|---|---|
| Acid mine drainage (AMD) | Low pH, dissolved Fe/Mn/Cu/Zn/As/Cd, sulfate (AMPAC USA, 2025-09) | pH correction with lime raise >10 and metals precipitation; membrane polish for residual dissolved salts and metals. |
| Process water (flotation, heap leach, cyanide, chlorination) | High TDS, cyanide, ammonia, or chloramines depending on circuit (AMPAC USA, 2025-09) | Coagulation, clarification, multimedia filtration, and RO polish at >99% rejection of dissolved metals and salts (AMPAC USA, 2025-09). |
| Tailings pond effluent | Fine solids, processing chemicals, leached metals (AMPAC USA, 2025-09) | Coagulation and high-rate clarification (DAF or lamella) followed by multimedia filtration and downstream dewatering of the produced sludge. |
| Dewatering discharge | Variable by geology; in some settings relatively clean, in others significant metal loading (AMPAC USA, 2025-09) | Equalization and metal-specific precipitation; treat as a separate stream rather than blending blind into AMD or process water. |
The defensible 2026 six-step treatment train near Coleman
The defensible unit-operation sequence for a Coleman-area mineral mining or aggregate operation in 2026 has six steps, and each one maps to a specific unit operation. The literature and the commercial flow sheets reviewed point to the same order: pH correction first, then coagulation, then solids separation, then multimedia filtration, then a membrane polish when salts or trace metals persist, with monitoring and reporting on the back end (Genesis Water Technologies, 2025-11; PMC review, 2024-02).
Step 1 is pH correction. The objective is to raise pH so dissolved metals precipitate as hydroxides and gypsum drops out — a lime raise to pH >10 before thickening is the operating target for AMD feeds (PMC review, 2024-02). Step 2 is coagulation: match coagulant and flocculant to the floc density that drives the next step. Step 3 is solids separation, with a dissolved air flotation system for buoyant floc or floating fines, or a high-efficiency sedimentation tank (lamella clarifier) for sludge volume and footprint (Genesis Water Technologies, 2025-11). Step 4 is multimedia filtration, with the operator specifying target SDI after the filter rather than inlet turbidity (LiqTech, 2025-08). Step 5 is the membrane polish, with UF for fine colloids and an industrial RO system at 50–70% recovery for AMD feed, 70–85% recovery as the RO stage of a ZLD train, and >99% rejection of dissolved metals and salts (AMPAC USA, 2025-09). Step 6 is monitoring and self-monitoring through a PLC/HMI on pH, flow, and conductivity, with POTW self-monitoring records (LiqTech, 2025-08). Chemistry across the train is held by a PLC-controlled automatic chemical dosing skid, and a multi-media filter handles RO pretreatment.
| Step | Objective | Parameter target | Equipment |
|---|---|---|---|
| 1. pH correction | Precipitate dissolved metals as hydroxides; drop gypsum (PMC review, 2024-02) | pH >10 on AMD feed before thickening (PMC review, 2024-02) | Lime dosing via PLC-controlled automatic chemical dosing skid |
| 2. Coagulation | Aggregate suspended solids and fine metal particles into settleable or floatable flocs | Floc density matched to the downstream clarifier (Genesis Water Technologies, 2025-11) | Coagulant and flocculant dosing skid |
| 3. Solids separation | Remove the bulk of the precipitated solids | Buoyant floc/oil/fines vs. heavy sludge and footprint constraint (Genesis Water Technologies, 2025-11) | Dissolved air flotation system or high-efficiency sedimentation tank (lamella clarifier) |
| 4. Multimedia filtration | Drop turbidity and colloids to protect downstream membranes | Target SDI after the filter (LiqTech, 2025-08) | Multi-media filter |
| 5. Membrane polish | Remove fine colloids (UF) and dissolved salts and metals (RO) | RO at 50–70% recovery on AMD feed, 70–85% on a ZLD RO stage; >99% rejection of dissolved metals and salts (AMPAC USA, 2025-09) | Ultrafiltration system and industrial RO system |
| 6. Monitoring and self-monitoring | Maintain chemistry setpoints and POTW self-monitoring records | Continuous pH, flow, and conductivity (LiqTech, 2025-08) | PLC/HMI tied to the same control system as the dosing skid |
Equipment selection matrix for Coleman-area flows
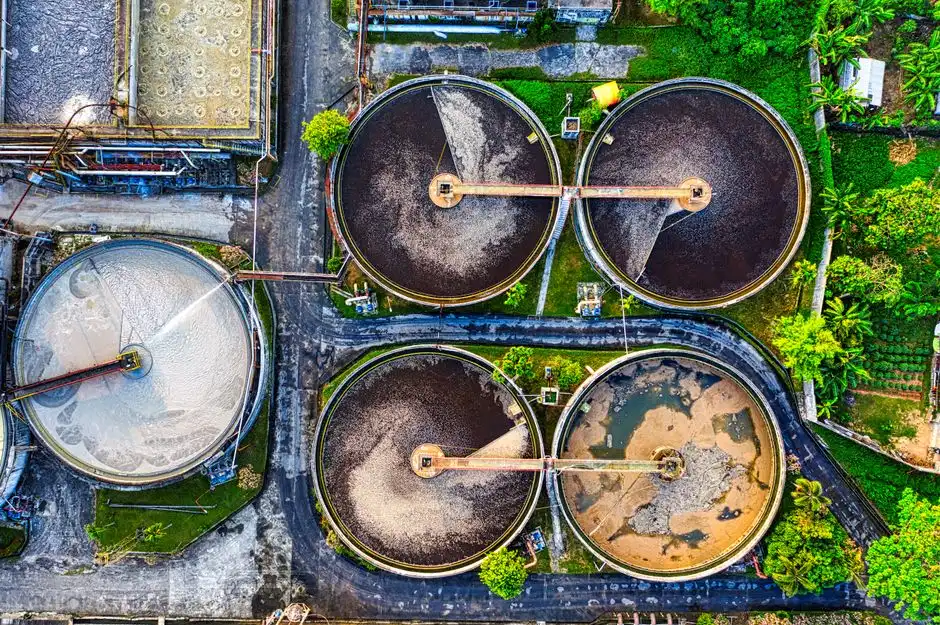
Equipment choices should be driven by the influent stream and the discharge limit, not by what a single supplier happens to stock. The clarification step is the central choice: a dissolved air flotation system for mining wastewater solids separation is preferred when the floc is buoyant or the influent carries oils or fines that float; a high-efficiency sedimentation tank (lamella clarifier) for metal hydroxide sludge is preferred when sludge volume and footprint are the constraint. Multimedia filtration is the workhorse for RO pretreatment, and the operator should specify target SDI after the filter rather than inlet turbidity (LiqTech, 2025-08). RO polish is the step conventional methods cannot replace: >99% rejection of dissolved metals and salts at 50–70% recovery on AMD feed or 70–85% on a ZLD RO stage (AMPAC USA, 2025-09). Sludge handling is the last unit operation, and a plate and frame filter press is the standard fit for the cake volumes produced by precipitation-based mining trains. Where the RO feed carries fine colloids that the multimedia filter cannot fully remove, an ultrafiltration system upstream of RO tightens the SDI and protects the RO membranes.
| Step | Pick this when | Equipment |
|---|---|---|
| Clarification — buoyant floc, oils, or floating fines | Floc density below water; fines that float | Dissolved air flotation system |
| Clarification — heavy floc, footprint-constrained | Sludge volume, footprint, no oil loading | High-efficiency sedimentation tank (lamella clarifier) |
| RO pretreatment | Target SDI after the filter (LiqTech, 2025-08) | Multi-media filter |
| RO feed polishing | Fine colloids not removed by multimedia filter | Ultrafiltration system |
| Membrane polish — salts and metals | Dissolved salts and metals above discharge limit | Industrial RO system at >99% rejection, 50–70% recovery on AMD feed, 70–85% on a ZLD RO stage (AMPAC USA, 2025-09) |
| Sludge dewatering | Cake volume from chemical precipitation | Plate and frame filter press |
Sizing logic and the basis-of-design checklist to hand a supplier
Size against the highest anticipated daily discharge, not the average, because peak flows drive equalization basin volume and pump selection. The information a buyer has to put into a quotation request is the peak and average flow in m³/h, the influent pH and metal profile from a representative sampling round, the local sewer authority discharge limits for metals, pH, and TSS, and the desired recovery percentage if reuse is in scope. The supplied research does not publish price points for a complete pretreatment train, so a buyer has to request a quotation against their own basis of design rather than rely on a published range. With that basis of design in hand, suppliers can quote a six-step train at the >99% rejection of dissolved metals and salts the literature reports (AMPAC USA, 2025-09). For more on how the influent profile and the local limits pair into a single basis-of-design package, the Montrose-area 2026 mining pretreatment guide walks the same checklist against a parallel site profile.
Reuse economics: how the compliance investment pays back near Coleman
Reverse-osmosis-based internal reuse can reduce freshwater consumption by 40–60% compared to once-through operation (AMPAC USA, 2025-09). That is the lever that turns a compliance cost into a capital project with a return: every cubic meter the plant reuses is a cubic meter it does not pay to draw from a freshwater source or to discharge to a sewer. Where ZLD is required, RO handles the bulk water recovery — typically 70–85% — before the more energy-intensive thermal stages handle the remaining concentrate, and the operator should request a recovery curve, not just a nameplate figure (AMPAC USA, 2025-09). The sizing logic is reuse as much as economics allow, then polish the rest to sewer quality, and the mine site water reuse sizing guide carries the reclaimed-water capacity calculations through to a defensible number.
Vetting a supplier for a Coleman-area mining pretreatment train
Look for a supplier that provides end-to-end service and helps the operator obtain a durable, efficient mining wastewater treatment system with a clear plan for operation and maintenance (LiqTech, 2025-08). Confirm the proposed scope ties chemistry dosing, PLC/HMI controls, and the membrane skid into a single integrated control system, and confirm the supplier has installed the same unit operations — DAF or lamella, multimedia filter, UF, RO, and sludge dewatering — at flows in the same order of magnitude as the Coleman site. For a parallel check on what the same six-step train looks like against a different tributary's local limits, the Montrose-area 2026 mining pretreatment guide is the nearest reference point.
Frequently Asked Questions
How does a Coleman-area operator confirm whether 40 CFR Part 436 has numeric effluent limits for their mineral before sizing a treatment train?
Check the EPA industrial wastewater page and the current 40 CFR Part 436 subpart list to confirm whether the mineral is in an active subpart with numeric limits or a reserved subpart. Reserved subparts as of EPA, 2026-02 include Dimension Stone (A), Lightweight Aggregates (H), Lithium (U), Ball Clay (AH), Feldspar (AI), Talc/Steatite/Soapstone/Pyrophyllite (AJ), and Garnet (AK). A reserved subpart carries no current numeric federal limits, so the design basis is set by the local POTW and the influent profile rather than by a federal number.
What should be included in a quotation request for a six-step mining pretreatment train near Coleman, and what does the supplied research say about price points?
Put the peak and average flow in m³/h, the influent pH and metal profile from a representative sampling round, the local sewer authority discharge limits for metals, pH, and TSS, and the desired recovery percentage if reuse is in scope into the request. The supplied research does not publish price points for a complete pretreatment train, so the buyer has to request a quotation against their own basis of design rather than rely on a published range. With that basis of design, suppliers can quote a six-step train at the >99% rejection of dissolved metals and salts the literature reports (AMPAC USA, 2025-09).
When is a DAF system the right clarifier choice versus a lamella clarifier for a Coleman-area mining train?
Pick a DAF system when the floc is buoyant or the influent carries oils or floating fines, and pick a lamella clarifier when sludge volume and footprint are the constraint and there is no oil loading (Genesis Water Technologies, 2025-11). The influent stream — AMD, process water, tailings pond effluent, or dewatering discharge — drives the choice, and the same logic shows up in the parameter-by-parameter step table earlier in this article.
How does a Coleman-area operator defend the basis of design to both the EPA and the local sewer authority in 2026?
Stack the two sets of numbers: the 40 CFR Part 436 subpart status from the EPA industrial wastewater page and the local sewer authority's discharge limits for metals, pH, and TSS, plus the influent profile from a representative sampling round, all in front of the engineer at the same time (EPA, 2026-02; LiqTech, 2025-08). Show the six-step train against that combined basis of design, with the RO polish sized at >99% rejection of dissolved metals and salts (AMPAC USA, 2025-09) and the self-monitoring plan tied to the PLC/HMI the POTW expects to see in the discharge report.