Why POME COD Is Hard to Treat
Palm oil mill effluent (POME) is a high-strength wastewater characterized by very high organic matter, suspended solids, oil and grease, and intense color, with raw COD typically falling between 15,000 and 100,000 mg/L depending on mill operations and dilution from condensate streams (Raji et al., RSC Advances, May 2026). POME leaves the sterilizer at 70–80 °C and carries 4,000–6,000 mg/L of oil and grease, which fouls membranes, strips dissolved oxygen from aerobic basins, and creates emulsions that resist gravity separation. Conventional ponding systems and single-stage anaerobic digestion face long treatment times, large land footprints, secondary sludge production, and inconsistent pollutant removal — ponding systems in particular can take 60–120 days to reach acceptable discharge quality and occupy several hectares per mill (Raji et al., 2026; ScienceDirect, Resources Chemicals and Materials, 2025). The combination of high temperature, high oil and grease, and COD variability creates shock-loading risks: a hot, oily slug entering an anaerobic lagoon can drop methane yield, lift effluent VFA, and push COD past compliance for days. For these reasons, no single technology reliably brings POME from raw strength to modern discharge limits; a staged train is the engineering default.
Typical POME Treatment Train in 2026
A POME treatment train sequences unit operations by function: oil and grit removal, equalization and cooling, biological reduction (anaerobic, sometimes followed by aerobic or membrane bioreactor polishing), and tertiary polishing such as membrane filtration, electrocoagulation, or advanced oxidation (ScienceDirect, 2025). The first stage strips free oil and settleable solids — typically with a DAF system for oil and suspended-solids removal ahead of biological treatment — because emulsified oil entering a digester or membrane will coat biomass and blind membranes within hours. Equalization then buffers flow and temperature so downstream biology runs in a mesophilic band near 35 °C. Anaerobic digestion (covered lagoon, CSTR, or UASB) carries the bulk COD load economically while generating biogas, but it rarely drives effluent below 250–500 mg/L COD on its own. Aerobic or MBR polishing takes the residual biodegradable fraction and lifts effluent to near-reuse quality, while tertiary steps (electrocoagulation, chitosan composite membranes, AOPs) strip the refractory COD, color, and trace organics that the biology leaves behind. The 2026 specification approach is to size each stage for what it does best and let polishing handle what biology cannot.
COD Removal by Technology: 2026 Comparison
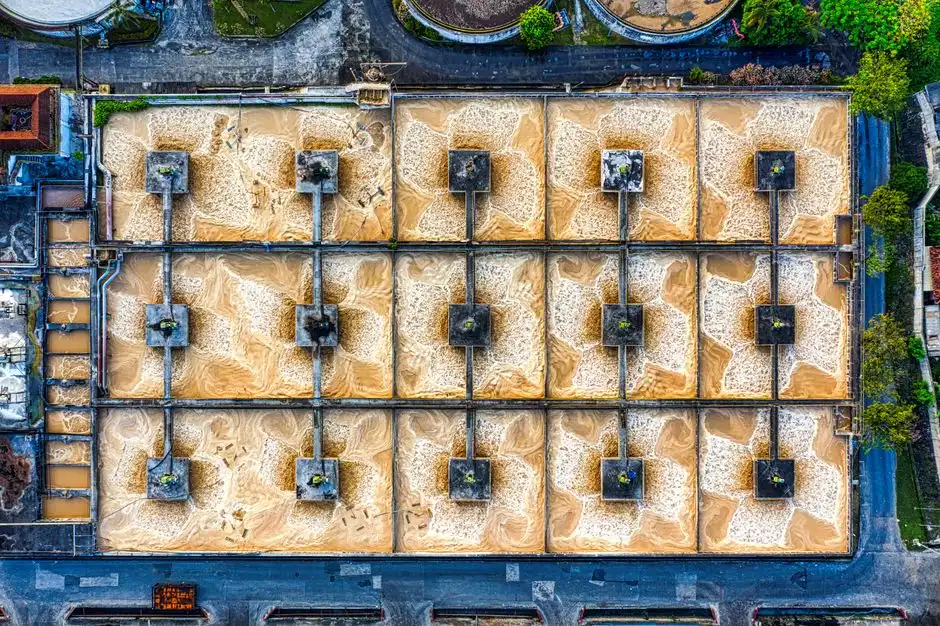
Six technology classes dominate POME COD removal in 2026, and the table below pairs the headline removal figures with the operating parameters an engineer puts on a P&ID. Anaerobic digestion — covered lagoons and CSTRs — delivers 80–95% COD removal at 20–60 day HRT with biogas recovery, but at the cost of large footprint and temperature sensitivity (ScienceDirect, 2025). Aerobic polishing and MBR systems cut footprint substantially and push effluent toward reuse quality; a submerged PVDF MBR is a common choice for the polishing step, and you can spec an MBR system for POME polishing with flat-sheet PVDF MBR modules for POME duty. Electrocoagulation with iron electrodes (2 cm gap, 12 V, 15 min) reaches 89.2% COD removal at pH 4 and 83.0% at pH 9 in a 10 L batch reactor, with decolorization up to 90.4% at pH 4 (Gobi et al., Zenodo, 2013). A chitosan-PVA-PEG composite membrane (1:1 ratio, 300 rpm cross-flow) achieves 97.24% COD rejection and 97.60% BOD rejection, with flux of 27.15 L/m²·h at 300 rpm versus 40.20 L/m²·h at 100 rpm (Wahyuni et al., 2016). Advanced oxidation processes (Fenton, ozone, photocatalysis) are effective on refractory COD and color but limited by reagent and energy cost (ScienceDirect, 2025). Nanochitosan adsorption is the emerging option, with large surface area and amino-group functionality that integrate with biological and physicochemical steps to lift overall removal (Raji et al., RSC Advances, May 2026).
| Technology | Typical COD removal | Influent COD range (mg/L) | HRT / contact time | Energy / footprint | Sludge yield |
|---|---|---|---|---|---|
| Anaerobic digestion (covered lagoon / CSTR) | 80–95% | 15,000–100,000 | 20–60 days (lagoon); 15–30 days (CSTR) | Low energy, very large footprint | Low biological yield; biogas offset |
| Aerobic / MBR polishing | 80–95% on residual | 250–2,000 (post-AD) | 6–24 h (aerobic); 8–16 h (MBR) | Moderate energy, small footprint | Moderate (MBR waste activated sludge) |
| Electrocoagulation (Fe, 12 V, 2 cm gap) | 83.0–89.2% | 500–5,000 (post-biology) | 15–30 min batch | Moderate energy, small footprint | High Fe(OH)₃ sludge |
| Chitosan-PVA-PEG membrane (1:1, 300 rpm) | 97.24% rejection | 100–2,000 (polishing) | 50 min cross-flow; flux 27.15 L/m²·h | Low–moderate energy, compact | Concentrate stream to dewater |
| Advanced oxidation (Fenton, O₃, photocatalysis) | 50–90% on refractory | 100–1,000 (polishing) | 30–120 min | High reagent/energy | Iron-rich chemical sludge (Fenton) |
| Nanochitosan adsorption | 50–85% (emerging) | 100–1,000 (polishing) | 30–120 min contact | Low energy, small footprint | Spent adsorbent; regeneration step |
Design Parameters That Drive POME COD Performance
The numbers an engineer needs to size equipment, set controls, and write operating procedures are the influent COD range, the HRT or contact time, the pH window, the current density or flux, and the fouling control strategy. Raw POME COD typically spans 15,000–100,000 mg/L; downstream of an anaerobic digester it falls to 250–2,000 mg/L before polishing, and downstream of a chitosan membrane it can reach sub-100 mg/L rejection-class values (Wahyuni et al., 2016; Raji et al., 2026). For electrocoagulation, current density is the master variable — the cited study tested 6, 12, and 18 V with a 2 cm electrode gap and reaction times of 5–60 min, finding 12 V and 15 min as the operating point that balances COD removal and energy (89.2% at pH 4, 83.0% at pH 9) (Zenodo, 2013). For membrane steps, flux and cross-flow velocity set the area requirement: 27.15 L/m²·h at 300 rpm versus 40.20 L/m²·h at 100 rpm in the chitosan study (Wahyuni et al., 2016), with higher rpm trading flux for pumping energy. For biological steps, covered lagoons typically run 20–60 day HRT, while CSTRs and UASBs shorten that to 15–30 days; mesophilic operation near 35 °C is the standard because POME arrives hot and must be cooled to avoid digester upset. High-efficiency sedimentation tanks upstream of the biological stage and a multi-media filter ahead of the membrane protect downstream equipment from suspended-solids carryover. For a deeper look at how an MBR unit integrates with the train, see the MBR process explainer; for digester upset diagnostics, the anaerobic digester troubleshooting guide covers the failure modes that show up most often on palm oil mill digesters.
| Stage | Key design parameter | Typical range | Source / study |
|---|---|---|---|
| Raw POME | Influent COD | 15,000–100,000 mg/L | Raji et al., 2026 |
| Anaerobic (covered lagoon) | HRT | 20–60 days | ScienceDirect, 2025 |
| Anaerobic (CSTR / UASB) | HRT | 15–30 days | ScienceDirect, 2025 |
| Electrocoagulation (Fe) | Voltage / time | 12 V, 15 min (peak COD) | Zenodo, 2013 |
| Electrocoagulation (Fe) | Electrode gap | 2 cm | Zenodo, 2013 |
| Electrocoagulation (Fe) | pH window | 4 (89.2% COD) / 9 (83.0% COD) | Zenodo, 2013 |
| Chitosan-PVA-PEG membrane | Cross-flow rpm | 100 rpm → 40.20 L/m²·h; 300 rpm → 27.15 L/m²·h | Wahyuni et al., 2016 |
| Chitosan-PVA-PEG membrane | Rejection (1:1, 300 rpm) | 97.24% COD, 97.60% BOD | Wahyuni et al., 2016 |
Integration: Putting the Train Together
The right sequence in 2026 is primary separation → equalization/cooling → anaerobic digestion → aerobic or MBR polishing → tertiary polishing → sludge dewatering. A DAF system for oil and suspended-solids removal ahead of biological treatment is the workhorse first step because it strips free oil, reduces TSS to a level the digester can tolerate, and prevents grease from coating biomass. Between the biological and membrane stages, an automatic chemical dosing system for pH and coagulant control stabilizes influent pH, breaks residual emulsions, and doses antiscalant to protect membrane life. For guidance on sizing the upstream clarifier that feeds the train, the primary clarifier specifications guide walks through the design numbers. At the back end, a plate and frame filter press for POME sludge handles the solids generated by electrocoagulation, biological wasting, and chemical precipitation, bringing cake dryness into a range that disposal or land application can accept. The integrated train is the 2026 default for mills facing tightening effluent COD limits, biogas-recovery incentives, and the operational cost of running any single stage in isolation.
Cost, Energy and Sustainability Trade-offs
Cost framing here is directional, because the cited studies do not publish dollar figures — describe drivers, not invented numbers. Biological steps (covered lagoon, CSTR, aerobic/MBR) carry low OPEX once running but high CAPEX for reactors and basins; long HRT translates directly into land cost, which is significant in Indonesia and Malaysia where mills operate on tight concession footprints. Electrocoagulation has a small footprint and moderate energy at the 12 V operating point reported (Zenodo, 2013), but generates iron-rich sludge that must be dewatered downstream. Membranes have high CAPEX and fouling-driven OPEX, but deliver the smallest polishing footprint and reuse-quality effluent — payback improves when the mill values water reuse or faces strict COD limits. AOPs and nanochitosan adsorption carry high reagent or material cost and are best applied as final polishing on a small flow after biological reduction has done the bulk of the work (ScienceDirect, 2025; Raji et al., RSC Advances, May 2026). Across all options, biogas revenue from the anaerobic stage partially offsets OPEX and is often the line item that moves a project from marginal to bankable.
Frequently Asked Questions
What is the typical COD range for raw palm oil mill effluent?
Raw POME COD typically falls between 15,000 and 100,000 mg/L, depending on mill operations and dilution from condensate streams (Raji et al., RSC Advances, May 2026).
How effective is electrocoagulation for POME COD removal?
Electrocoagulation with iron electrodes (2 cm gap, 12 V, 15 min) achieves 89.2% COD removal at pH 4 and 83.0% at pH 9, with decolorization up to 90.4% at pH 4 in a 10 L batch reactor (Zenodo, 2013).
What removal rates do chitosan composite membranes achieve on POME?
A chitosan-PVA-PEG composite membrane (1:1 ratio, 300 rpm cross-flow) reaches 97.24% COD rejection and 97.60% BOD rejection, with flux of 27.15 L/m²·h at 300 rpm versus 40.20 L/m²·h at 100 rpm (Wahyuni et al., 2016).
Why do POME treatment plants use a multi-stage train instead of one technology?
POME arrives at 70–80 °C with high oil and grease and COD from 15,000 to 100,000 mg/L; no single technology reliably takes it to modern discharge limits, so the 2026 default is primary separation, anaerobic digestion, polishing, and tertiary treatment in series (Raji et al., 2026; ScienceDirect, 2025).