Why Jetersville Food and Beverage Factories Are Reopening the DAF-vs-Clarifier Question in 2026
For a Jetersville, Virginia food or beverage factory in 2026, default to a DAF system: it removes 92–97% of TSS and up to 95% of FOG on a footprint roughly one-fifth that of a gravity clarifier, while producing 3–5% float solids versus 1–2% underflow. A conventional clarifier still wins only for heavy inorganic grit or where a serviceable basin already exists, and 40 CFR Part 408 plus Virginia DEQ pretreatment set the compliance floor.
The procurement pressure is no longer theoretical. The categorical standards that govern Jetersville F&B plants are 40 CFR Part 408 subparts — Dairy Products Processing (Subpart B), Canned and Preserved Fruits and Vegetables (Subpart C), Canned and Preserved Seafood (Subpart D), and Meat Products Processing (Subpart E) — operating under the 40 CFR Part 403 general pretreatment framework. Mid-Atlantic F&B raw effluent routinely runs 200–3,000 mg/L FOG and 500–5,000 mg/L TSS, with hourly swings from CIP caustic and batch cook condensate dumps that can double those numbers inside ten minutes. The Chesapeake Bay TMDL overlay is the 2026-specific driver: residual BOD, ammonia, and phosphorus reaching the James River service authority POTWs now trigger surcharges under Virginia DEQ pretreatment review, and a smaller chemical footprint plus lower hauled sludge volume is a direct permit-review advantage. The question most Jetersville engineers are answering in 2026 is which primary clarifier to put on the purchase order — a DAF skid or a new concrete clarifier basin — not a polish-stage retrofit, which is the framing the Pacific-region DAF vs clarifier guide covers separately.
How a DAF and a Clarifier Actually Move Solids
DAF and gravity clarification look similar from outside the fence line — a tank, a skimmer or rake, an outlet — but the physics that moves solids is opposite. A DAF presses micro-bubbles onto flocculated particles and floats them upward. A clarifier waits for gravity to pull them down.
In a DAF, 10–30% of clarified recycle is pressurized in a saturation vessel at 4–6 bar to 85–95% air saturation efficiency, then released through needle-valve orifices. The dissolved air comes out of solution as 20–100 μm micro-bubbles, with the 30–50 μm band as the engineering target because it gives the right surface-area-to-buoyancy ratio without violent rising velocity. Bubbles nucleate on pre-formed flocs, the air-filled aggregate rises to the surface in minutes, and a paddle skimmer pulls the float at 3–5% solids. The four dials an operator turns are recycle ratio, saturation pressure, polymer charge and dose, and pH, held in the 6.5–8.5 window where most cationic flocculants perform.
A conventional gravity clarifier relies on Stokes' law: a particle settles when gravitational force overcomes drag. For FOG, fruit pulp, blood proteins, and fine cellulose — all with specific gravity at or below 1.0 — that settling requires hours, which is why clarifier retention sits at 2–4 hours and surface loading rates stay below 2 m/h. Rake-driven sludge moves to a central hopper, and the underflow exits at 1–2% solids. To force a clarifier to remove FOG, operators overdose coagulants — typically 3–5× the polymer a DAF would need — and accept both the OPEX penalty and the larger sludge volume; field removal tops out at 40–70% FOG in the best-operated cases.
Side-by-Side: DAF vs Clarifier on the Numbers That Matter in Jetersville
Procurement readers want the trade-off in 30 seconds, so the matrix below is the anchor. Numbers reflect typical operating bands for food and beverage streams; verify against jar testing and vendor proposals before locking a P&O.
| Parameter | Dissolved Air Flotation (DAF) | Conventional Gravity Clarifier |
|---|---|---|
| TSS removal (high-FOG F&B) | 92–97% (HydropureWater field data, 2025) | 40–70% on heavy inorganics; <50% on FOG (HydropureWater field data, 2025) |
| FOG / O&G removal | Up to 95%; 95% in 2026 Ecologix case pair | 40–60%; 70% in 2026 Ecologix case pair on the same stream |
| Surface loading rate | 5–15 m/h | <2 m/h |
| Footprint at 50 m³/h | ~15 m² skid (per ZSQ series dissolved air flotation system sizing) | ~200 m² concrete basin (per high-efficiency sedimentation tank civil footprint) |
| Sludge / float solids | 3–5% float | 1–2% underflow |
| Energy | 0.2–0.5 kWh/m³ (recycle pump + air compressor) | Minimal pumping; no aeration load |
| Polymer dose (high-FOG) | 1× reference | 3–5× reference when forced to settle FOG |
| CAPEX band, 50 m³/h greenfield | $120,000–$180,000 mid-range SS304 ZSQ (HydropureWater, 2025) | Comparable once civil work is included; cheaper if a basin exists |
The single most decisive number for a space-constrained Jetersville plant is the surface loading rate: 5–15 m/h for a ZSQ series dissolved air flotation system versus less than 2 m/h for a clarifier. On a 50 m³/h dairy or brewery wash stream, that gap is the difference between a 15 m² skid and a 200 m² concrete basin — and most rural Piedmont food plants do not have 200 m² of unused pad near the sewer tie-in.
Jetersville-Specific Variables Generic Guides Get Wrong
Generic DAF-versus-clarifier guides fail Mid-Atlantic buyers because they assume 20–25 °C effluent and a neutral-pH stream. Four Jetersville variables invalidate that assumption and force a temperature-corrected, chemistry-corrected, and material-corrected design.
First, Mid-Atlantic effluent swings from ~10 °C in winter to ~30 °C in summer; saturation efficiency and micro-bubble yield drift with it, so a DAF must be sized for real peak hourly flow with a temperature derate rather than nameplate flow. Second, brewery CIP and rendering cook condensate routinely push pH above 9, which collapses cationic flocflocculant performance — the 6.5–8.5 window is a hard precondition, and an automatic chemical dosing skid with pH trim is not optional. Third, the Chesapeake Bay TMDL overlay for nitrogen, phosphorus, and sediment penalizes residual BOD, ammonia, and TSS reaching the James River service authority POTWs, so a smaller chemical footprint and lower sludge volume are direct permit-review advantages. Fourth, hot washwater, fruit acids, and rendering cook condensate demand SS316 over the SS304 baseline for both DAF tanks and skimmer components — a real Jetersville decision input that no Pacific guide addresses. For a Jetersville plant running rendering cookers or fruit-acid sauces, the SS316 uplift is roughly 15–25% on tank CAPEX but eliminates the chloride pitting and organic-acid attack that has taken SS304 tanks out of service inside five years on Mid-Atlantic sites.
Sizing a 50 m³/h Jetersville DAF: the 2026 Requisition Checklist
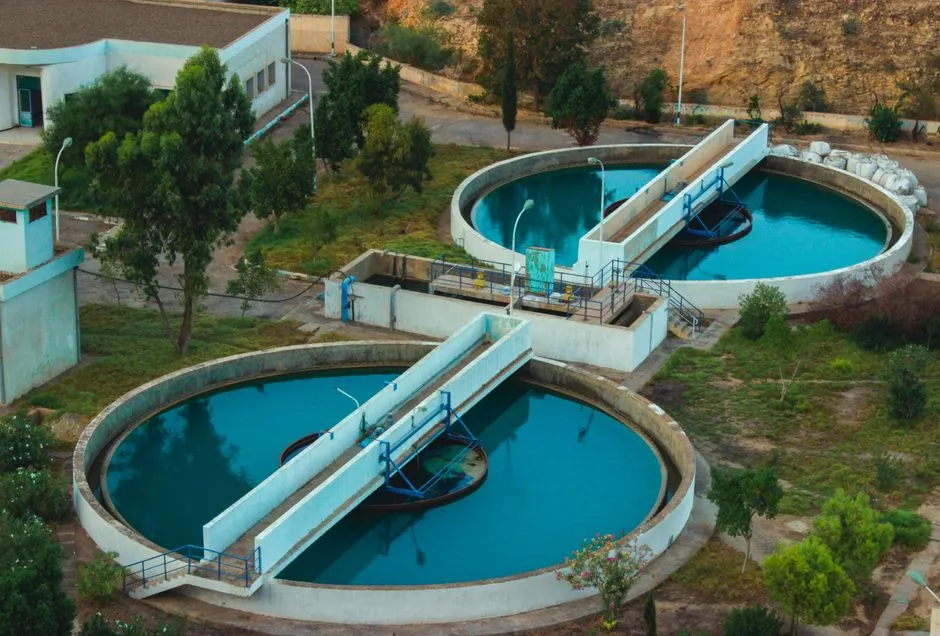
The matrix tells you what a DAF does; the spec table below tells you what to put on the requisition. The ZSQ line covers 4–300 m³/h across 13 standard models, but the underlying sizing rules have not changed.
| Requisition Item | Specification | Why it matters for a Jetersville food plant |
|---|---|---|
| Flow range | 4–300 m³/h across 13 standard ZSQ series dissolved air flotation system models | Covers a small craft beverage line through a large dairy or rendering plant |
| Sizing basis | Peak hourly flow plus temperature derate, not nameplate | Winter 10 °C effluent carries less air than summer 30 °C effluent |
| Material of construction | SS304 standard; SS316 for hot washwater, rendering cook condensate, fruit acids, and high-chloride seafood | Fruit acids and rendering cook condensate demand SS316 in most Jetersville cases |
| Upstream screening | Rotary mechanical bar screen with 2–3 mm openings | Clogged recycle nozzles are the #1 unplanned shutdown cause; hair, fruit solids, and packaging fragments reach the DAF within hours without screening |
| Chemical dosing | Automatic chemical dosing skid with flow-proportional and streaming-current trim | Locks pH at 6.5–8.5 and polymer dose to jar-test target |
| Automation | PLC-controlled skimmer speed, polymer dose, pressure setpoints; remote alarming | Required for 2026 labor-light operations across multi-site Mid-Atlantic operators |
| Downstream dewatering | Plate and frame filter press to push float to 25–35% cake solids | Cuts hauled volume another 80–85% beyond DAF float; works in series with the food factory expansion ETP retrofit pattern |
The three most common sizing mistakes on Jetersville projects are: (1) using nameplate flow rather than peak hourly flow, which leaves no headroom for the CIP surge; (2) ignoring temperature, so saturation efficiency drifts and float carryover appears from October through April; and (3) underspecifying the upstream screen, which lets hair, fruit solids, and packaging fragments clog recycle nozzles within weeks. All three are visible in field service logs inside the first quarter of operation.
Payback Math for a 50 m³/h Jetersville Brewery or Dairy
Engineers do not buy equipment; they buy payback periods. The example below uses a representative 50 m³/h brewery or dairy washwater stream with 1,500 mg/L TSS and 600 mg/L FOG — typical of a Jetersville craft brewery, dairy, or cheese plant discharging under 40 CFR Part 408 and a Virginia DEQ pretreatment permit.
CAPEX lands at $120,000–$180,000 for a mid-range SS304 ZSQ series unit with PLC and dosing skid. Annual energy runs 0.2–0.5 kWh/m³ × 50 × 8,000 h × $0.14/kWh Mid-Atlantic industrial tariff, or roughly $11,000–$28,000. Annual polymer consumption sits between 200 and 2,000 kg/yr at $4–$8/kg depending on jar-test results — a jar test on the actual influent should always precede the polymer lock, because the best- to worst-case gap is wider than the entire annual maintenance budget on a mid-sized plant. The line item that drives the payback is sludge disposal: DAF float at 3–5% solids runs 50–70% lower volume than clarifier underflow, which alone saves $40,000+ per year versus the clarifier baseline. Add avoided FOG and TSS surcharges under Virginia DEQ and the local James River service authority and the project lands at 1.5–3 year payback, with the higher end of the energy band, the worst-case polymer dose, or an unpriced TSS surcharge pushing the math past three years. For context on how a DAF retrofit slots into a broader plant expansion, the food factory expansion ETP guide walks the same procurement pattern at a larger CAPEX scale.
When a Jetersville Plant Should Still Pick a Clarifier
Credibility comes from naming the cases where DAF is overkill. A clarifier remains the better answer for heavy inorganic grit streams with little FOG, where a clarifier's 40–70% TSS removal beats a DAF and polymer demand is low; for very low-flow side streams well below 5 m³/h, where the DAF skid CAPEX does not amortize; and for sites with a serviceable existing concrete clarifier basin that a retrofit can reuse at a fraction of new-build cost. A hybrid DAF-as-polish ahead of an existing clarifier often reaches 40 CFR Part 408 compliance at roughly half the CAPEX of a full replacement, which is the same retrofit logic covered for a similar Piedmont and Mid-Atlantic stream in the PA-side DAF vs clarifier guide.
Frequently Asked Questions
What removal efficiency does a DAF deliver versus a clarifier on a Jetersville food or beverage stream?
A DAF delivers 92–97% TSS removal and up to 95% FOG removal on flocculated dairy, brewery, or rendering washwater, versus 40–70% TSS and less than 50% FOG on a gravity clarifier for the same stream. The gap is driven by surface loading rate: 5–15 m/h on DAF versus less than 2 m/h on a clarifier, because FOG and protein have specific gravity at or below 1.0 and will not settle under gravity within practical retention.
What is the 2026 payback for a 50 m³/h DAF on a Jetersville brewery or dairy stream?
A 50 m³/h mid-range SS304 ZSQ unit with PLC and dosing skid typically lands between $120,000 and $180,000, with a 1.5–3 year payback from sludge-disposal savings (50–70% lower volume than clarifier underflow) and avoided FOG and TSS surcharges under Virginia DEQ and the local James River service authority (HydropureWater field data, 2025).
Which regulations govern DAF or clarifier selection for a Jetersville F&B plant?
The compliance floor is 40 CFR Part 408 categorical standards — Dairy Products Processing (Subpart B), Canned and Preserved Fruits and Vegetables (Subpart C), Canned and Preserved Seafood (Subpart D), and Meat Products Processing (Subpart E) — operating under the 40 CFR Part 403 general pretreatment framework, with Virginia DEQ pretreatment review and James River service authority surcharges on top.
What are the three sizing errors generic DAF-versus-clarifier guides make for Jetersville plants?
Generic guides size to nameplate flow rather than peak hourly flow, ignore the temperature derate from ~10 °C winter to ~30 °C summer effluent, and underspecify the upstream rotary mechanical bar screen that keeps recycle nozzles clear. All three show up in field service logs inside the first quarter of operation and each one can be prevented at the requisition stage.