What an Effluent Treatment Plant in Ahmedabad Actually Does
An industrial effluent treatment plant in Ahmedabad is a four-stage train — preliminary (screening, grit removal), primary (equalization, dissolved air flotation or clarifier), secondary (biological — activated sludge, sequencing batch reactor, or membrane bioreactor), and tertiary (filtration, disinfection, RO if reuse is needed) — designed to meet Gujarat Pollution Control Board (GPCB) inlet and outlet norms for discharge into sewer, CETP, or surface water. The U.S. EPA defines effluent as "wastewater – treated or untreated – that flows out of a treatment plant, sewer, or industrial outfall" and the same definition holds under the Water (Prevention and Control of Pollution) Act, 1974 that GPCB enforces in Gujarat (per S5, EPA/Clean Water Act framework).
At the preliminary stage, a rotary mechanical bar screen removes rags, plastics, and grit that would otherwise damage downstream pumps. Primary treatment — typically equalization plus DAF or a clarifier — drops over 70% of suspended solids and roughly 40% of BOD before water enters biology (per S4, Ahmedabad manufacturer data). Secondary biological treatment then removes 70–90% of BOD and 80–90% of dissolved solids using aerobic or anaerobic微生物 consortia, with the secondary clarifier underflow producing a sludge consistency of 1–1.5% that must be thickened and dewatered by a plate and frame filter press before disposal (per S4).
Three terms confuse most first-time buyers. ETP treats industrial effluent on a single factory's premises. STP (sewage treatment plant) handles domestic sewage. CETP (common effluent treatment plant) takes pre-treated trade effluent from multiple factories in one industrial cluster — Jetpur is Gujarat's largest textile CETP, and Ahmedabad's Naroda and Vatva clusters have similar shared infrastructure. Picking the wrong system class is the most common procurement mistake in this region.
Ahmedabad Industrial Effluent Profile: Why One ETP Design Does Not Fit All
Textile-dyeing effluent from the Naroda–Jetpur corridor carries high COD (typically 800–2,500 mg/L in raw composite samples), recalcitrant azo dyes, sulfate from sodium sulfate baths, and trace heavy metals (Cu, Cr) from mordants. A 2026 whole-genome sequencing study of Enterococcus casseliflavus strain CV10 — isolated from the Jetpur CETP itself — confirmed that the cluster's effluent "often overwhelms conventional physicochemical treatment" and that specialized bioaugmentation strains with FMN-dependent azoreductases, multicopper oxidases, and alkanesulfonate monooxygenases are required to break down the dye structures (per S2, Kachhela et al., J Environ Sci Health A, June 2026, DOI 10.1080/10934529.2026.2682090). The same study reported a 3.5 Mb genome assembled at 98.7% completeness — concrete evidence that Jetpur effluent biology is now well-characterized at the genomic level.
Chemical and dye-intermediate effluent from Vatva and Narol behaves differently: pH swings between 2 and 11 are routine, solvent traces (toluene, xylene, chlorinated compounds) suppress biology, and TDS often exceeds 8,000 mg/L because of dissolved salts. These plants need a robust equalization tank with mechanical mixing, pH correction dosing, and an oil-grease removal stage before any biological reactor.
Pharmaceutical and auto-ancillary effluent from Sanand and Changodar has lower influent colour, moderate COD (400–1,200 mg/L is typical), and variable solvent loads that change shift-to-shift. The lower suspended-solids load and the demand for stable reuse-quality effluent make this segment a natural fit for an MBR membrane bioreactor system, which combines a suspended-growth biological stage with sub-1 μm membrane filtration in a single skid. A more detailed five-stage wastewater treatment walkthrough explains how these three profiles map to the same unit operations but at very different design parameters.
GPCB and CPCB Discharge Norms Every Ahmedabad ETP Must Meet
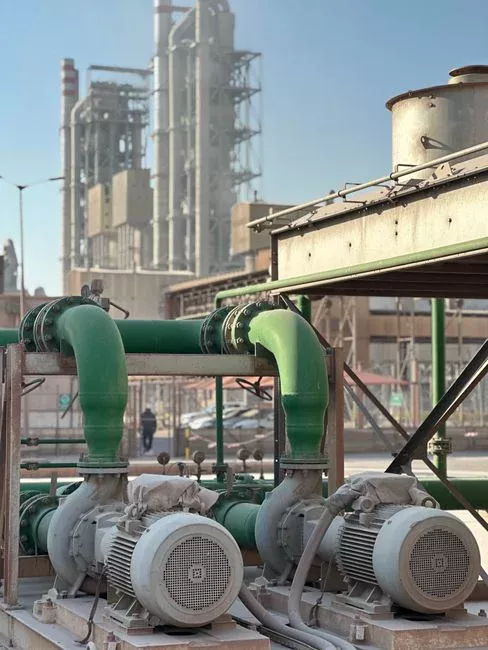
GPCB issues consent to establish and consent to operate under the Water Act, 1974 and the Air Act, 1981, with effluent limits set by industry category, discharge destination (sewer for CETP, inland surface water, or land), and the industrial zone's pollution category. GPCB and CPCB schedule limits are revised periodically — the buyer must verify the current mg/L thresholds for their specific category against the latest GPCB consent order before specifying any ETP; do not assume the limits in any single older reference document still apply.
Typical analytical parameters tested in every GPCB consent include pH (commonly 6.5–8.5 outlet range across categories), total suspended solids, total dissolved solids, COD, BOD₃ at 27°C (the Indian standard temperature, not the 20°C used in EU/US methods), oil and grease, sulphates, chlorides, and a heavy-metal panel (Cr, Ni, Zn, Cu, Pb, Cd). Textile consents add specific azo-dye restrictions; pharma consents add specific solvent and API residues. The U.S. EPA "secondary treatment" benchmark of 30 mg/L BOD and 30 mg/L TSS (per S5, 40 CFR 133) is useful as a reference for Ahmedabad exporters who must also meet buyer-side standards in the EU or US.
Compliance risk is real: any ETP discharging without a valid GPCB consent risks immediate closure under the Water Act, and the Ahmedabad Municipal Corporation enforces oil-grease separator and pre-treatment requirements for any trade effluent entering the city sewer. Buyers should ask the vendor for a copy of at least two reference plants where the ETP consistently meets GPCB outlet norms on the latest consent renewal.
| Parameter | Typical ETP inlet (industrial composite) | Indicative GPCB outlet range (verify with current consent) | Why it matters |
|---|---|---|---|
| pH | 4–11 (varies by process) | 6.5–8.5 in most consent orders | Protects sewer biology and receiving water |
| TSS | 200–1,500 mg/L | 30–100 mg/L | Sludge load and discharge solids |
| COD | 500–3,000 mg/L | 100–250 mg/L | Direct measure of organic pollution |
| BOD (3-day, 27°C) | 200–1,200 mg/L | 20–50 mg/L | Biodegradable organic load |
| Oil & grease | 50–500 mg/L | 5–10 mg/L | Can smother biological flocs |
| Heavy metals (Cr/Ni/Cu/Pb) | Trace–50 mg/L combined | 0.5–2 mg/L individual | Toxic to biology and receiving water |
Technology Comparison: ASP, SBR, MBR and DAF Pretreatment
The four biological reactor types most commonly quoted for Ahmedabad ETPs are activated sludge process (ASP), sequencing batch reactor (SBR), membrane bioreactor (MBR), and moving bed biofilm reactor (MBBR). Each hits a different balance of footprint, effluent quality, and operating complexity. A DAF system for primary treatment usually sits ahead of all four for textile and food effluent because it removes fats, oils, greases, and fine suspended solids with a small footprint before biology.
Conventional ASP is the lowest-CAPEX option and is what most Ahmedabad reference plants run. SBR offers better effluent stability because it batches fill, react, settle, and decant in a single tank. MBR pushes the secondary stage much further — the membrane retains essentially all suspended solids and most colloids, producing reuse-ready water with no separate clarifier. MBBR adds plastic media to an aeration tank and is a good retrofit for overloaded ASP plants. A regional ETP cost breakdown for another Indian industrial city shows how these four technologies map to different ₹/KLD bands outside Gujarat.
| Technology | Typical BOD removal | Footprint | MLSS range (mg/L) | Sludge yield | Effluent quality | Best-fit Ahmedabad industry |
|---|---|---|---|---|---|---|
| ASP (conventional) | 70–90% | High | 1,500–3,000 | 0.4–0.6 kg/kg BOD | 30 mg/L BOD, 30 mg/L TSS typical | Chemical, large textile plants |
| SBR | 85–95% | Medium | 2,000–5,000 | 0.3–0.5 kg/kg BOD | 20 mg/L BOD, 20 mg/L TSS | Textile, food, batch processes |
| MBR | 95–99% | Low | 6,000–12,000 | 0.25–0.4 kg/kg BOD | <5 mg/L BOD, <1 mg/L TSS | Pharma, auto-ancillary, reuse |
| MBBR | 80–92% | Medium-high | 3,000–5,000 (biofilm carriers) | 0.3–0.5 kg/kg BOD | 25 mg/L BOD, 30 mg/L TSS | Retrofit of overloaded ASP |
One-sentence decision rule per industry: textile in Naroda/Jetpur → DAF plus ASP or SBR with bioaugmentation, sized for high salinity; pharma/auto in Sanand → MBR for stable reuse water; chemical in Vatva → equalization plus neutralization plus ASP with toxic-load monitoring; food in Narol → DAF plus ASP. The 70–90% BOD and 80–90% dissolved-solids removal figures for secondary biology are baseline ASP numbers from the Ahmedabad manufacturer dataset (S4); MBR pushes both above 95% because of the physical membrane barrier (per S4 and the MBR product reference).
CAPEX and OPEX Ranges for an ETP in Ahmedabad (Indicative 2026)
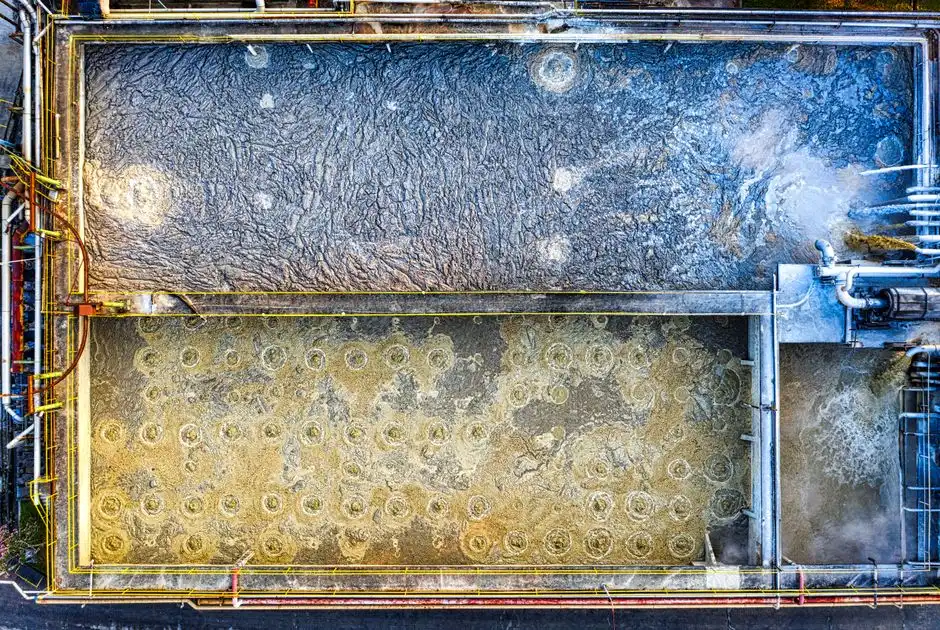
No publicly scraped source publishes Indian ETP CAPEX in ₹/KLD, so the ranges below are indicative 2026 market figures assembled from publicly known equipment costs and civil-works norms — every figure must be re-verified with shortlisted vendors before any CAPEX submission. As a working envelope, civil plus mechanical plus electrical cost typically lands at ₹8–15 lakh per KLD for small plants (≤50 KLD), ₹5–10 lakh per KLD for medium plants (50–250 KLD), ₹4–7 lakh per KLD for large plants (250–1,000 KLD), and ₹3–5 lakh per KLD for very large plants (>1,000 KLD), driven mainly by the economies of scale on the biological reactor volume and the MBR membrane area.
OPEX is dominated by power for aeration (typically 0.4–0.8 kWh per kg BOD removed, with aeration blowers drawing 40–60% of total plant power), membrane replacement (membranes typically last 3–5 years before replacement, at ₹1,500–3,000 per m² of membrane area), chemical dosing (coagulant, polymer, pH adjuster) handled by an automatic chemical dosing system, and sludge disposal to TSDF or co-processing in a cement kiln. Power tariff, influent loading, and consent-driven reuse requirements move the OPEX line more than any other variable.
Ahmedabad plants that add an RO polishing loop to MBR permeate for boiler feed or cooling-tower make-up typically hit payback in 18–36 months because the avoided fresh-water purchase at ₹60–100 per kL and the reduced sewer-discharge volume both fall straight to the bottom line. For Surat-area process plants, a separate Gujarat industrial wastewater guide for cooling and process blowdown covers the reuse-side economics in more detail.
| Plant size (KLD) | Indicative CAPEX (₹ lakh per KLD, 2026) | Typical monthly OPEX (₹ per KLD treated) | Largest OPEX line item |
|---|---|---|---|
| ≤50 (small) | 8–15 | 900–1,500 | Power (aeration) |
| 50–250 (medium) | 5–10 | 600–1,100 | Power + chemical dosing |
| 250–1,000 (large) | 4–7 | 450–900 | Membrane replacement (if MBR) |
| >1,000 (very large) | 3–5 | 350–700 | Sludge disposal + power |
Choosing an ETP Manufacturer in Ahmedabad: 10-Point Vendor Checklist
A shortlist of three to five vendors is normal; the checklist below is what separates a competent ETP firm from a fabrication shop that bolts tanks together. The Jetpur CETP genomic research (per S2, 2026) is a useful reminder that complex Gujarat effluent rarely behaves like the textbook — pilot data and a process flow diagram (PFD) are not optional for textile and chemical work.
A credible PFD should show, in one drawing, the influent screening with a rotary mechanical bar screen, equalization, primary clarification or DAF, biological stage, secondary clarifier or membrane skid, tertiary filtration and disinfection, the sludge line to a plate and frame filter press, and all recycle streams. If the PFD is missing any of these, ask why before you ask about price.
| # | Check | Weight | Pass / fail evidence to ask for |
|---|---|---|---|
| 1 | GPCB consent track record in Gujarat | High | At least 3 reference plants with active consents |
| 2 | In-house design vs sub-contracted fabrication | High | List of in-house process and structural engineers |
| 3 | PLC/SCADA capability | Medium | Sample HMI screen and tag list |
| 4 | Guaranteed effluent in the contract | High | Performance bank guarantee tied to outlet BOD/COD |
| 5 | 12-month AMC and spares availability | Medium | AMC cost as a separate line item |
| 6 | Reference plants in the same industry and size band | High | Site visit, not just a PDF brochure |
| 7 | Pilot or jar-test data on your effluent | High for textile/chemical | Lab report dated within last 6 months |
| 8 | Timeline and liquidated-damages clause | Medium | LD at 0.5–1% per week of delay, capped at 10% |
| 9 | Compliance with latest GPCB/CPCB norms | High | Signed undertaking to upgrade if norms tighten |
| 10 | Documentation: P&ID, GA drawing, O&M manual | Medium | Delivered before dispatch, not after |
One warning that saves real money: reject any quotation that lists CAPEX only, with no separate OPEX line for power, membranes, chemicals, and sludge. Two vendors quoting the same membrane equipment can produce lifetime costs that differ by 30–40% purely on aeration design and chemical strategy. The Jetpur case is a useful Gujarat-specific reminder — bioaugmentation, advanced oxidation, or simply tighter dissolved-oxygen control each push OPEX in different directions, and the difference is visible in a 12-month operating cost, not in a CAPEX table.
Frequently Asked Questions About ETP in Ahmedabad
What is the difference between ETP, STP, and CETP?
ETP treats industrial effluent at a single factory, STP treats domestic sewage, and CETP is a shared facility that takes pre-treated trade effluent from many factories in one cluster — Jetpur is Gujarat's largest textile CETP, and Ahmedabad's Naroda and Vatva clusters operate similar shared infrastructure. ETP outlet norms under GPCB are typically tighter than CETP inlet norms because the CETP is designed to polish, not to start from raw.
How much does an ETP cost per KLD in Ahmedabad?
As an indicative 2026 envelope, civil plus mechanical plus electrical CAPEX lands at ₹8–15 lakh per KLD for small plants (≤50 KLD), ₹5–10 lakh per KLD for medium plants (50–250 KLD), ₹4–7 lakh per KLD for large plants (250–1,000 KLD), and ₹3–5 lakh per KLD for very large plants (>1,000 KLD) — verify all numbers with shortlisted vendors before any budget submission.
Which biological treatment is best for a textile ETP in Ahmedabad?
For most Ahmedabad textile plants — including the Jetpur–Naroda corridor — DAF plus ASP or SBR with bioaugmentation is the workhorse configuration, removing 70–90% of BOD at the secondary stage (per S4) and polishing to 20–30 mg/L BOD at the outlet. MBR is worth the higher CAPEX only if the plant needs reuse-quality water for boiler or dyeing feed.
How long does GPCB consent take and what documents are needed?
Consent to establish typically takes 30–90 days and consent to operate takes another 30–60 days, with timelines varying by industry category and zone. The vendor's scope should include the process flow diagram, P&ID, GPCB application forms, and a site visit for the joint inspection.
What is the typical payback for a reuse loop in Ahmedabad?
An Ahmedabad plant adding an RO polishing loop to MBR permeate for boiler feed or cooling-tower make-up typically hits payback in 18–36 months, because the avoided fresh-water cost at ₹60–100 per kL and the reduced sewer-discharge volume both fall directly to the bottom line. For a broader cost benchmark, the ETP cost breakdown for another Indian industrial city provides a useful cross-regional comparison.
Frequently Asked Questions
What is the cost of an ETP plant in Ahmedabad for a 100 KLD textile unit?
For a 100 KLD textile effluent treatment plant in Ahmedabad, the capital expenditure (CAPEX) typically ranges from INR 25 lakhs to INR 45 lakhs, depending on the complexity of the treatment train and the degree of automation. This estimate includes civil works, mechanical equipment, electrical panels, and instrumentation, but excludes land costs and specialized ZLD (Zero Liquid Discharge) components like Multiple Effect Evaporators (MEE) or Agitated Thin Film Dryers (ATFD).
Operational expenditure (OPEX) for such a unit generally falls between INR 35 and INR 65 per cubic meter of treated water. These costs are influenced by local electricity tariffs in Gujarat and the specific chemical dosing requirements necessitated by the high TDS and COD loads common in Ahmedabad’s textile cluster.
Which ETP technology is best for textile dye effluent in Gujarat?
The most effective technology for textile dye effluent in Gujarat currently involves a combination of Physico-Chemical treatment followed by Advanced Oxidation Processes (AOP) and biological treatment. Given the high color and recalcitrant organic load, Fenton’s reagent or Ozone-based oxidation is highly recommended prior to biological degradation to break down complex azo dyes.
For plants aiming for compliance with GPCB norms, a sequential treatment approach—utilizing Equalization, Coagulation-Flocculation, Biological Aeration (MBBR or MBR), and tertiary filtration (Activated Carbon and Sand Filters)—is the industry standard. Reverse Osmosis (RO) is often required as a final stage if the facility is mandated to achieve Zero Liquid Discharge (ZLD).
What are the GPCB discharge limits for industrial effluent in Ahmedabad?
The Gujarat Pollution Control Board (GPCB) mandates stringent discharge standards for industrial effluents depending on the point of disposal. For discharge into inland surface waters, the general limits include a pH range of 6.5 to 8.5, a Biochemical Oxygen Demand (BOD) not exceeding 30 mg/l, and a Chemical Oxygen Demand (COD) typically capped at 250 mg/l.
Total Suspended Solids (TSS) must remain below 100 mg/l, while Oil and Grease levels must be less than 10 mg/l. Industries located in specific industrial estates or those discharging into CETPs may face additional parameters regarding Total Dissolved Solids (TDS), which are often restricted to below 2100 mg/l, depending on the specific environmental clearance of the receiving water body.
How long does it take to install an effluent treatment plant in Ahmedabad?
The typical timeline for the design, construction, and commissioning of an ETP in Ahmedabad ranges from 4 to 8 months. The initial phase, involving site survey, pilot testing, and GPCB approval documentation, usually occupies the first 4 to 6 weeks. Civil construction, including the casting of RCC tanks, requires 10 to 14 weeks depending on the soil bearing capacity and site logistics.
Mechanical and electrical installation, including piping, pump integration, and control panel setup, typically takes 6 to 8 weeks. Final commissioning, including trial runs and achieving stable biological culture (seeding) in aeration tanks, requires an additional 2 to 4 weeks before the plant can be certified for full-scale operation.
Is MBR better than conventional activated sludge for an Ahmedabad pharma plant?
For an Ahmedabad-based pharmaceutical plant, Membrane Bioreactor (MBR) technology is generally superior to Conventional Activated Sludge (CAS) processes. MBR systems provide a significantly higher quality of permeate by utilizing microfiltration or ultrafiltration membranes, which effectively remove bacteria and suspended solids, resulting in a BOD of less than 5 mg/l and ensuring the effluent is suitable for secondary applications or RO feed.
Furthermore, MBR systems offer a smaller physical footprint—often 50% to 70% less than CAS systems—which is a critical advantage given the high land costs in Ahmedabad's industrial zones. While MBR requires higher energy consumption for membrane scouring and more frequent chemical cleaning (CIP) of membranes, the consistency in effluent quality makes it the preferred choice for pharmaceutical units handling variable and complex organic loads.