How to Choose Between DAF and Clarifier for Plastics and Rubber Wastewater
North Baltimore plastics and rubber factories should choose based on the wastewater, not the industry label. Select dissolved air flotation (DAF) when oil, grease, latex, coating residues, plasticizers, or other floatable material is a meaningful fraction of the load; select a clarifier when bench testing shows that conditioned solids settle reliably. Mixed streams may need DAF plus clarification. EPA identifies flotation and gravity separation as distinct solids-removal processes and emphasizes coagulation, flocculation, equalization, and application-specific design. In 2026, require factory wastewater data, a pilot or jar-test basis, and calculations for recycle, surface loading, float and sludge recovery, utilities, and final disposal before approving equipment.
DAF attaches conditioned particles to pressurized-air microbubbles, lifts them to a skimmable surface layer, and removes the resulting float. Gravity clarification uses settling to move conditioned solids into a bottom sludge zone; a lamella plate clarifier uses inclined plates to increase effective separation area. EPA’s Process Design Manual for Suspended Solids Removal, January 1975, frames process selection around the properties of the actual solids and the required separation rather than around a generic industry description.
Neither process removes dissolved contaminants by itself. Downstream biological treatment, filtration, or another unit may still be required for dissolved organics, metals, toxicity, nutrients, or reuse criteria. This makes the preliminary equipment decision a solids-separation decision—not a complete treatment-train decision.
| Selection condition | Primary mechanism | What the buyer should establish |
|---|---|---|
| Material is meaningfully floatable | DAF flotation and surface skimming | Floatable fraction, conditioning response, bubble attachment, and float destination |
| Conditioned solids settle reliably | Gravity sedimentation | Settling behavior, surface-loading calculation, sludge withdrawal, and treatment objective |
| Both floatable and settleable fractions are material | Hybrid flotation and clarification | Removal sequence, intermediate water quality, separate recovery streams, and handling burden |
For a fuller application of this screening logic, see the plastics and rubber wastewater comparison.
Map the Wastewater Fractions Before Choosing Equipment
Industrial wastewater characterization must resolve contaminant fractions before equipment can be selected because a plastics or rubber factory may send oily wash water, dispersed latex, coating residue, fillers, grit, and dissolved process chemicals in the same discharge. Sample production and washdown periods separately, then composite only with a documented flow basis. Record flow, pH, temperature, oil and grease, suspended solids, settleable solids, turbidity, and relevant process identifiers.
Screen the following fractions independently:
- Free oil and grease: determine whether it is free-flowing, emulsified, or already associated with solids.
- Latex and dispersed polymers: distinguish free-flowing latex from coagulated or flocculated material.
- Coating and adhesive residues: identify whether the material floats, disperses, or adheres to other particles.
- Plasticizer-associated material: characterize its physical state and whether analytical results represent dissolved material, suspended material, or both.
- Fillers, pigments, grit, and heavy sediment: determine settleability and grit-related abrasion or loading.
- Dissolved contaminants: identify constituents that solids-removal equipment cannot remove.
EPA’s January 1975 manual states that particle size, specific gravity, and strength or shear resistance can affect separation performance. It also describes coagulation and flocculation as means of changing solids characteristics so that physical separation becomes more effective. This supports a jar-test program that evaluates settling, float recovery, chemical dose, and floc breakage under representative mixing conditions.
| Waste fraction | Physical condition to identify | Initial process direction |
|---|---|---|
| Free oil and grease | Free-flowing, emulsified, or solids-associated | DAF screening; conditioning may be needed for emulsified material |
| Latex or dispersed polymers | Free-flowing, colloidal, or already flocculated | DAF and coagulation/flocculation trials |
| Coating and adhesive residues | Floatable, dispersible, or adherent to solids | DAF screening with recovery testing |
| Fillers, pigments, and grit | Colloidal, settleable, or heavy sediment | Clarification screening and grit assessment |
| Dissolved contaminants | Soluble or speciated in the wastewater | Route to downstream biological, filtration, or other treatment |
EPA gives 200 mg/L as a typical raw domestic wastewater suspended-solids concentration in its January 1975 manual. That municipal value is neither a plastics or rubber influent assumption nor an effluent prediction. Use factory data, not that value, as the design basis. Chemical testing should also define the feed requirements for an automatic chemical dosing system.
What DAF Changes Inside a Plastics and Rubber Treatment Train
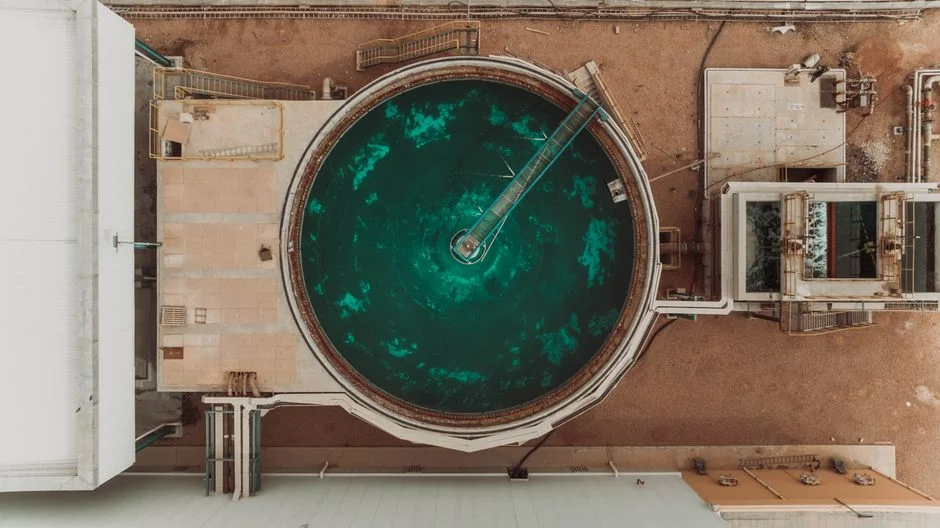
DAF is a conditioned separation process in which pressurized air is released as microbubbles, particles attach to those bubbles, and the attached solids rise to a surface layer that a skimmer removes. HydropureWater’s 2026 article, citing Clearwater Industries’ commercial literature dated 2026-04-27, identifies the microbubbles as 30–50 micrometers. That figure is commercial guidance, not a universal plant guarantee.
Coagulation and flocculation are central to performance. Coagulation destabilizes particles, while flocculation creates larger structures more capable of contacting bubbles. The same clearwater Industries guidance cited by HydropureWater in 2026 recommends pairing DAF with coagulation and flocculation. A supplier that omits chemical assumptions, mixing intensity, contact time, or dose-control logic has not defined the process.
Hahn’s Fundamentals of Wastewater Flotation, published in 2010, identifies air-to-solids ratio, hydraulic loading, chemical addition, pressure, flow rate, and equalization as flotation design variables. Equalization is particularly important where washdown and production flows create changing oil, solids, and temperature conditions. The bidder should show how its selected industrial dissolved air flotation system responds to that duty cycle rather than quoting one nominal treatment rate.
Heavier particles can settle even inside a flotation unit. A credible DAF proposal therefore needs a bottom-solids collection and removal arrangement, not just a surface skimmer. It should also state how float is drained, stored, dewatered, and disposed. HydropureWater lists 13 DAF catalog configurations from 4–300 m³/h; those are available configurations, not proof that any listed model fits a North Baltimore factory.
When Gravity Clarification Is the Better Fit
Gravity clarification is the stronger starting choice when jar or pilot testing shows that most target solids can be conditioned into floc that settles reliably. A lamella clarifier uses inclined plates to increase effective separation area before solids slide into a collection zone. The objective is then bottom-sludge recovery, not float recovery.
HydropureWater’s product specification lists 20–40 m/h surface loading for its lamella clarifier. That is a manufacturer specification, not a transferable design value. The supplier should show the calculation, selected peak and average flows, settling characteristics, inlet behavior, and assumed wastewater condition behind the proposed loading.
Ecologix Systems’ commercial selection guidance states generally that clarifiers have lower operating costs and are suited to heavy solids. Treat that as a qualitative commercial comparison, not a guaranteed lifecycle cost. A North Baltimore comparison still needs chemical consumption, labor, sludge handling, utilities, maintenance, and disposal assumptions calculated for the actual site.
Oil, grease, latex, and other floatable contaminants can defeat a gravity-only approach or require a preceding removal stage. Conversely, using DAF as the only stage when most solids are heavy and settleable may add unnecessary flotation duty and create a larger float-handling burden. EPA’s January 1975 manual addresses clarifier design, chemical sedimentation, solids-contact clarification, and flocculation as parts of a broader selection framework. The lamella clarifier for settleable industrial solids should therefore be specified around the desired floc structure and sludge destination.
DAF, Clarifier, or Hybrid Treatment: Decision Matrix
A hybrid train is the leading architecture when floatable material and heavy settleable solids are both material parts of the same stream. Ecologix Systems’ commercial guide reports that, on one food-processing stream, DAF achieved 95% oil and grease removal compared with 70% for a clarifier. This is a site-specific commercial example, not a plastics or rubber performance guarantee, but it illustrates why the same wastewater can respond differently to flotation and settling.
| Comparison basis | DAF | Lamella clarification | Hybrid flotation plus clarification |
|---|---|---|---|
| Primary waste fraction | Oil, grease, latex, coating residues, and other floatable material | Conditioned fillers, pigments, grit, and other settleable solids | Both floatable and settleable fractions are material |
| Separation mechanism | Bubble attachment and surface flotation | Gravity settling through inclined plates | Flotation and gravity separation in a defined sequence |
| Expected recovered material | Surface float | Bottom sludge | Separate float and sludge streams |
| Chemical dependence | Depends on particle attachment and required floc structure | Depends on formation of reliably settling floc | Requires coordinated chemical and hydraulic design |
| Footprint and utility burden | Calculate from the selected configuration, recycle basis, air generation, equalization, and site constraints | Calculate from basin geometry, surface loading, sludge handling, and site constraints | Calculate from both unit trains, intermediate transfer, and recovery systems |
| Handling burden | Float water content, recoverability, odor control, and dewatering | Sludge withdrawal, conditioning, water content, and disposal | Separate handling and disposal requirements for both products |
Do not assign an exact capital cost, energy consumption, footprint, or sludge volume from generic comparisons. Those are outputs of the selected configuration and factory data. Apply four questions before naming a preliminary architecture:
- Is the target material predominantly floatable?
- Does conditioned material settle reliably?
- Are both fractions material to the treatment objective?
- Must one recovered stream be recovered for reuse or a higher-value disposal route?
The plastics and rubber wastewater comparison provides a useful companion framework, but the North Baltimore factory’s analytical and operating data remain controlling.
Build a Vendor Proposal That Can Be Compared Fairly
Comparable bids require identical wastewater inputs, duty cycles, treatment objectives, recovered-material destinations, and acceptance criteria. A DAF proposal should identify the flotation model, recycle basis, hydraulic calculation, chemical assumptions, air and recycle utilities, bottom-solids collection, float handling, controls, materials of construction, and performance-test method. A clarifier proposal should identify its surface-loading calculation, inlet configuration, flocculation or sludge-recirculation arrangement, sludge withdrawal, basin access, odor controls, and assumed wastewater characteristics.
Both bids must use the same average and peak flow, production and washdown schedule, industrial wastewater characterization, electrical supply, installation constraints, and required effluent performance. Where flow varies, require the supplier to explain its controls and equalization strategy. EPA’s January 1975 manual identifies flow variation and equalization as design considerations; Hahn’s 2010 flotation source also identifies equalization as a factor affecting treatment efficiency.
| Proposal item | DAF evidence required | Clarifier evidence required |
|---|---|---|
| Hydraulic basis | Selected model, flow, recycle basis, and hydraulic calculation | Surface-loading calculation, inlet design, and basin geometry |
| Chemical assumptions | Coagulant, flocculant, dose range, mixing, contact, and controls | Coagulant, flocculant, dose range, mixing, flocculation, and sludge conditioning |
| Recovery | Skimming, float discharge, bottom-solids removal, and storage | Sludge withdrawal, collection, conditioning, and discharge |
| Utilities and materials | Power, compressed air, recycle flow, controls, and corrosion materials | Power, sludge mechanism, controls, and corrosion materials |
| Performance and service | Acceptance test, guarantees, training, maintenance, and support | Acceptance test, guarantees, training, maintenance, and support |
Treat float and sludge as products or disposal burdens. Ask for expected water content, recoverability, dewatering needs, odor control, downstream handling, and final destination. Jar testing or a pilot trial is warranted when particle behavior is mixed or uncertain; it also supports planning an industrial wastewater treatment station. Any dewatering assumption should be checked against options such as the plate-frame filter press rather than inferred from the upstream unit.
North Baltimore Implementation and Compliance Questions
The discharge route determines whether solids removal alone is adequate for the North Baltimore site. A plant may discharge to a sanitary sewer, an industrial pretreatment system, a permitted outfall, or a zero-liquid-discharge route, and each route creates different treatment, documentation, and residual-management requirements.
No universal plastics or rubber effluent limit can be inferred from the supplied research. Confirm current permit and sewer requirements with the receiving authority and the site’s environmental manager. The bid should also include available footprint, electrical supply, compressed air, drainage, corrosion exposure, odor controls, noise limits, maintenance access, and future expansion requirements.
DAF and clarification primarily address suspended solids and floatable material. Dissolved organics, toxicity, metals, pH, nutrients, or reuse requirements may require biological, filtration, polishing, or other downstream treatment. A wastewater plant acquisition discussion can be useful for identifying due-diligence questions, but it does not establish North Baltimore compliance requirements or the receiving route for a plastics or rubber facility.
Frequently Asked Questions
Which option will cost less to operate for a North Baltimore factory?
Do not compare from equipment price alone. Ecologix Systems’ commercial guidance states generally that clarifiers have lower operating costs, while DAF may be better suited to specific oily contaminants. Request each bidder’s chemical consumption, compressed-air and recycle requirements, power demand, labor, maintenance, float or sludge handling, dewatering, and disposal assumptions using the same wastewater basis. Without those inputs and local utility rates, no defensible lifecycle cost or payback period can be stated.
How should a plastics or rubber wastewater skid be sized?
Catalog capacity is not design sizing. HydropureWater lists 13 DAF configurations from 4–300 m³/h, but the selected model must follow from factory wastewater characterization, average and peak flow, duty cycle, required separation, recycle basis, chemical response, and site-specific hydraulic calculations. For clarification, require the supplier’s surface-loading calculation and the same factory data. Pilot or jar-test results should substantiate the assumptions before equipment capacity is accepted.
How should DAF and clarifier suppliers be compared?
Require every bidder to use the same wastewater characterization, flow schedule, treatment objective, recovery assumptions, utilities, controls, materials of construction, service scope, and acceptance criteria. A DAF bid should expose recycle and bottom-solids handling; a clarifier bid should expose surface loading and sludge withdrawal. This common-basis check is more revealing than comparing published removal percentages from different sites.
When is a hybrid DAF-plus-clarifier train warranted?
Consider hybrid treatment when the stream contains a material floatable fraction—such as oil, latex, or coating residue—and a material settleable fraction such as fillers, grit, or flocculated solids. DAF can recover the float while clarification captures the heavier solids, but the sequence must be established by testing rather than by treating both units as mandatory. Compare recovered-stream quality, transfer requirements, chemical use, utilities, footprint, and separate handling burdens.