Determine Whether Textile Sludge Fits a Belt Press
A belt filter press can suit textile wastewater sludge when continuous drainage, adjustable compression and manageable cake discharge match the plant’s solids loading. Selection depends on sludge characteristics, polymer conditioning, hydraulic and solids loading rates, belt cleaning, target cake dryness and available space. The supplied 2024 study identifies textile sludge as capable of producing cakes with high solids concentrations, but its polymer-sludge case produced only 19% dry solids with a vacuum belt filter, compared with 35% using a filter press. Because performance is sludge-specific, buyers should request representative testing before fixing belt width, filtration area or expected cake dryness.
The first screening step is a representative feed characterization, not a generic capacity calculation. The 2024 Processes study characterized an industrial polymer-effluent sludge containing approximately 9% dry solids, COD exceeding 40,000 mg/L, TSS of 10,500 mg/L and pH of 8.5. Those values describe that case, not every textile ETP sludge. A buyer should request equivalent measurements together with sludge origin, fiber content, variability and the treatment stage represented by the sample.
Textile sludge should be treated as a candidate for relatively high-solids cake, not a guaranteed outcome. Processes noted in March 2024 that sludge from industries including textiles can produce dewatered cakes with significantly high solids concentrations. The same source states that most belt-press applications require polymer addition before dewatering. Polymer selection and dose should therefore be developed with representative sludge because conditioning changes floc structure, filtration behavior, cake release and downstream disposal characteristics.
| Selection input | Buyer information required | Decision use |
|---|---|---|
| Feed solids | Dry-solids content and TSS, measured on representative samples | Defines the hydraulic and solids loading entering the press |
| Sludge composition | Textile ETP origin, fiber content, treatment stage, COD and pH | Identifies conditioning and filtration risks |
| Variability | Across production, cleaning and batch-settlement cycles | Sets operating-control and buffering requirements |
| Conditioning | Polymer type, dose point, required mixing and expected filtrate response | Determines whether the selected configuration can retain solids |
| Output target | Required cake solids, filtrate quality and permitted disposal route | Provides the acceptance basis for comparison |
The chemical-feed scope should be defined with the same care as the press. An automatic chemical dosing system may be relevant where polymer preparation and feed must be coordinated with feed rate and sludge condition, but the supplier still needs a feed-characterization result and representative trial to establish the recipe. Do not use the textile example as a universal design basis: it was polymer sludge from an industrial effluent treatment plant, not a controlled comparison of every textile application.
Map the Belt Filter Press Process to the Required Performance
A belt press separates free moisture in a defined sequence: uniform slurry distribution, gravity drainage, progressive belt compression and cake discharge. Dewater.com describes slurry entering a specially designed head box, free moisture separating through moving belts, gradual compression in an adjustable wedge zone, and dry cake being removed by doctor blades. Each stage must be matched to the sludge and the required output rather than treated as an automatic result of machine width.
For a textile ETP, the head-box arrangement must distribute conditioned sludge consistently across the available filtration area. The gravity drainage zone then establishes how much free water can leave the slurry before compression. Progressive wedge compression can increase cake solids, but excessive or poorly controlled compression may impair drainage. Cake release must remain practical with the selected belt material, polymer condition and discharge route.
Operating controls determine whether the machine can hold its performance envelope. The Processes study identifies belt speed, belt tension, belt porosity, vacuum set point, steam injection and lime flow as variables affecting the vacuum belt installation tested in 2024. For a gravity-and-pressure belt press, the buyer should request controls or adjustment provisions for belt speed, belt tension and pressure profile, together with a defined belt-cleaning sequence. Dewater.com likewise identifies the need for chemical conditioning and even feed distribution for effective use of filtration area.
| Process stage | Required operating data | Performance to verify |
|---|---|---|
| Head box and feed distribution | Feed rate, conditioned-solids concentration and distribution uniformity | Full use of filtration area without excessive edge loss |
| Gravity drainage zone | Belt speed, retention path and drainage-zone condition | Removal of free moisture before compression |
| Wedge compression | Pressure profile, belt tension and adjustment range | Target cake solids without unacceptable solids loss |
| Cleaning and discharge | Washwater demand, wash cycle, doctor-blake condition and cake route | Stable operation and cake release |
| Whole system | Filtrate flow, solids capture and operating hours | Compliance with the specified discharge and mass-balance requirements |
Set the performance targets before comparing machines. In the 2024 industrial case, the vacuum belt filter produced cake at 19% solids, while the replacement filter press produced 35% solids cake. The comparison demonstrates that belt filtration and a filter press are not interchangeable for that tested polymer sludge. It does not establish that the same 35% result applies to a textile ETP; the buyer should request a site-specific trial or supplier performance calculation based on representative conditioned sludge.
Choose the Configuration That Fits the Feed
The correct belt-press architecture follows from drainage behavior and feed solids, not from a generic preference for more compression. Komline-Sanderson’s Series III belt filter press is offered in three-belt, two-belt and extended-gravity two-belt designs. Its manufacturer states that basic-machine selection depends on sludge type and feed solids, confirming that belt width alone is not a complete design basis.
A two-belt configuration should be evaluated when the required gravity drainage and compression sequence fits the available footprint and the feed does not need a separately adjustable drainage stage. A three-belt arrangement provides an independent gravity zone; Komline-Sanderson describes this as using a more open belt for rapid drainage of water. That architecture is worth reviewing when a textile sludge drains slowly or when an upstream thickening stage would improve downstream dewatering.
The extended-gravity design adds drainage length, while the independent gravity zone can also be arranged to operate as a thickener before the dewatering section. These are manufacturer-specific configurations, not universal rules. Komline states that its independent gravity zone can handle dilute sludge with suspended solids below 1.5%, while standard designs require feed-specific review. Use that statement to define questions for testing and supplier selection; do not transfer the threshold to another machine without evidence.
| Configuration | Evaluate when | Key question for representative testing |
|---|---|---|
| Two-belt | The feed can drain and compress adequately within the standard sequence and the installation footprint is constrained | Does the standard gravity section provide enough residence time before the wedge zone? |
| Three-belt with independent gravity zone | Slow drainage, dilute feed or thickening-before-dewatering is operationally valuable | Does the independent zone improve feed concentration without increasing retained solids? |
| Extended-gravity two-belt | Additional drainage is needed before final compression | What are the tested solids concentration and hydraulic loading at the gravity-zone outlet? |
| Combined thickening and dewatering | Plant operation benefits from a controllable thickening duty before compression | Can the transition and discharge controls handle both operating modes reliably? |
Available space is part of the selection, not an afterthought. The supplier should demonstrate the complete installed envelope, including feed distribution, gravity drainage, wedge compression, cake discharge, cleaning, controls and maintenance access. A configuration that achieves the target cake in a pilot trial but cannot be cleaned or maintained in the plant layout has not passed the selection test.
Compare Belt Presses with the Viable Alternatives
The 2024 Processes study identifies centrifuges and belt filter presses as preferred tools for large-scale sludge-dewatering projects, but its industrial comparison shows why a preferred category cannot replace a feed-specific decision. For the tested polymer sludge, a filter press outperformed the installed vacuum belt filter: cake solids were 35% rather than 19%, and the filter-press filtrate met local discharge regulations without additional treatment.
A conventional belt filter press offers continuous operation with gravity drainage and progressive compression. A vacuum belt filter adds suction-driven dewatering, so its performance depends on vacuum generation, belt porosity, belt tension, belt speed and washwater management. A filter press applies pressure through filter media in a batch process, creating discrete filter cycles and cake release from the plates. A plate-and-frame sludge filter press should therefore be evaluated on cycle time and filtrate handling as well as final cake solids.
| Decision factor | Belt filter press | Vacuum belt filter | Filter press |
|---|---|---|---|
| Dewatering mechanism | Gravity drainage followed by belt compression | Vacuum-assisted filtration with moving belt media | Pressure filtration through plates and filter media |
| Evidence in the 2024 case | Not the tested installed system | 19% solids cake | 35% solids cake; filtrate met local discharge regulations without additional treatment |
| Operating consideration | Continuous drainage, compression and cake release | Vacuum system, belt speed and tension, porosity and washwater | Batch cycles, plate operation, cake release and filtrate handling |
| Selection risk | Poor drainage or conditioning can limit compression performance | Insufficient cake dryness for the disposal route | Cycle time, polymer demand and batch logistics may affect economics |
| Required proof | Representative feed trial and operating-control data | Vacuum and belt performance trial | Cycle-time, filtrate and cake test on representative sludge |
Economics must also be route-specific. Processes reported savings of up to 50% annually and a payback period of 1.5 years for the filter-press retrofit, but those results belong to the documented industrial case. A textile plant comparison should include polymer, washwater, energy, labor, maintenance, cake transport and final disposal. Ask each supplier to state the assumptions behind any savings or payback claim, including feed characteristics, operating hours and disposal cost.
Build the Sizing and Supplier Acceptance Checklist
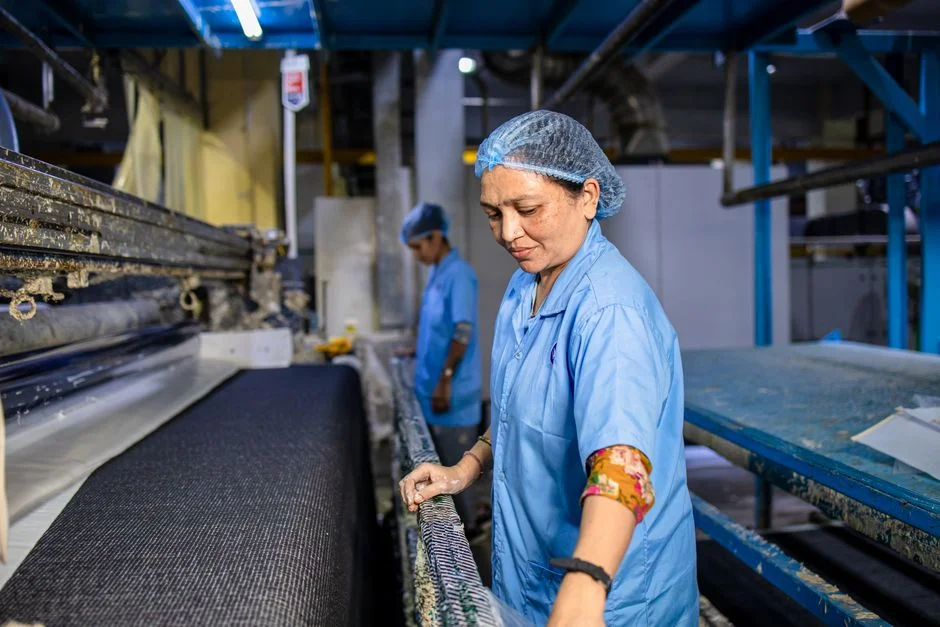
A supplier-ready package should define the feed, expected output, equipment envelope and test conditions before filtration area or belt dimensions are accepted. Processes states that belt filter press design must account for chemical conditioning, hydraulic and solids loading rates, and belt cleaning. The quotation should therefore describe a complete performance envelope rather than only list belt width and nominal capacity.
Request representative-sludge testing because filtration and compression depend on sludge type, conditioning, dewatering device and operating conditions, according to Processes in March 2024. The trial should use the proposed machine configuration, chemical recipe and representative operating range. The selected route then becomes a polymer dosing system design criteria issue as well as a dewatering-equipment issue.
| Procurement package | Minimum information or deliverable | Acceptance check |
|---|---|---|
| Feed envelope | Feed flow, dry-solids concentration, hydraulic loading rate, solids loading rate, operating hours and variability | Values are supported by representative-site data, not generic sludge assumptions |
| Output targets | Target cake solids, filtrate quality, solids capture and disposal route | Supplier demonstrates compliance with each stated target |
| Test basis | Representative sample, conditioning recipe, test duration and mass-balance method | Test protocol and calculation method are agreed before the order |
| Mechanical scope | Filtration area, belt width and length, drive power, frame and guarding | Dimensions fit the available space and service access |
| Auxiliary systems | Polymer preparation and feed, washwater, cake discharge, filtrate handling, controls and safety guarding | Interfaces, utilities and responsibilities are explicitly priced |
| Commissioning | Installation, training, trial run, performance test, spares and documentation | Acceptance procedure, instruments, witness attendance and defect remedy are documented |
For a filter-press fallback, require the supplier to state whether the offer is batch or continuous, the filtration area, cycle-time basis, plate and cloth arrangement, polymer-feed scope, washwater arrangement and control package. HydropureWater’s verified product catalog lists filtration areas from 1–500 m² and manual, hydraulic or fully automatic PLC-controlled operation. Those are supplier-published selection facts, not a guarantee that a particular area will meet a textile plant’s throughput or cake target.
Turn the matrix into contractual acceptance criteria. A practical sequence is: characterize the feed, run a representative trial, confirm conditioning, verify filtration-area and loading calculations, execute a site performance test, and accept only against agreed calculation methods. This sequence prevents a machine selected from dry-solids content alone from being accepted without evidence for solids capture, cake dryness, filtrate quality or stable operation.
Frequently Asked Questions
How much does a belt filter press for textile wastewater cost?
No supported textile-specific quotation is available in the supplied research, so a defensible price cannot be stated. Request a quotation based on feed flow, dry-solids concentration, hydraulic and solids loading rates, target cake solids, operating hours, required belt width and length, filtration area, polymer-feed scope, washwater, controls and installation conditions. Require polymer, washwater, labor, maintenance and disposal assumptions to be shown separately rather than accepting a single capacity-based price.
Which textile sludge condition should lead to a filter press instead?
Consider a filter press when representative testing shows that the belt route cannot reach the required cake solids or filtrate quality. The 2024 Processes case is relevant evidence: for the tested polymer sludge, a filter press produced 35% solids cake compared with 19% from the vacuum belt filter, and its filtrate met local discharge regulations without additional treatment. This is a case-specific result, not proof that all textile sludge should use a filter press; request equivalent testing before changing routes.
What feed data is required to size a belt filter press?
Provide representative dry-solids concentration, TSS, feed flow, hydraulic loading rate, solids loading rate, sludge origin and treatment stage, COD, pH, fiber content, variability, conditioning requirements, target cake solids and filtrate-quality limit. Dewater.com states that most applications require polymer addition before dewatering, and Processes identifies conditioning, hydraulic and solids loading rates and belt cleaning as key belt-press design requirements.
How should the buyer compare supplier performance guarantees?
Require every guarantee to use the same feed and calculation basis: conditioned and unconditioned feed characterization, polymer recipe, hydraulic and solids loading rates, operating hours, sampling method, cake-solids method, filtrate-quality method and solids-capture calculation. Ask the supplier to state whether the performance basis came from representative testing, a calculation or another project. Reject a comparison in which one supplier reports cake dryness while another reports only hydraulic capacity.