Start with the permit and process inventory
Fabricated metals plants near Marysville meet pretreatment limits by first confirming whether 40 CFR Part 433 applies, comparing the applicable PSES or PSNS standard with the current City of Marysville POTW local limits, and using the stricter limit for each parameter. The resulting treatment train generally uses equalization, oil removal, hexavalent-chromium reduction, cyanide oxidation, hydroxide precipitation, DAF or lamella clarification, final pH control and sludge handling. Equipment sizing should follow at least a full week of representative composite sampling because batch dumps can sharply change flow, pH and contaminant loads. Marysville also requires new sewer users to submit an Industrial User Survey Form and obtain discharge requirements from the city's Division of Wastewater.
Part 433 applicability depends on the plant’s actual operations, not its business description. A dry-stamping operation that sends parts to an outside finisher is generally outside the category, while a plant operating zinc, nickel or chromic-acid tanks is within the covered scope (HydropureWater, 2026). Document every plating, anodizing, hard-chrome, pickling and co-located covered metal-finishing operation before selecting equipment.
Existing sources are evaluated under PSES, while new sources are evaluated under PSNS; PSNS is the tighter categorical standard. The design target is nevertheless established parameter by parameter against Marysville’s current local-limit table. This approach is explained in the fabricated metals sewer-limit compliance guide.
| Parameter | Regulatory reference | Design record required |
|---|---|---|
| Cadmium, chromium, copper, lead, nickel, silver, zinc and total toxic organics | Applicable PSES or PSNS categorical standard | Standard, source status, local limit, stricter target and proposed control point |
| Oil and grease, total suspended solids and pH | Current Marysville POTW local limits, where applicable | Monitoring frequency, sample point and treatment outlet specification |
| Hexavalent chromium and cyanide | Categorical requirement plus plant process chemistry | Reduction or oxidation stage, reaction endpoint and failure-response interlock |
Marysville’s Industrial Pretreatment Program operates under Part II Section Y of NPDES Permit 4PE00002*DD, 40 CFR 403, Chapter 3745-3 of the Ohio Administrative Code and Chapter 6111 of the Ohio Revised Code (City of Marysville, 2026). The city also identifies sources, issues control documents and conducts compliance monitoring. New sanitary-sewer users must submit an Industrial User Survey Form, while industrial and commercial users should contact the Division of Wastewater at (937) 645-7344 for discharge limits.
Characterize the wastewater before sizing the system
A full week of representative composite sampling is necessary before finalizing equalization because a four-hour composite can miss a Friday-afternoon dump and undersize the basin (HydropureWater, 2026). Characterize flow and mass loading together; a low concentration does not establish that the treatment train has adequate hydraulic or chemical capacity.
Separate contributions from stamping, machining and drawing compounds, acid pickling, chromic-acid anodizing, hard chrome, conversion coating, grinding swarf, casting sand, floor drainage, line washdown and production rinsewater. Record whether each composite captured a tank dump, washdown or other batch release. That information determines whether equalization is merely a short-flow buffer or the central control unit for a variable batch-discharge stream.
| Source contribution | Principal concern to characterize | Information needed for sizing |
|---|---|---|
| Stamping, machining and drawing compounds | Free and emulsified oil | Oil concentration, flow contribution and emulsification characteristics |
| Acid pickling and rinsewater | Dissolved metals and low pH | Metal species, concentration, acidity and dump frequency |
| Chromic-acid anodizing and hard chrome | Hexavalent chromium | Cr(VI), total chromium, pH and flow during dump events |
| Grinding swarf, casting sand and conversion coating | Suspended solids | TSS, particle characteristics and solids contribution by stream |
| Floor drainage, line washdown and rinsewater | Dilution, variable flow and batch contamination | Continuous flow, dump volume, timing and contaminant contribution |
HydropureWater’s 2026 field ranges are screening information rather than substitute site data: oils at 50–500 mg/L, total dissolved metals at 5–200 mg/L, TSS at 100–1,000 mg/L and pH moving between 2 and 12 across batch dumps (HydropureWater, 2026). Calculate mass loading from measured flow and concentration. Do not size tanks or chemical systems from concentration alone, because the weekly flow profile determines equalization volume, instantaneous treatment demand and the frequency of chemical adjustments.
Match each contaminant to a dedicated control step
Each contaminant family requires a different control mechanism, and upstream failure carries into every downstream unit. Equalization buffers batch dumps and smooths downstream chemistry; HydropureWater’s 2026 design objective is pH 6–9 after equalization and a flow coefficient of variation below 0.5. Remove free and emulsified oils physically or by chemical breaking before the principal metals treatment sequence.
Reduce hexavalent chromium to trivalent chromium with sodium metabisulfite or ferrous sulfate at pH 2–3 and approximately 250–300 mV ORP. The precipitation stage then operates at pH 8.5–9.5, where trivalent chromium precipitates as Cr(OH)₃ while hexavalent chromium hydroxide would remain soluble (HydropureWater, 2026). Oxidize cyanide before metals precipitation because cyanide can resolubilize downstream metal precipitates.
Precipitate dissolved metals as hydroxides and remove the resulting floc by DAF or lamella clarification before final pH adjustment. Do not combine reduction, oxidation, oil removal and precipitation into one uncontrolled reaction stage. Each stage needs an outlet specification, monitoring point and defined failure response.
| Control stage | Required outlet condition | Principal failure mode | Protective response |
|---|---|---|---|
| Equalization | Smoothed flow and controlled pH | Oversized batch exceeds downstream hydraulic or chemical capacity | Track basin level and composite-sample discharge |
| Oil removal | Free and emulsified oil controlled before metals chemistry | Interference with floc formation or flotation | Diversion based on the selected oil-monitoring criterion |
| Chromium reduction | pH 2–3 and approximately 250–300 mV ORP | Incomplete reduction leaves chromium soluble | Stop feed and divert on out-of-range pH or ORP |
| Cyanide oxidation | Oxidation endpoint met before precipitation | Cyanide carries forward or redissolves precipitates | Interlock downstream precipitation on oxidation failure |
| Hydroxide precipitation | pH 8.5–9.5 and defined metal-removal performance | Precipitates redissolve or carry over | Verify pH, solids removal and downstream metal results |
| DAF or lamella separation | Defined TSS and floc-removal outlet specification | Floc breakthrough, fragile float or uneven sludge collection | High-TSS diversion and monitored solids removal |
A PLC-controlled automatic chemical dosing skid should meter reductant, oxidant, pH-adjustment chemicals and polymer against flow and treatment feedback. The process flow should retain clear boundaries between these chemical duties, with each feed assigned to a defined contaminant and monitored reaction endpoint.
Size equalization, solids separation and sludge handling
Equalization sizing must reflect the full-week composite record and measured mass-loading profile so batch dumps do not overwhelm downstream chemistry. Hydrodynamic volume, working storage and transfer capacity are separate procurement inputs; a tank selected only from average daily flow will not describe the plant’s actual batch response.
For DAF, require the supplier to state hydraulic surface loading, air-to-solids ratio and recycle assumptions. HydropureWater’s 2026 guidance identifies 4–20 m/h surface loading, 0.005–0.060 A/S with 0.02 as a typical design point, and recycle of 10–30% of forward flow. Increasing A/S can produce drier float but consumes more blower power and may break fragile floc. Increasing recycle can improve TSS removal while diluting chemistry and increasing equalization demand.
Compare DAF with lamella clarification using the actual wastewater and installation constraints. DAF is the starting point when the objective includes TSS, FOG, oil, grease or colloidal material; lamella clarification is attractive where compact inclined-plate separation, sludge recirculation and integrated flocculation fit the installation (HydropureWater, 2026). The industrial DAF system for metalworking wastewater proposal should disclose these operating assumptions rather than provide only a model and surface area.
| System element | Bid information required | Operating or commercial dependency |
|---|---|---|
| Equalization | Weekly flow and mass-loading basis, working volume and transfer arrangement | Batch-release frequency and collection-system response |
| DAF | Surface loading, A/S, recycle, floc condition and hydraulic capacity | Power use, chemical dilution and fragile floc |
| Lamella clarification | Clarifier area, plate configuration, flocculation and sludge withdrawal | Floc disturbance, carryover and uneven sludge collection |
| Sludge dewatering | Feed solids, selected dewatering method, cycle controls and residue destination | Chemical carryover, wet disposal and equipment blockage |
Evaluate sludge dewatering against the disposal contract rather than filter area alone. HydropureWater reports 2–5% dry solids leaving DAF, 25–35% after plate-and-frame dewatering and a belt-press ceiling around 22% for metal hydroxide sludge (HydropureWater, 2026). Hauler acceptance, leachate characteristics and destination requirements therefore affect the correct dewatering target.
Protect the sludge train from rags, wipes and tramp metal with upstream mechanical screening. HydropureWater identifies premature filter-press blinding as the principal failure associated with this debris (2026). A mechanical bar screen ahead of solids handling should appear in the protected flow route, and the metal hydroxide sludge filter press scope should include the required upstream protection.
Build controls that protect the discharge point
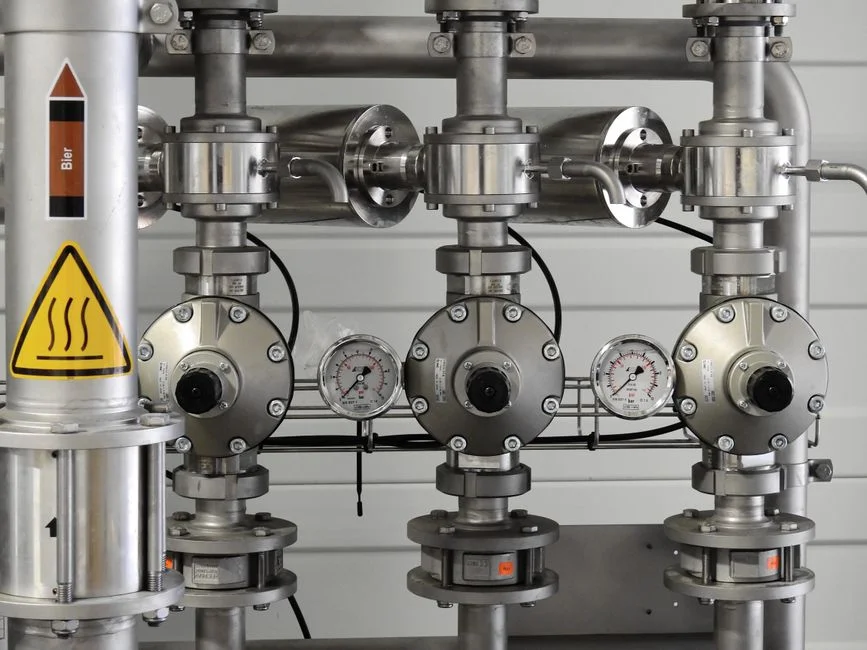
Batch wastewater requires feedforward chemical pacing combined with feedback from pH or ORP; fixed manual settings do not adequately control variable discharges (HydropureWater, 2026). Specify a PLC-controlled, skid-mounted system so interlocks can be bench-tested before shipment and operators can manage the treatment sequence through one interface. The high-performance wastewater chemical dosing controls guide provides a useful basis for reviewing those requirements.
- Document the four principal chemical duties: pH adjustment with NaOH or H₂SO₄, chromium reduction with sodium metabisulfite, cyanide destruction with NaOCl, and flocculation with anionic or cationic polymer.
- Require calibration columns and stroke-count totalizers on each metering pump so operators can verify chemical delivery.
- Specify automatic diversion to the equalization basin header for pH excursions, out-of-range ORP and high TSS.
- Require flow-paced feeds linked to equalized flow, with feedback corrections based on the controlled reaction endpoint.
- Include the control narrative, alarm list and emergency diversion in the compliance documentation rather than treating automation as an accessory.
The control case should link every alarm to an initiating condition, protective action and operator instruction. Include pH and ORP trends, chemical-use records, pump totals, equalization levels, TSS results, alarm events and sludge-disposal records in the operating record reviewed for compliance (HydropureWater, 2026).
Decide whether polishing is justified now or later
Most fabricated metals plants can meet sewer limits with the core treatment train and do not need a polishing step (HydropureWater, 2026). Add polishing only when the current POTW limit is tighter than PSNS, the plant establishes a reuse objective, or a new requirement creates a treatment target beyond the primary train.
For BOD/COD tightening or reuse, HydropureWater’s 2026 guidance describes a submerged PVDF MBR with filtration below 1 μm. For sub-ppm TDS or very tight metal targets, consider reverse osmosis with upstream multi-media filtration. The integrated MBR treatment system and reverse-osmosis treatment system should therefore be evaluated against a defined target rather than included as unspecified contingency equipment.
EPA’s 2026 PFAS rulemaking activity scoped to chrome-finishing facilities did not establish a current numerical PFAS limit for chrome finishers (HydropureWater, 2026). PFAS is not a numeric design basis in 2026. Where future requirements are plausible, reserve space, utilities, containment and control interfaces for a possible anion-exchange or granular activated carbon skid rather than installing an unrequired polishing system now.
Turn the permit basis into a procurement checklist
A defensible bid starts with the current Marysville local-limit table, the applicable PSES or PSNS standard, sewer-use authorization, discharge authorization and the plant’s process inventory. Until those documents are identified, an outlet-performance guarantee has no defined compliance basis.
| Procurement document | Question the buyer should require the bidder to answer | Acceptable supporting basis |
|---|---|---|
| Process flow and design envelope | Which parameter, standard or local limit does each control point address? | Parameter-by-parameter table tied to current permit documents |
| Equipment sizing | Which measured flow, mass-loading and wastewater properties determine the selected capacity? | Full-week composite dataset and stated sizing calculations |
| Controls | How are pH, ORP, flow and high-TSS upsets detected and contained? | Control narrative, alarm list and diversion sequence |
| Chemical consumption | What operating conditions drive reductant, oxidant, acid, base and polymer demand? | Documented calculation range and chemical assumptions |
| Sludge and cost scope | Where will residue go, and what is included in the quoted price? | Disposal basis plus itemized installed-cost exclusions |
Require the supplier to separate equipment cost from foundations, electrical work, chemical supply, commissioning, operator training, maintenance and sludge disposal. Ask which claims are calculated design values, which are guaranteed performance terms and which depend on site chemical consumption, sludge properties or operator practice.
Do not accept an outlet-performance guarantee until the current Marysville local-limit table, sewer-use authorization, discharge authorization and applicable categorical standard have been identified. For any comparison that includes biological treatment, the MBR versus conventional treatment for fabricated metals assessment should be tied to a defined reuse or tightening objective.
Frequently Asked Questions
Does a fabricated metals plant near Marysville always fall under 40 CFR Part 433?
No. A dry-stamping plant shipping parts to an outside finisher is generally outside Part 433, while a plant operating zinc, nickel or chromic-acid tanks is within the covered scope (HydropureWater, 2026). Document the actual operations, including any co-located covered metal-finishing activities, before selecting categorical assumptions.
Why should equalization be sized from at least one week of composite samples?
Plating shops produce batch dumps rather than steady flow. A four-hour composite can miss a Friday-afternoon dump and undersize the basin (HydropureWater, 2026). Use the resulting flow and mass-loading profile to establish working storage, transfer capacity and downstream hydraulic demand.
What should a supplier need before pricing a complete pretreatment system?
Request the current Marysville local-limit table, process inventory, full-week composite data, treatment objectives, chemical-consumption basis, solids-disposal method and required controls. Require a complete flow diagram, sizing calculations, alarm list, control narrative and itemized exclusions. These inputs establish whether the proposed equipment responds to the actual permit and wastewater rather than generic assumptions.
What determines the cost of a compliant fabricated metals pretreatment system?
The supplied research contains no defensible capital-cost quotation, so a price cannot be stated responsibly. Obtain current permit limits, wastewater characterization, flow and mass-loading data, chemical requirements, controls, site installation conditions and sludge-disposal terms. Then ask bidders to separate equipment from foundations, electrical work, chemicals, commissioning, training, maintenance and disposal costs.
Should the system include polishing and a PFAS treatment stage in 2026?
Most fabricated metals plants do not need polishing to meet the core sewer limits. Add MBR or reverse osmosis only for a defined reuse or tighter treatment objective (HydropureWater, 2026). No current numerical PFAS limit for chrome finishers was established by the cited 2026 rulemaking activity, so reserve space and utilities for possible future treatment rather than using PFAS as a present numeric design basis.