What Pretreatment Compliance Looks Like for a Waco Paper Mill in 2026
An "indirect discharger" sends wastewater to a publicly owned treatment works (POTW) instead of a receiving stream, and the federal Clean Water Act framework places the local POTW pretreatment program on top of any categorical standard (per EPA 40 CFR Part 430 framework). For a McLennan County paperboard, tissue, or recycled-fiber mill discharging to the Waco POTW, that means three layers of compliance stack: the federal effluent guideline under 40 CFR Part 430, the Texas Commission on Environmental Quality (TCEQ) delegation that authorizes the POTW's pretreatment program, and the local sewer-use ordinance the Waco POTW enforces. The mill that skips any layer ends up renegotiating its discharge permit under a consent order — that is the operating reality in 2026.
EPA promulgated the Pulp, Paper and Paperboard Effluent Guidelines in 1974 and 1977, amended them in 1982 and 1986, and issued a major toxic-pollutant amendment in 1998 (the "cluster rules") (per EPA 40 CFR Part 430). The category is split into subparts, and the two most likely to apply to a Waco-area indirect discharger are Subpart D (unbleached kraft — linerboard and bag paper) and Subpart J (secondary fiber from wastepaper, including tissue and paperboard from non-deinking furnish) (per EPA 40 CFR Part 430). A bleached mill would land in Subpart B (bleached papergrade kraft and soda), which brings adsorbable organic halide (AOX) and chlorinated compound limits into scope. The TCEQ authorizes the Waco POTW to run the local pretreatment program under the federal delegation rules in 40 CFR Part 403; specific permit numbers and ordinance citations vary by facility and should be pulled from the mill's own control authority correspondence.
The Pollutants a Paper Mill Has to Control Before the Sewer
The parameters that drive the equipment train are BOD, COD, TSS, color, toxicity, pH, temperature, and — for bleached subcategories — AOX (per Hubbe et al. 2016 industry review). The BOD/COD ratio is the single most useful design number, because it sets the fraction of organics that are biologically degradable: a ratio above ~0.4 supports a conventional activated-sludge train, while a ratio below 0.3 signals the need for an advanced oxidation or membrane polishing step (per Hubbe et al. 2016 industry review, citing McCubbin and Folke 1993). Chemical pulping streams have been documented to carry more than 40% of their total organic load as poorly biodegradable material, which is exactly why a biological-only train undershoots POTW color and COD limits without a polishing stage (per Hubbe et al. 2016 industry review, citing Dahlman et al. 1995).
AOX tracks chlorine consumption in the bleach plant almost linearly, and the industry has cut AOX emissions by more than 80% since 1990 through oxygen delignification and ECF/TCF substitution (per Hubbe et al. 2016 industry review, citing Savant et al. 2006 and Fiere et al. 2003). That number matters because an unbleached or secondary-fiber mill in McLennan County is generally not subject to numeric AOX limits at all, but a bleached line that ships effluent to the Waco POTW will see AOX flagged in the local surcharge schedule. The other load that gets miscategorized is "fibre + filler + stickies" — the same suspended solids that drive POTW TSS surcharges are the same furnish a DAF or save-all can recover upstream and feed back into the product stream, which turns a compliance cost into a yield win.
The 2026 Treatment Train: From DAF to Discharge
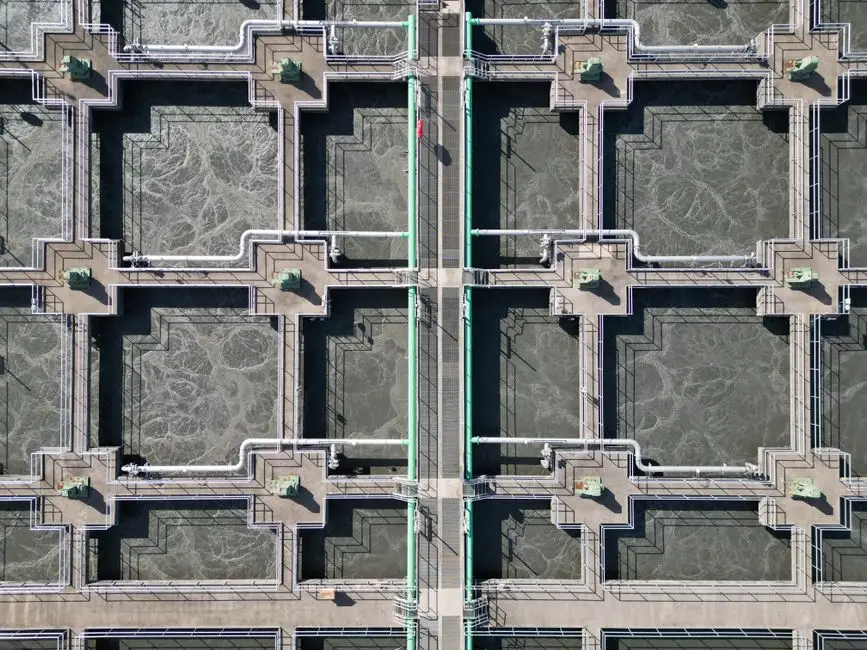
A 2026-vintage treatment train for a Waco-area indirect discharger runs in five stages, and skipping any one of them shows up as a surcharge or a violation on the next POTW compliance report.
- Fibre and filler recovery (DAF or filtration save-all). A mill-duty DAF skid or a save-all filter recovers reusable furnish from white water and cuts TSS loading to the sewer — both a yield and an environmental win. Per the Hubbe et al. (2016) review, upstream DAF and kidney systems materially reduce both pollutant load and effluent volume, which cascades into a smaller, cheaper biological stage downstream.
- Equalization. A surge tank sized to 8–24 hours of average flow smooths pH, flow, and temperature swings from pulping, broke handling, and paper-machine upsets. Thermal discharge violations are a routine POTW finding, and equalization is the cheapest way to keep mixed-sewer temperatures inside the local limit (typically ≤40 °C / 104 °F at the POTW sample point).
- Biological stage. Conventional activated sludge is the long-standing default; moving-bed biofilm reactor (MBR/MBBR) and membrane bioreactor (MBR) are gaining share for higher mixed-liquor suspended solids and tighter effluent targets (per Hubbe et al. 2016 industry review). For a 10–200 m³/h Waco-area mill, a skid-mounted or containerized biological package keeps civil work to a foundation pad and interconnecting piping.
- Polishing and chemical dosing. A PLC-controlled coagulant and pH dosing skid followed by a DAF or lamella clarifier drops residual TSS, color, and any residual AOX to sewer-ordinance levels. Mills that want reuse-grade water on the back end typically add a PVDF ultrafiltration polish after the biological stage.
- Sludge dewatering. A plate-and-frame sludge filter press drops dewatered cake solids to 30–40% dry solids, which keeps hauling and landfill disposal cost down and meets most POTW sludge-acceptance thresholds.
The flow direction is DAF → EQ → biological → chemical polish → discharge, with UF as an optional reuse branch off the biological effluent and a plate press on the combined sludge line.
Parameter Table: Influent vs. POTW Limit vs. Post-Stage Effluent
The table below uses typical ranges drawn from P&P industry reviews and commonly adopted POTW local sewer limits; confirm every number against the Waco POTW sewer-use ordinance and your own control-authority correspondence before specifying equipment (per Hubbe et al. 2016 industry review, and standard POTW pretreatment limits for industrial users).
| Parameter | Typical P&P influent | Common POTW local limit (illustrative) | After DAF / primary | After biological | After chemical / membrane polish |
|---|---|---|---|---|---|
| BOD5 (mg/L) | 1,500–4,000 | 250–500 (daily max) | 800–2,000 | 20–60 | < 20 |
| COD (mg/L) | 3,000–10,000 | 600–1,000 | 1,800–5,000 | 150–400 | < 100 |
| TSS (mg/L) | 1,000–4,000 | 200–450 | 200–600 | 20–60 | < 10 |
| Color (Pt-Co) | 1,500–5,000 | 300–500 (where listed) | 1,000–3,000 | 300–800 | < 100 (with oxidation) |
| pH (s.u.) | 4–10 | 5.0–10.5 (instantaneous) | 6–9 (after EQ) | 6.5–8.5 | 6.5–8.5 |
| Temperature (°C) | 25–55 | ≤ 40 (at sample point) | 25–45 (after EQ) | 20–35 | 20–30 |
| AOX (kg/ADt or mg/L) | 0.5–3.0 (bleached only) | 0.10–0.30 (where regulated) | 0.3–2.0 | 0.1–0.5 | < 0.1 (with UF/polish) |
AOX only applies to bleached subcategories (B, C) under 40 CFR Part 430; unbleached kraft (Subpart D) and secondary fiber (Subpart J) mills are not subject to numeric AOX limits, though color and COD/TSS still drive local sewer surcharges (per EPA 40 CFR Part 430, Subpart listing). Color is the parameter that most often gets flagged in a local ordinance even when it is not in the federal numeric table, which is what justifies keeping an oxidation or membrane polish in the train.
Choosing the Right Skid for Each Step in 2026
For a 10–200 m³/h McLennan County site, the selection matrix is driven less by absolute technology choice and more by what the upstream fibre-recovery step already gives you. Upstream DAF and kidney operations reduce both pollutant load and effluent volume, which directly shrinks the size and cost of the biological stage downstream (per Hubbe et al. 2016 industry review).
| Train slot | Option A (capex-favoured) | Option B (reuse-favoured) | Option C (capex ceiling) | Selection signal |
|---|---|---|---|---|
| Primary TSS / furnish recovery | DAF skid (mill-duty) | Lamella clarifier | Sedimentation tank (high-rate) | Filler/fibre resale value > $50/ADt → DAF wins on yield payback |
| Biological | Packaged activated sludge | MBBR (moving-bed biofilm reactor) | Containerized MBR (membrane bioreactor) | Need reuse-quality effluent → MBR; high variability / low operator headcount → MBBR; legacy site with basin volume → activated sludge |
| Sludge dewatering | Plate-and-frame filter press | Belt press | Decanter centrifuge | Cake dryness target > 30% DS → plate press; high volume / low dryness OK → belt press |
| Polishing | Coagulant dosing + DAF | UF (PVDF) | AOP + DAF | Color and AOX limits → AOP or UF; TSS only → coagulant + DAF |
For mills that want water reuse on top of compliance, a containerized MBR system delivers a sub-1 μm effluent (per product spec) and runs roughly 60% smaller than a conventional activated-sludge basin at the same load. Pair it with an MBR membrane module sized for the design flux, and a high-efficiency sedimentation tank upstream to keep the membrane from fouling on TSS spikes. A working walk-through of MBR sizing and hydraulics is in the MBR process explainer; a head-to-head of the DAF/clarifier choice for a paper mill is in the DAF vs. clarifier decision guide for a paper mill; and the civil-work trade-off between packaged and cast-in-place biological trains is in the packaged vs. cast-in-place STP comparison for a paper mill.
What a 2026 Retrofit Typically Costs and How to Pitch It
Capex ordering is consistent across the industry: DAF and chemical dosing are the lowest-cost slots per cubic metre treated, the biological stage is the single largest line item, and MBR is the most expensive biological option but pays back fastest where reuse water displaces freshwater intake. Three numbers drive the business case more than any spec sheet: the furnish recovery rate from the upstream DAF (typically 85–95% of fibre and filler in the white-water sidestream), the avoided POTW surcharge on TSS and BOD, and the avoided freshwater cost from any reuse loop the MBR or UF stage enables. The industry has cut water use by approximately 95% per tonne of paper over the last 30 years (per Hubbe et al. 2016 industry review, citing Blanco et al. 2004), which is the benchmark to anchor a 2026 reuse-oriented upgrade against — not just a compliance-driven one.
Most packaged 2026 retrofits install in a 4–10 week window per skid, because the DAF, dosing, biological, MBR, and plate-press skids arrive factory-tested and skid-mounted, with the only major site work being the equalization basin, interconnecting piping, and the sludge hopper tie-in. For a Waco-area mill with a 50–150 m³/h design flow, the realistic budget conversation is staged: DAF and chemical dosing first (fastest ROI), biological upgrade or MBR retrofit second (capex ceiling), and a polishing or UF reuse loop third (payback through freshwater displacement).
Frequently Asked Questions
Does 40 CFR Part 430 apply to a paper mill that discharges to the Waco POTW?
Yes. EPA promulgated the Pulp, Paper and Paperboard Effluent Guidelines under 40 CFR Part 430 in 1974 and 1977, with major toxic-pollutant amendments in 1998, and the categorical limits are incorporated into POTW pretreatment programs for indirect dischargers (per EPA 40 CFR Part 430). The specific limits depend on which subpart — D (unbleached kraft linerboard) or J (secondary fiber) most commonly applies in McLennan County.
What pollutants does a Waco-area paper mill typically have to control?
The headline parameters are BOD, COD, TSS, color, toxicity, pH, and temperature; bleached mills in Subpart B or C also have to control AOX (per EPA 40 CFR Part 430 subcategory list). AOX emissions across the industry have dropped over 80% since 1990 due to oxygen delignification and ECF/TCF substitution (per Hubbe et al. 2016 industry review).
Is an MBR worth the higher capex for a small paper mill in Waco?
For a 10–200 m³/h indirect discharger, an MBR is the right call when reuse-grade effluent (< 1 μm) is needed to offset freshwater intake, or when site footprint is constrained. Per the product spec, the containerized MBR footprint runs roughly 60% smaller than a comparable conventional activated-sludge basin, which typically justifies the capex premium within the reuse-loop payback window (per HydropureWater product specification, 2026).
For site-specific sizing, influent characterization, and a CAPEX/OPEX model tied to the Waco POTW sewer-use ordinance, a HydropureWater engineer can run a mass-balance and a skid selection against your mill's monthly compliance data.