Why tanneries need a filter press on the sludge line
Tannery effluent carries dissolved trivalent chromium together with high COD and BOD from fats, proteins and hide fragments; raising the pH to about 8.5 precipitates the chrome as chromium hydroxide, but the resulting sludge is a handling and disposal problem before it is a treatment problem. The settled or DAF-thickened chrome sludge leaves clarification at roughly 85–95% water by weight, and pumping that volume to landfill is uneconomic on hauling alone and often non-compliant against regional hazardous-waste thresholds (Senjie, 2026-07).
The mechanical dewatering step is therefore not optional. A filter press compacts the chrome precipitate into a transportable cake, which is why the filter press is the most common dewatering device for chrome sludge — it is chosen over belt press or centrifuge for cake dryness and chrome capture rate (Senjie, 2026-07). Dewatered cake at 30–45% solids (≈55–70% moisture) is the realistic operating window for a chamber press; adding a membrane (diaphragm) squeeze pushes solids toward the upper end of that range and shortens cycle time (Senjie, 2026-07).
Process flow: from chrome precipitation to filter press feed
The filter press only does its job if the upstream chemistry and thickening are right. Dissolved Cr3+ is converted to a filterable solid by raising the effluent pH to about 8.5, which precipitates chromium hydroxide; under-precipitation leaves chrome in the filtrate and defeats the purpose of dewatering, while over-precipitation wastes caustic and bloats cake volume (Senjie, 2026-07). The precipitated floc is then thickened in a settling tank or DAF unit upstream of the press — good primary clarification is the difference between a clean cake and a cloth-blinding mess downstream (Senjie, 2026-07).
Thickened sludge is pumped to the press at a feed pressure of roughly 0.6–1.0 MPa; underfeeding the press lengthens cycle time, overfeeding risks cloth blow-out (Senjie, 2026-07). Polymer conditioning is standard practice in municipal biosolids dewatering, where the US EPA reports polymer doses of 1–10 g/kg depending on sludge type, with raw primary sludge at 1–5 g/kg and raw WAS or raw primary+WAS at 1–10 g/kg (EPA 832-F-00-057, September 2000). For tannery chrome floc, the published EPA numbers are not directly applicable — the specific polymer and dose for chrome sludge must be bench-tested on site, and the buyer should request vendor-supported jar tests before specifying conditioning chemistry.
Chamber vs plate-and-frame vs membrane press: which one fits a tannery
Three press geometries are routinely offered for tannery duty, and the choice is driven by cake dryness target, automation level and whether chrome recovery is in scope. Chamber presses are the workhorse for small and mid-size tanneries — lower capex, simple operation, and cake in the 30–45% solids window (Senjie, 2026-07). Membrane (diaphragm) presses add a squeeze step at the end of the cycle; they push cake solids toward the higher end of the 30–45% range and shorten cycle time, which matters when hauling cost is high or chrome is being recovered (Senjie, 2026-07). Plate-and-frame presses are typically used where very dry cake or thorough cake washing is needed; they are less common for routine tannery duty but appear in chrome-recovery loops that need a wash step (Senjie, 2026-07).
On capex, a membrane press typically carries a roughly 15–30% capital premium over an equal-area chamber press, but the drier cake cuts hauling weight and concentrates the feed for chrome regeneration (Senjie, 2026-07). Manually operated chamber presses for smaller tanneries sit at the lower end of the industrial filter press price range; PLC-controlled membrane presses with automatic plate shifting sit at the higher end and dominate at large tannery estates in South Asia and Brazil running multiple shifts (Senjie, 2026-07). For a head-to-head procurement view, the comparison table below summarises the trade-offs.
| Parameter | Chamber press | Plate-and-frame | Membrane (diaphragm) press |
|---|---|---|---|
| Typical cake solids, chrome sludge | 30–45% | 30–45% (with possible wash step) | Upper end of 30–45% range |
| Capex vs equal-area chamber | Baseline | Comparable to chamber | ≈15–30% higher |
| Cycle time | Longer | Longer | Shorter (squeeze step) |
| Chrome-recovery readiness | Possible | Possible (wash step helps) | Best — concentrated feed to redissolution |
| Typical fit | Smaller tanneries, lower daily wastewater volume | Where cake washing is required | Larger clusters, high disposal cost, chrome recovery focus |
For a specification of the chamber/frame architecture that underlies all three geometries, see the plate and frame filter press reference design.
Filter cloth and plates for tannery duty
The most common operating failure on a tannery filter press is premature cloth blinding, and the root cause is the floc itself. Chromium hydroxide is fine and gelatinous and blinds coarse cloth quickly, which is why a fine-micron woven polypropylene (PP) monofilament cloth is the standard cloth choice for chrome sludge duty (Senjie, 2026-07). Tannery process water also swings across extreme pH between the tanning and liming stages, and PP monofilament tolerates this pH swing better than natural fibres (Senjie, 2026-07).
Expect cloth life to run shorter than in mineral dewatering because of the fine, sticky nature of chrome floc; plan on periodic acid or alkaline cloth washing to hold flow rate between full replacements (Senjie, 2026-07). On the plate side, specify acid-resistant PP plates and match plate seal dimensions to the cloth supplied by the same manufacturer — mismatched seals create leak paths that defeat the press and contaminate the filtrate (Senjie, 2026-07). Where pH swings are extreme or chrome-rich filtrate is being recycled, the cloth-and-plate combination should be quoted as a matched set rather than as separate line items.
Sizing the press from daily wastewater flow and hide throughput
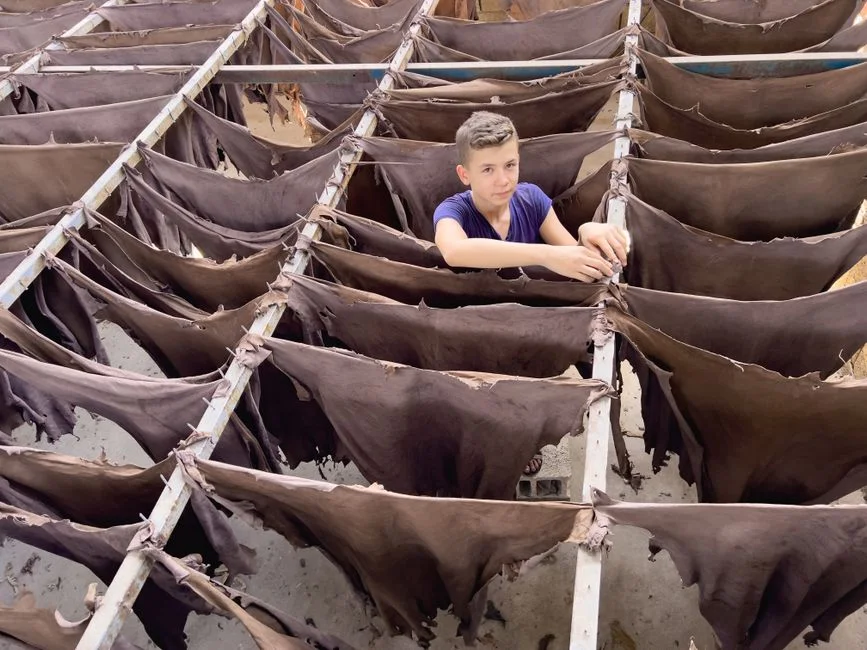
Sizing the press against hide throughput alone is a common mistake. The vendor actually needs average and peak daily wastewater flow, settled-sludge yield (kg DS/day or % solids to the press), shift pattern, and the target cake dryness — chrome load and the upstream hair-saving, liming and pickling process choice change the sludge yield per hide significantly, and a hide count without a flow figure is not a sizing input (Senjie, 2026-07). The standard sizing logic is to use the cake dryness target (for example 35% vs 45% solids) and the feed solids (typically 1–5% from a well-run DAF) to compute dry solids per cycle, then back-calculate chamber volume and plate count (Senjie, 2026-07).
For a sanity check on achievable dryness, the US EPA reports the following belt-press cake-solids ranges for biosolids (EPA 832-F-00-057, September 2000):
| Sludge type (biosolids, EPA data) | Total feed solids (%) | Polymer (g/kg) | Total cake solids (%) |
|---|---|---|---|
| Raw primary | 3–10 | 1–5 | 28–44 |
| Raw WAS | 0.5–4 | 1–10 | 20–35 |
| Raw primary + WAS | 3–6 | 1–10 | 20–35 |
| Anaerobically digested primary + WAS | 3–9 | 2–8 | 18–44 |
These biosolids ranges are useful as a benchmark — tannery chrome sludge is not biosolids and typically dewatersto a similar 30–45% solids window, with membrane squeeze pushing toward the upper end (Senjie, 2026-07; EPA 832-F-00-057, September 2000). The takeaway for a buyer is to size the press against the dry-solids mass the upstream plant actually produces, then confirm the cake-solids assumption with a pilot or a reference plant on similar chrome feed.
Chrome recovery from the cake: closing the loop
The filter press is not the end of the chrome story — the cake is a feedstock for regenerating tanning liquor. In many tanneries the chromium-rich cake is redissolved with sulfuric acid to regenerate a basic chromium sulfate tanning liquor, which is reused in the tanning drum; this reduces both raw chemical purchase cost and the volume of hazardous waste sent to landfill (Senjie, 2026-07). The route only works if the cake is reasonably pure chromium hydroxide, which means fats and hide fragments must have been removed upstream by screening and primary clarification rather than co-precipitated into the cake (Senjie, 2026-07).
A membrane press pays back faster in a chrome-recovery loop because the redissolution tank sees a higher solids feed and the recovery reaction runs hotter and faster (Senjie, 2026-07). Where chrome recovery is not practiced, the dewatered cake still has downstream value: Hashem et al. (Environ Sci Pollut Res Int, 2026) report that 4% filter-press tannery effluent sludge (FPTES) in fired bricks achieved 15.9 MPa compressive strength — meeting ASTM and BDS 'Category A' brick standards — with 14.7% water absorption, 2.3% shrinkage, 9.8% weight loss and 1.8 g/cm³ density, and the NEN 7345 leachate heavy metals were below permissible limits; the same study recorded a saving of USD 0.012/brick and a 25.8% reduction in energy consumption per brick (Hashem et al., Environ Sci Pollut Res Int, 2026).
Cost, compliance and what to send the vendor
Filter press price is driven by plate size, plate count and automation level rather than the tannery application itself, and a quotation should be requested against the actual daily flow and settled-sludge yield, not hide throughput alone (Senjie, 2026-07). For context on mechanical dewatering economics, the US EPA reports belt-press capital costs of USD 47,500–115,000 for 0.5–1.5 m belt units, overall O&M of USD 80–200 per dry ton of solids, and polymer costs of USD 2.65–91.15 per million gallons (averaging USD 24.38) — a filter press typically carries higher capital cost than a belt press but produces a drier cake, so the comparison must be run on whole-of-life hauling and disposal cost rather than capex alone (EPA 832-F-00-057, September 2000).
On compliance, cake that fails regional hazardous-waste thresholds cannot be landfilled; the buyer should confirm the disposal route against the local framework — Bangladesh DoE, India CPCB, Brazil CONAMA 430/2011 and EU IED Annex I all set chrome limits on residues and leachates, and the cake dryness target must be set against the route the cake will actually take. The RFQ checklist for the vendor should therefore include: feed flow (m³/day), feed solids (%), target cake solids (%), peak shift, available floor area, power supply, cloth material preference (PP monofilament), and whether chrome recovery is in scope. For pH and polymer control on the conditioning side, an automatic chemical dosing for pH and polymer control system should be specified alongside the press. For cross-process comparison points, a filter press for distillery wastewater guide and a filter press for winery wastewater sizing guide cover adjacent duty, while a DAF sizing guide for dyeing effluent addresses the same upstream thickening step used here.
Frequently Asked Questions
At what pH should chrome be precipitated before the press?
Roughly pH 8.5. That is the operating point that minimises chromium solubility and converts dissolved Cr3+ into a filterable chromium hydroxide (Senjie, 2026-07).
What cake dryness can a tannery filter press realistically achieve, and what does that mean for hauling and disposal budget?
30–45% solids (≈55–70% moisture) for a chamber press; membrane squeeze pushes toward the higher end of that range (Senjie, 2026-07). Because hauling cost scales with water mass, a buyer should ask the vendor for a per-cycle wet-cake weight at the quoted cake dryness and multiply by the daily cycle count — the capex premium for a membrane press is recovered through lower tonnage hauled, but only when the disposal route charges by mass.
Chamber or membrane press for a mid-size tannery, and how do I compare supplier quotes?
Chamber for lower capex and simple operation; membrane if chrome recovery is in scope or landfill cost is high — expect a roughly 15–30% capital premium for equal plate area (Senjie, 2026-07). When comparing supplier quotes, normalise on plate area (m²), chamber volume, cake solids guarantee and cloth specification; a low headline price on a smaller plate area is not equivalent to a higher price on a properly sized unit.
Is tannery filter-press cake reusable, or is it a hazardous waste?
Yes — redissolved cake can regenerate basic chromium sulfate tanning liquor, and 4% FPTES in fired bricks met ASTM/BDS 'Category A' strength (15.9 MPa) with NEN 7345 leachate heavy metals below permissible limits, delivering USD 0.012/brick saving and 25.8% lower energy per brick (Hashem et al., Environ Sci Pollut Res Int, 2026; Senjie, 2026-07). Whether reuse or disposal applies depends on the local hazardous-waste framework (Bangladesh DoE, India CPCB, Brazil CONAMA 430/2011, EU IED Annex I), and the cake dryness target should be set against the route the cake will actually take.