What a UASB Reactor Does and Where It Fits
A UASB (Upflow Anaerobic Sludge Blanket) reactor is a single-vessel, upflow anaerobic system that treats wastewater by passing it upward through a dense bed of self-immobilised granular sludge; hydrolysis, acidogenesis, acetogenesis and methanogenesis convert 80–95% of influent COD into biogas, with the reactor typically delivering 4–15 kg COD/m³/day at hydraulic retention times of 6–14 hours and yielding roughly 0.35 m³ of biogas per kg of COD removed (source: blog.anaerobic-digestion.com UASB design reference). Unlike hybrid anaerobic filters or fluidised-bed systems, the UASB needs no carrier media and no mechanical mixing; the rising flow, the buoyancy of the biogas bubbles, and the settleability of the granules do the work.
The technology fits upstream of a polishing step in any treatment train handling high-strength biodegradable wastewater — breweries, distilleries, dairy, pulp and paper, sugar, starch, palm oil, and pharma all sit in the typical feed envelope, generally with influent COD above 1,500 mg/L. Because the system is anaerobic, it does not oxidise ammonia, strip phosphorus, or kill pathogens. An MBR polishing step for UASB effluent — or an aerated lagoon, constructed wetland, or moving-bed biofilm reactor — is mandatory to hit a discharge consent. Position the UASB as the primary workhorse that does the COD reduction and biogas generation, then size the downstream step to deal with the residual COD, nutrients, and solids.
The Upflow Reactor Layout, From Influent Pipe to Effluent Weir
Influent enters the bottom of the reactor through a distribution grid — typically inlet points spaced 2–3 m apart in full-scale vessels — to prevent channelling and short-circuiting through the sludge bed (source: blog.anaerobic-digestion.com UASB design reference). For acid or H₂S-bearing industrial streams, designers specify acid-resistant stainless steel, HDPE, or FRP for the laterals, with velocity-reducing features (orifices, splash plates) to protect the granules from jet erosion. A poorly designed distributor is the most common cause of dead zones and localised overloading in real installations.
As the flow rises it first passes through the sludge bed zone — a compact layer of 1–3 mm granules with biomass concentrations above 40 g/L MLSS, occupying roughly the lower third of the reactor. Above that sits the sludge blanket zone, a more diffuse, partly fluidised layer where biogas bubbles entrain particles; this zone buffers hydraulic and organic surges and keeps the bed from compacting. Higher in the vessel, the three-phase separator (gas–solids–liquid) takes over: inverted V-baffles deflect rising gas into a collection dome, deflector plates stop biomass from spilling into the launder, and a quiescent settling zone lets detached granules fall back into the bed rather than leaving with the effluent. Treated water then spills over an effluent weir or launder, while biogas exits through the dome above the separator for moisture removal, H₂S scrubbing, and onward use.
How Granular Sludge Converts COD to Biogas
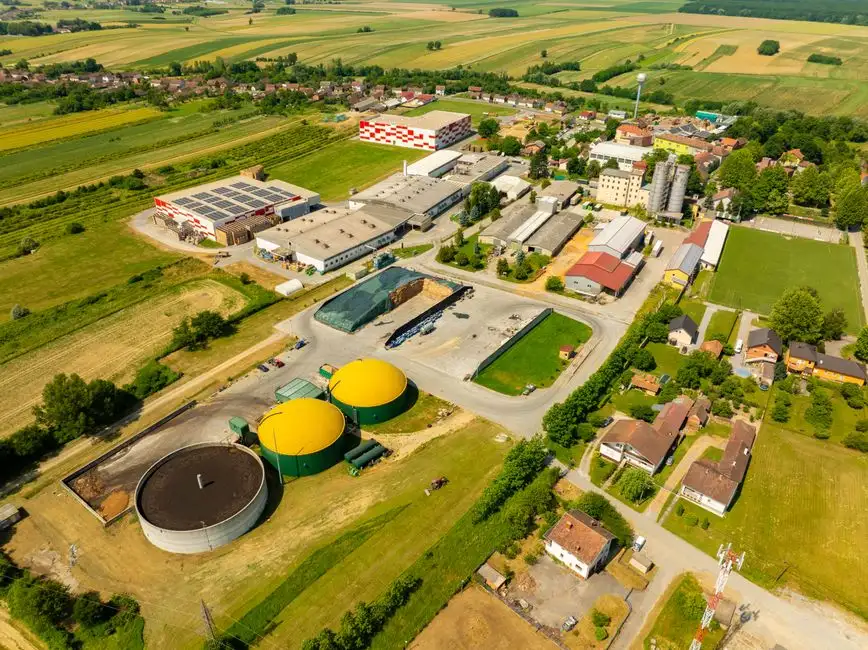
Each granule is a stratified microbial consortium. The outer layers house fast-growing fermentative bacteria that hydrolyse complex organics — carbohydrates, proteins, lipids — into volatile fatty acids (VFAs). Those VFAs diffuse inward, where slower-growing acetogens and methanogens convert them to acetate and then to methane and CO₂ (source: blog.anaerobic-digestion.com UASB design reference). This layered architecture is the reason granules tolerate substrates that would wash out a flocculant sludge: the sensitive methanogens sit in a low-inhibitor interior, shielded by the outer fermentative shell.
Specific methanogenic activity in mature granules routinely exceeds 1 g COD/g VSS/day — several times higher than floc-based anaerobic digesters, which is the fundamental reason the reactor can be so small. The granules themselves form through hydraulic selection: light, dispersed biomass washes out with the effluent, while dense, well-settling aggregates are retained and grow. The same mechanism that builds the granules, however, can also destroy them. Operate outside the design envelope — low pH, sudden temperature drop, excess fats or proteins, toxic shocks — and the granule matrix disintegrates; the earliest warning signs are rising effluent VFA, falling alkalinity, and a steady drop in COD removal (source: blog.anaerobic-digestion.com UASB design reference, 2010 Aiyuk et al. domestic-UASB data).
Key Design and Operating Parameters
The table below consolidates the operating envelope a designer or plant engineer can lift into a process datasheet. Numbers are taken from established UASB reference material (source: blog.anaerobic-digestion.com UASB design reference) and the 2010 Aiyuk et al. domestic-UASB study (source: doi.org/10.7763/ijesd.2010.v1.76).
| Parameter | Industrial UASB | Municipal / Domestic UASB | What it controls |
|---|---|---|---|
| HRT | 6–12 h | 10–14 h | Reactor volume; treatment completeness |
| OLR | 4–15 kg COD/m³/day | 1–3 kg COD/m³/day | Footprint vs. VFA risk |
| Upflow velocity | 0.5–1.5 m/h (up to 3 m/h peak) | 0.5–1.0 m/h | Sludge blanket expansion, washout risk |
| Reactor height | 4.5–7 m | 3–5 m | Gas–liquid–solid separation |
| H/D ratio | 3:1 to 5:1 | 3:1 to 4:1 | Hydraulic pattern, capex |
| Granule size | 1–3 mm | 0.5–2 mm | Activity, settling velocity |
| Biogas yield | ~0.35 m³/kg COD removed | ~0.30–0.35 m³/kg COD removed | Energy recovery sizing |
| Temperature | 30–37 °C (mesophilic) | Ambient (often <20 °C) | Methanogenic rate |
| pH | 6.8–7.4 | 6.8–7.4 | Granule integrity, VFA/alkalinity balance |
Push the OLR higher and reactor volume drops, but VFA risk rises sharply; extend the HRT and the system becomes more robust at the cost of capex. Below roughly 20 °C, methanogenic rates fall by a factor that the IWA hybrid UASB-filter study flagged as the reason unheated UASB reactors need a downstream filter stage to hit effluent targets in cold climates (source: IWA Publishing, doi.org/10.2166/wst.2004.0865). On the feed side, suspended solids should be low, macro/micronutrients balanced, and alkalinity sufficient to hold pH in the 6.8–7.4 window; fats and proteins need pre-treatment or co-digestion. A cautionary data point: Aiyuk et al. (2010) showed a domestic UASB fed raw sewage at 522 mg/L CODt still removed 80% of the COD, but suspended solids built up to ~70% of the influent COD, forcing sludge discharge roughly every 100 days — a clear signal that pre-screening is essential whenever SS is high (source: doi.org/10.7763/ijesd.2010.v1.76).
Three-Phase Separator and Biogas Handling
The three-phase separator is the single most failure-prone internal component of a UASB. It combines inverted V-baffles, a gas collection dome, deflector plates, and a quiescent settling zone; modern designs (e.g. the BIOPAQ® tilted-plate separator) boost gas-capture efficiency and reduce washout at higher loadings (source: blog.anaerobic-digestion.com UASB design reference). Get the geometry wrong and granules escape with the effluent — biomass inventory collapses, COD removal falls, and recovery takes months.
Biogas composition is typically 60–75% CH₄ and 25–40% CO₂, with water vapour and H₂S. Size the gas line for peak theoretical production (~0.35 m³/kg COD removed) plus a 20–30% safety factor to absorb surges. H₂S aggressively corrodes carbon-steel pipe, so specify stainless, HDPE, or FRP for the gas train and install an H₂S scrubber. The gas can be flared, burned in a boiler, or fed to a CHP unit; the waste heat from a CHP can be recovered through a heat exchanger to keep the reactor in the mesophilic 30–37 °C window, materially improving methane yield and stability (source: sswm.info UASB factsheet).
UASB vs Aerobic Activated Sludge: Working Principle Compared
The two technologies solve the same problem — COD reduction — through opposite metabolic pathways. The comparison below uses the numbers a procurement team will ask for, drawn from the same UASB reference material and from standard aerobic design ranges.
| Criterion | UASB (anaerobic) | Conventional Activated Sludge (aerobic) |
|---|---|---|
| COD removal | 80–95% (single stage) | 85–95% (with clarifier) |
| Energy use | Low; no aeration. Roughly 60–80% lower electricity than activated sludge | High; aeration is the dominant OPEX item |
| Sludge yield | ~0.05–0.10 kg VSS/kg COD | ~0.40 kg VSS/kg COD |
| Footprint | Compact; >40 g/L biomass, no clarifier | Large; aeration basin + secondary clarifier |
| Biogas byproduct | Yes (~0.35 m³/kg COD removed) | None |
| Nutrient (N/P) removal | Negligible — polishing step required | Partial nitrification possible; P needs chemical or EBPR step |
| Capex direction | Lower civil/structural capex; higher instrumentation | Higher civil/structural capex; standard equipment |
| Opex direction | Lower energy, lower sludge disposal cost | Higher energy and sludge disposal cost |
The economic argument is dominated by the aeration saving: a 60–80% electricity reduction against activated sludge, plus a usable biogas stream. The trade-off is that UASB alone does not remove nitrogen, phosphorus, pathogens, or recalcitrant COD; a polishing step — typically an MBR polishing step for UASB effluent — is non-negotiable for any plant with a discharge consent.
Start-Up, Common Upsets and How to Read Them
Start-up takes several months. Where possible, seed the reactor with granular sludge from a mature installation; otherwise, acclimatise flocculant seed over 8–16 weeks at progressively higher OLR until granules form (source: sswm.info UASB factsheet). The four upsets a plant team should expect to see are:
Upset 1 — VFA accumulation and pH drop. Cause is an OLR shock, temperature drop, or an inhibitor in the feed (e.g. ammonia from a protein spike, or a solvent slug). The fix is to cut load, restore alkalinity by dosing bicarbonate, and check for inhibitors in the upstream process.
Upset 2 — Granule washout. Symptom is rising effluent TSS and falling COD removal. Causes are excessive upflow velocity, distributor channelling, or a damaged separator. Investigate hydraulics first, then inspect the three-phase separator.
Upset 3 — Sludge build-up in domestic-style installations. The 2010 Aiyuk et al. study showed that feeding raw domestic sewage (522 mg/L CODt) without screening removed 80% of COD but generated ~70% of the influent COD as suspended solids, forcing sludge discharge roughly every 100 days; each discharge disturbed the methanogens and triggered a performance dip (source: doi.org/10.7763/ijesd.2010.v1.76). Pre-screening with a DAF pre-treatment upstream of a UASB is the practical fix whenever influent SS is high.
Upset 4 — Corrosion and odour. H₂S in the biogas attacks internals and piping. Install an H₂S scrubber, use stainless or FRP for the gas train, and route the gas away from any ignition source.
Frequently Asked Questions
What is a UASB reactor and how does it work?
A UASB reactor is a single-vessel anaerobic system that treats wastewater by pumping it upward through a dense bed of self-immobilised granular sludge, where hydrolysis, acidogenesis, acetogenesis and methanogenesis convert 80–95% of influent COD into biogas. An internal three-phase separator retains the granules, captures the biogas, and discharges clarified effluent.
What OLR and HRT should a UASB be designed for?
Industrial UASB reactors are typically designed for an OLR of 4–15 kg COD/m³/day at an HRT of 6–12 hours; municipal and domestic systems run at 10–14 hours HRT to absorb lower temperatures and weaker feed. The trade-off is volume versus robustness: longer HRT costs capex but improves stability (source: blog.anaerobic-digestion.com UASB design reference).
What is granular sludge and why does it matter?
Granular sludge is a 1–3 mm diameter microbial aggregate with a layered structure: fermentative bacteria on the outside, methanogens on the inside. Its specific methanogenic activity routinely exceeds 1 g COD/g VSS/day, several times higher than flocculant sludge, which is what allows the reactor to be so compact.
Does a UASB need post-treatment?
Yes. A UASB does not remove nitrogen, phosphorus, pathogens, or recalcitrant COD; an MBR, aerated lagoon, constructed wetland, or moving-bed biofilm reactor is mandatory to meet a discharge consent, and a sludge dewatering press for wasted UASB biomass is normally required downstream as well (source: sswm.info UASB factsheet).
Can a UASB reactor work in cold climates?
Below roughly 20 °C, methanogenic activity drops sharply and an unheated UASB struggles to hit effluent targets without a hybrid UASB-filter or covered-insulation design (source: IWA Publishing, doi.org/10.2166/wst.2004.0865). Cold-climate installations generally combine a UASB with a downstream anaerobic or aerobic filter and biogas-side heat recovery.
How much sludge does a UASB produce compared with activated sludge?
A UASB produces roughly 0.05–0.10 kg VSS per kg of COD removed, against ~0.40 kg VSS/kg COD for a conventional activated sludge plant — a 4–8× reduction that directly cuts sludge handling and disposal cost (source: blog.anaerobic-digestion.com UASB design reference).